High-Purity Fruit Powders & Synergistic Botanical Actives
Manufactured under stringent ISO9001 and cGMP-aligned systems in Xi'an, China. Every fruit extract powder and synergistic active delivers validated solubility, high active retention, and total batch reproducibility.
Natural high-potency glycosides purified to 98% via recrystallization, providing clean sweetness without glycemic impact or bitter aftertaste.
Send an Inquiry
Native Vitamin C naturally bound to bioflavonoids for superior biological half-life. Low-temperature dried for maximum active stability.
Send an Inquiry
Rich in bioactive anthocyanins and complex dietary fibers. Ideal for RTD functional beverages, clean-label confectioneries, and bakery formulations.
Send an Inquiry
Whole-berry matrix concentrating rare palmitoleic acid (Omega-7), superoxide dismutase (SOD), and vitamin E for premium cellular vitality formulas.
Send an Inquiry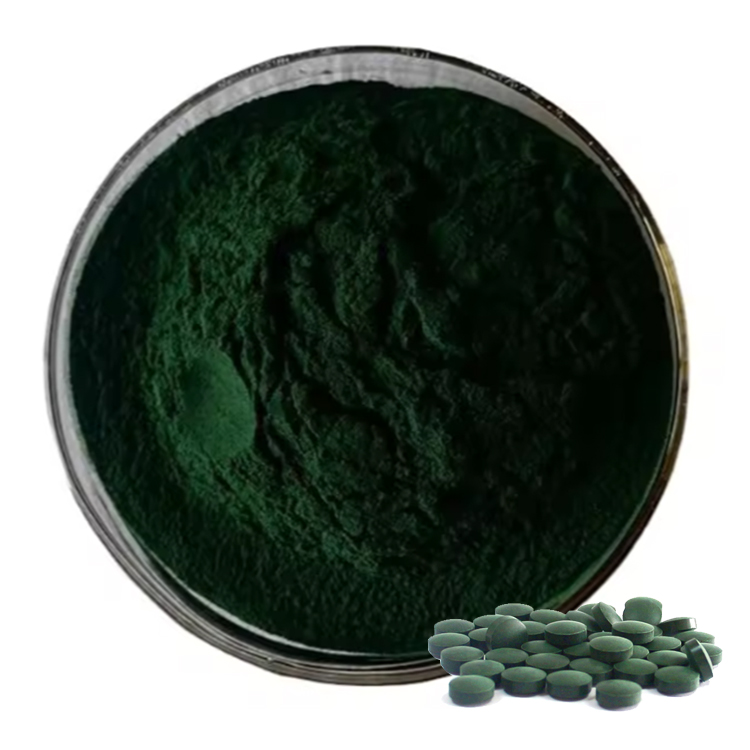
Cultivated under closed-circuit raceway systems. Certified food grade, rich in phycocyanin, iron, and complete vegetable protein profile.
Send an Inquiry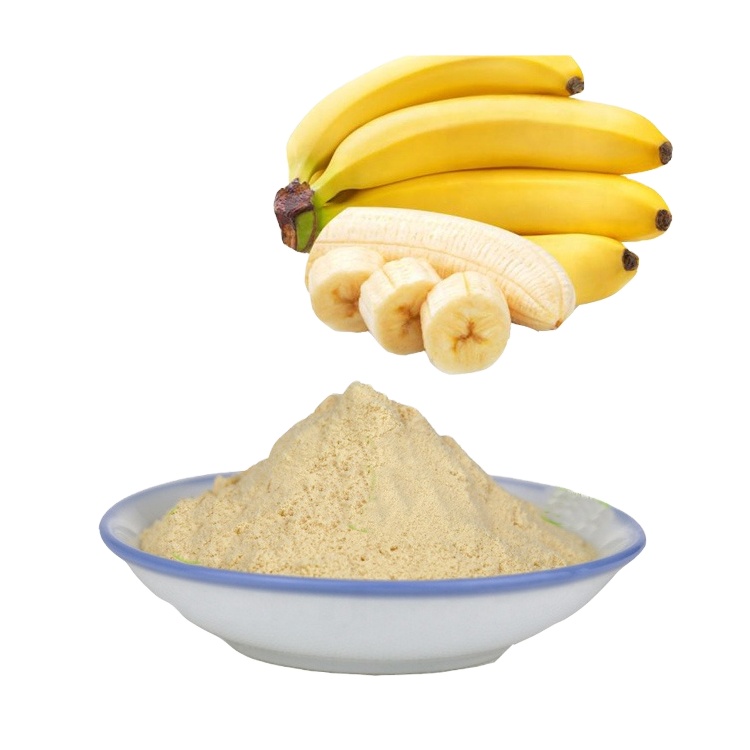
100% natural organic Musa acuminata, vacuum sublimated to preserve thermolabile vitamins, enzymatic integrity, and authentic flavor aromatics.
Send an Inquiry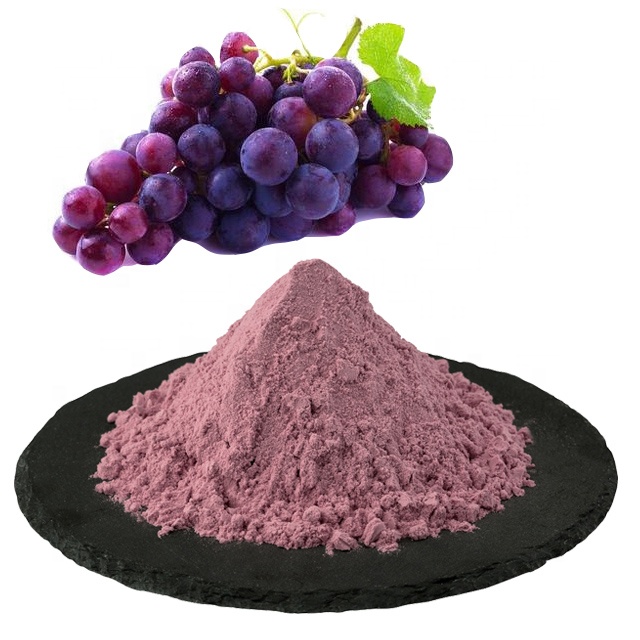
Concentrated Citrus paradisi juice powder high in naringin, hesperidin, and natural pectin, offering instant cold-water dispersion without precipitation.
Send an Inquiry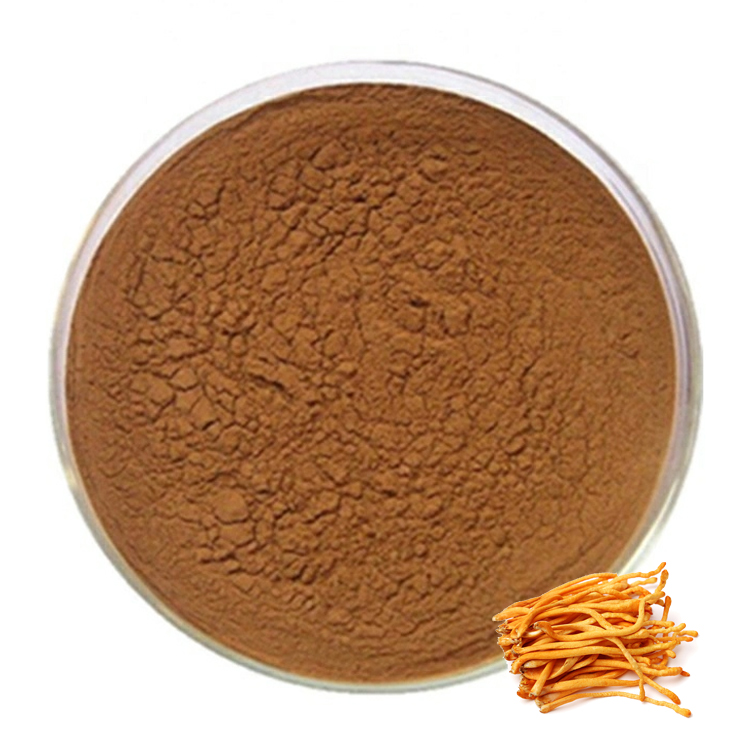
Deep enzymatic extraction yielding 30%–50% polysaccharides and HPLC-verified cordycepin, providing robust functional synergy with fruit powders.
Send an InquiryOvercoming Degradation in Fruit Powder Manufacturing: From Polyphenol Stability to Thermodynamic Drying
A technical guide for industrial formulation directors, master supplement formulators, and supply chain procurement officers.
1. The Chemistry of Thermal Degradation and Enzymatic Browning
In the processing of whole fruits into commercially viable extract powders, preserving delicate phytocompounds is a complex thermodynamic challenge. Natural bioactive markers such as anthocyanins (cyanidin-3-glucoside), polyphenols (resveratrol, naringin), and native ascorbic acid are vulnerable to oxidation, mechanical shearing, and heat-induced thermal degradation. Exposure of crude fruit puree to heat exceeding 60°C activates polyphenol oxidase (PPO) and peroxidase (POD), accelerating phenolic compound cleavage into melanoid pigments, degrading active yield and darkening powder color.
At Torzi Biotech, our extraction methodology circumvents this degradation pathway through continuous closed-circuit extraction paired with ultrafiltration and flash vacuum concentration. Operating under negative pressure (vacuum state: -0.08 to -0.095 MPa), we suppress boiling points below 45°C. This allows our fruit powders—such as natural Acerola Cherry (standardized up to 25% native Vitamin C) and Freeze-Dried Grapefruit juice powder—to preserve native molecular integrity, ensuring maximum biological activity for demanding nutraceutical applications.
2. Resolving Moisture Adsorption, Glass Transition State (Tg), and Caking
High monosaccharide and disaccharide concentrations (glucose, fructose, sucrose) with low molecular weight give dried fruit purees low Glass Transition Temperatures (Tg), frequently under 35°C at ambient humidity. When temperatures during transport or storage surpass this critical Tg point, the powder transitions from a stable glassy state to a rubbery state, causing particle stickiness, caking, hygroscopic liquefaction, and poor solubility.
Through proprietary encapsulation technology using food-grade carrier matrices (or 100% pure carrier-free drying via industrial cryogenic sublimation), we stabilize the surface amorphous structure. The result is a free-flowing, 80–120 mesh particle distribution that disperses easily in RTD drinks, sports powders, and tableting lines without clumping or clogging commercial high-speed feeders.
Analytical Matrix: Testing Standards for Export Purity
| Analytical Parameter | Reference Methodology | Torzi Biotech Factory Specification | Procurement Risk Mitigation |
|---|---|---|---|
| Bioactive Assay | High-Performance Liquid Chromatography (HPLC) / UV-Vis | Target compound: 98% Steviol Glycosides / 25% Native VC | Eliminates raw material adulteration; guarantees formulation efficacy |
| Heavy Metal Limits | Atomic Absorption Spectrophotometry (AAS / ICP-MS) | Pb < 0.5 ppm, As < 0.5 ppm, Cd < 0.2 ppm, Hg < 0.1 ppm | Complies with California Prop 65 & EU Regulation (EC) 1881/2006 |
| Microbiological Bio-Burden | Plate Count Agar / USP <2021> <2022> | Total Plate Count < 1,000 CFU/g, Yeast & Mold < 100 CFU/g | Pre-screened against Salmonella spp., E. coli, and S. aureus pathogens |
| Residual Solvents | Gas Chromatography Headspace (GC-HS) | Solvent-free (Water) or Meets USP <467> Class III limits | Eliminates toxic volatile hydrocarbons (Hexane, Benzene, Methanol) |
| Pesticide Screening | LC-MS/MS & GC-MS/MS Multiresidue Screen | Undetectable / Compliant with USDA NOP 500+ Compound Matrix | Guarantees organic compliance and prevents container import impounds |
Emerging Procurement Trends in Fruit Extract Powders (2025–2030)
Understanding shifting consumer demands, evolving European & North American regulatory compliance, and advancements in functional ingredient processing.
Clean-Label & Carrier-Free Transition
Global brands are phasing out maltodextrin, silicon dioxide, and modified starches in favor of 100% pure, carrier-free freeze-dried fruit concentrates. Procurement teams favor suppliers that control particle morphology physically through advanced freeze-milling rather than synthetic flow aids.
Synergistic Functional Blends
Single-source fruit extracts are increasingly formulated into high-performance stacks with adaptogens. We see rising demand for sea buckthorn berry powder blended with medicinal fungi like cordyceps or lion's mane, pairing tart cellular hydration with metabolic stamina in single-serve sachets.
Blockchain-Verified Supply Traceability
With tightening FDA FSMA and European Corporate Sustainability Due Diligence Directives (CSDDD), enterprise buyers require full farm-to-warehouse traceability. Validated batch reports must trace botanical cultivars back to regional farming origins and agricultural pesticide logs.
End-to-End Extraction Infrastructure Located in Xi'an
Shaanxi Torzi Biotech Co., Ltd. operates a vertically integrated 12,447 m² extraction, refining, and testing complex in the Qinling botanical corridor, eliminating broker markups and ensuring strict supply chain custody.
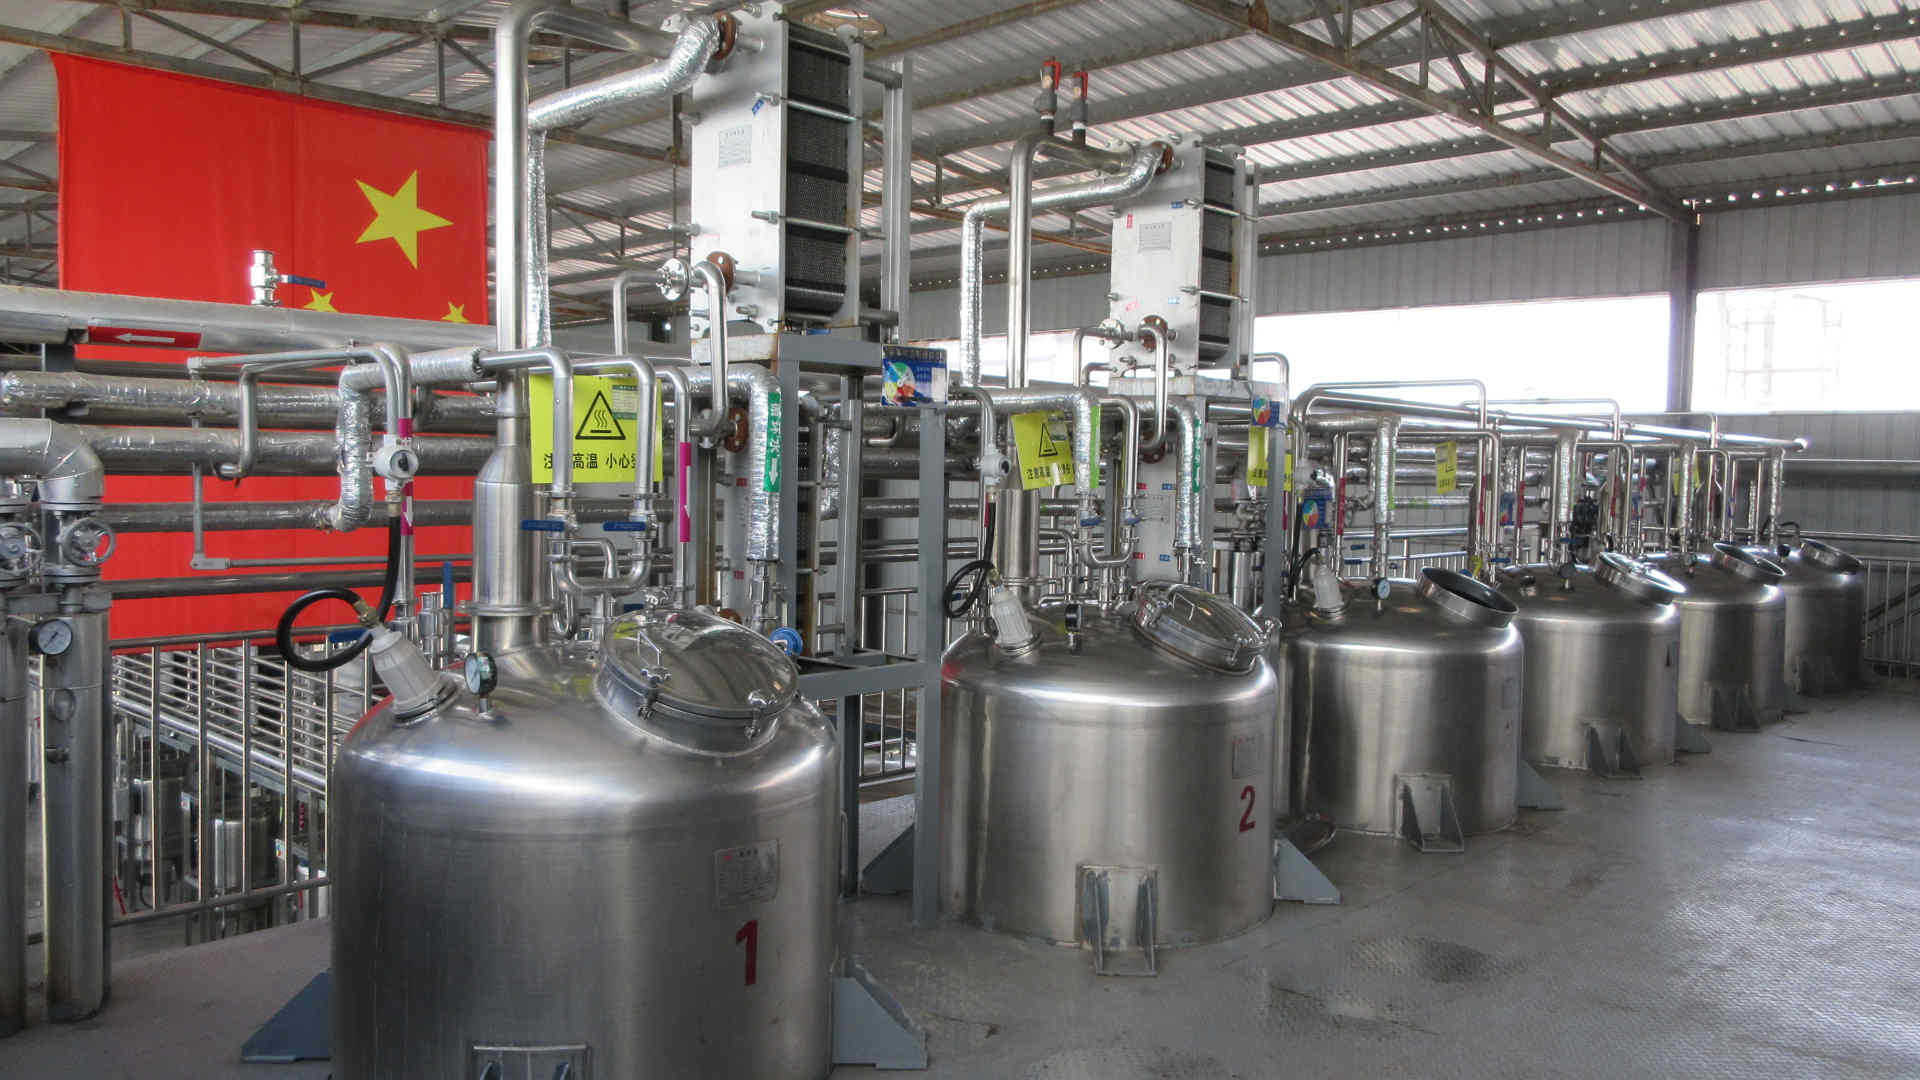
Dynamic Extraction
Sanitary stainless-steel extraction vessels with countercurrent fluid flow and multi-stage extraction cycling.
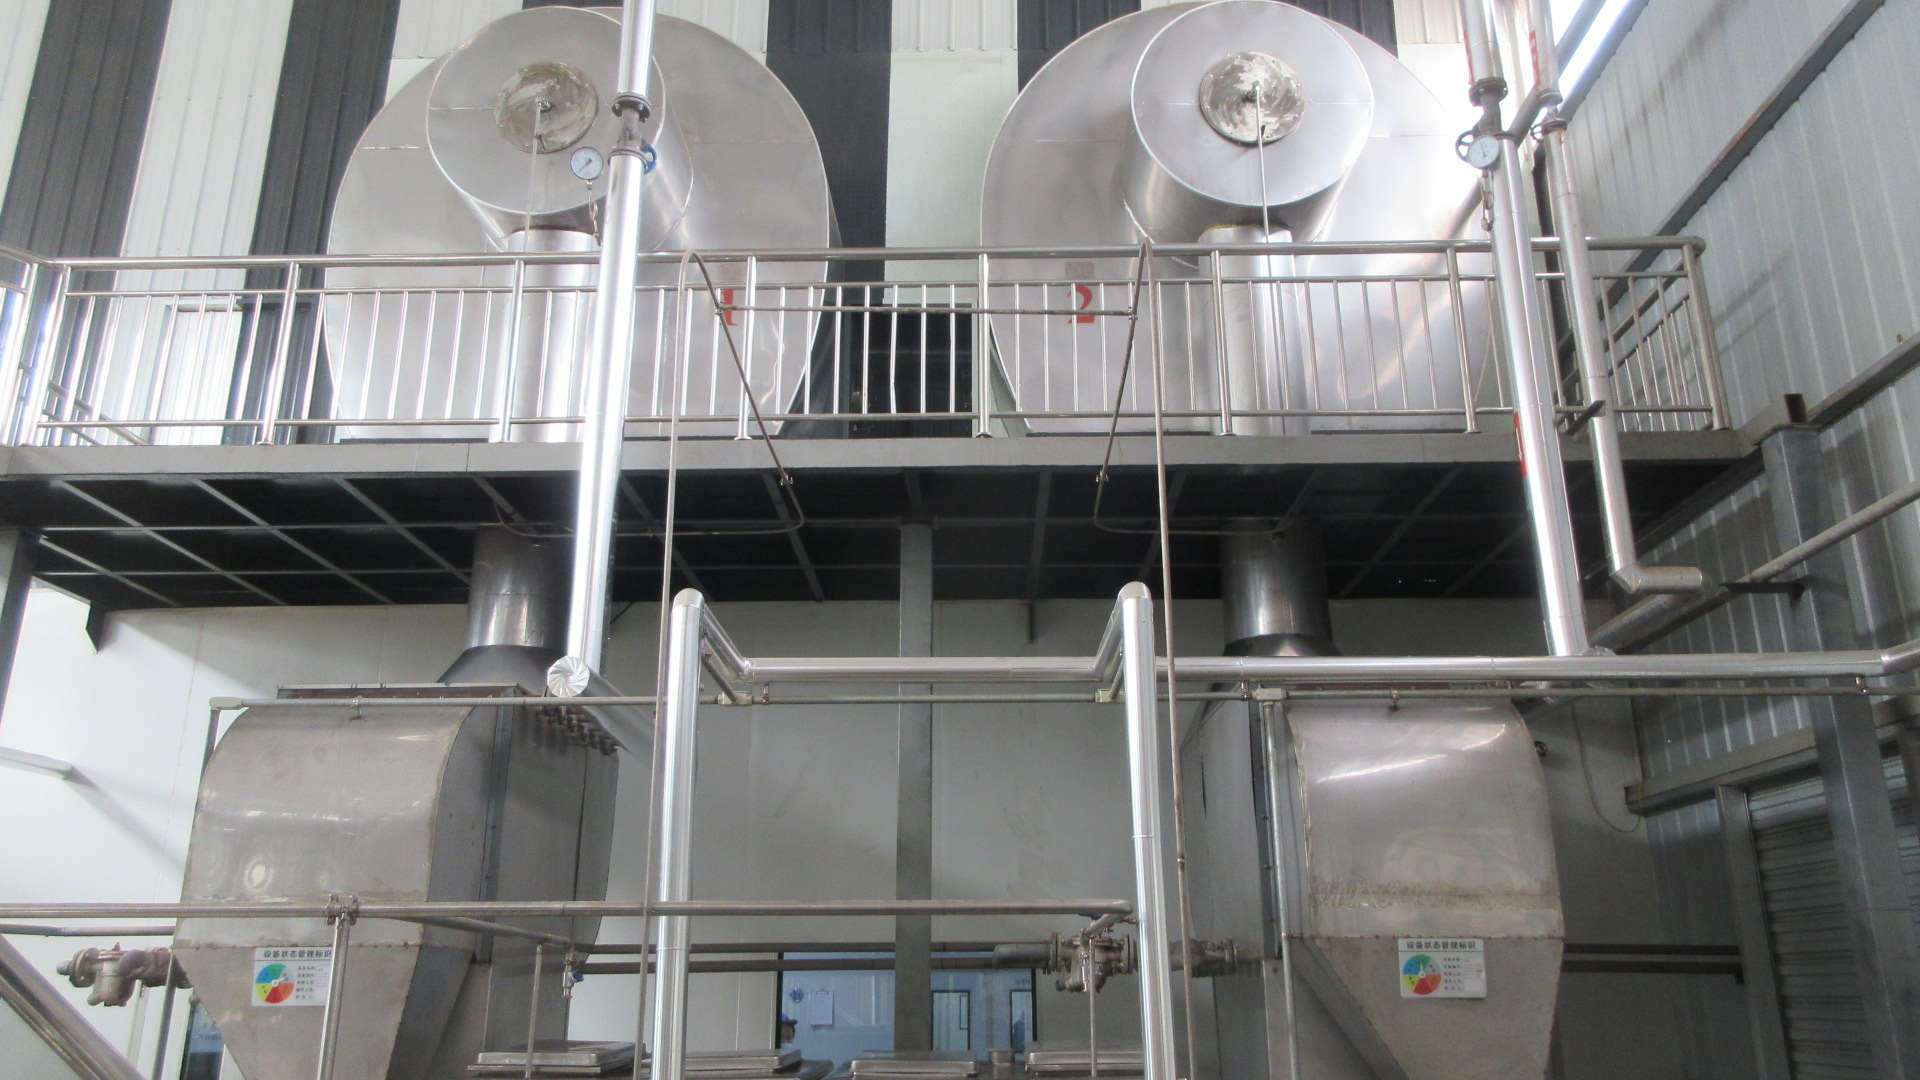
Low-Heat Drying
High-capacity centrifugal spray towers with chilled wall sweeps to prevent thermal carmelization of sugars.
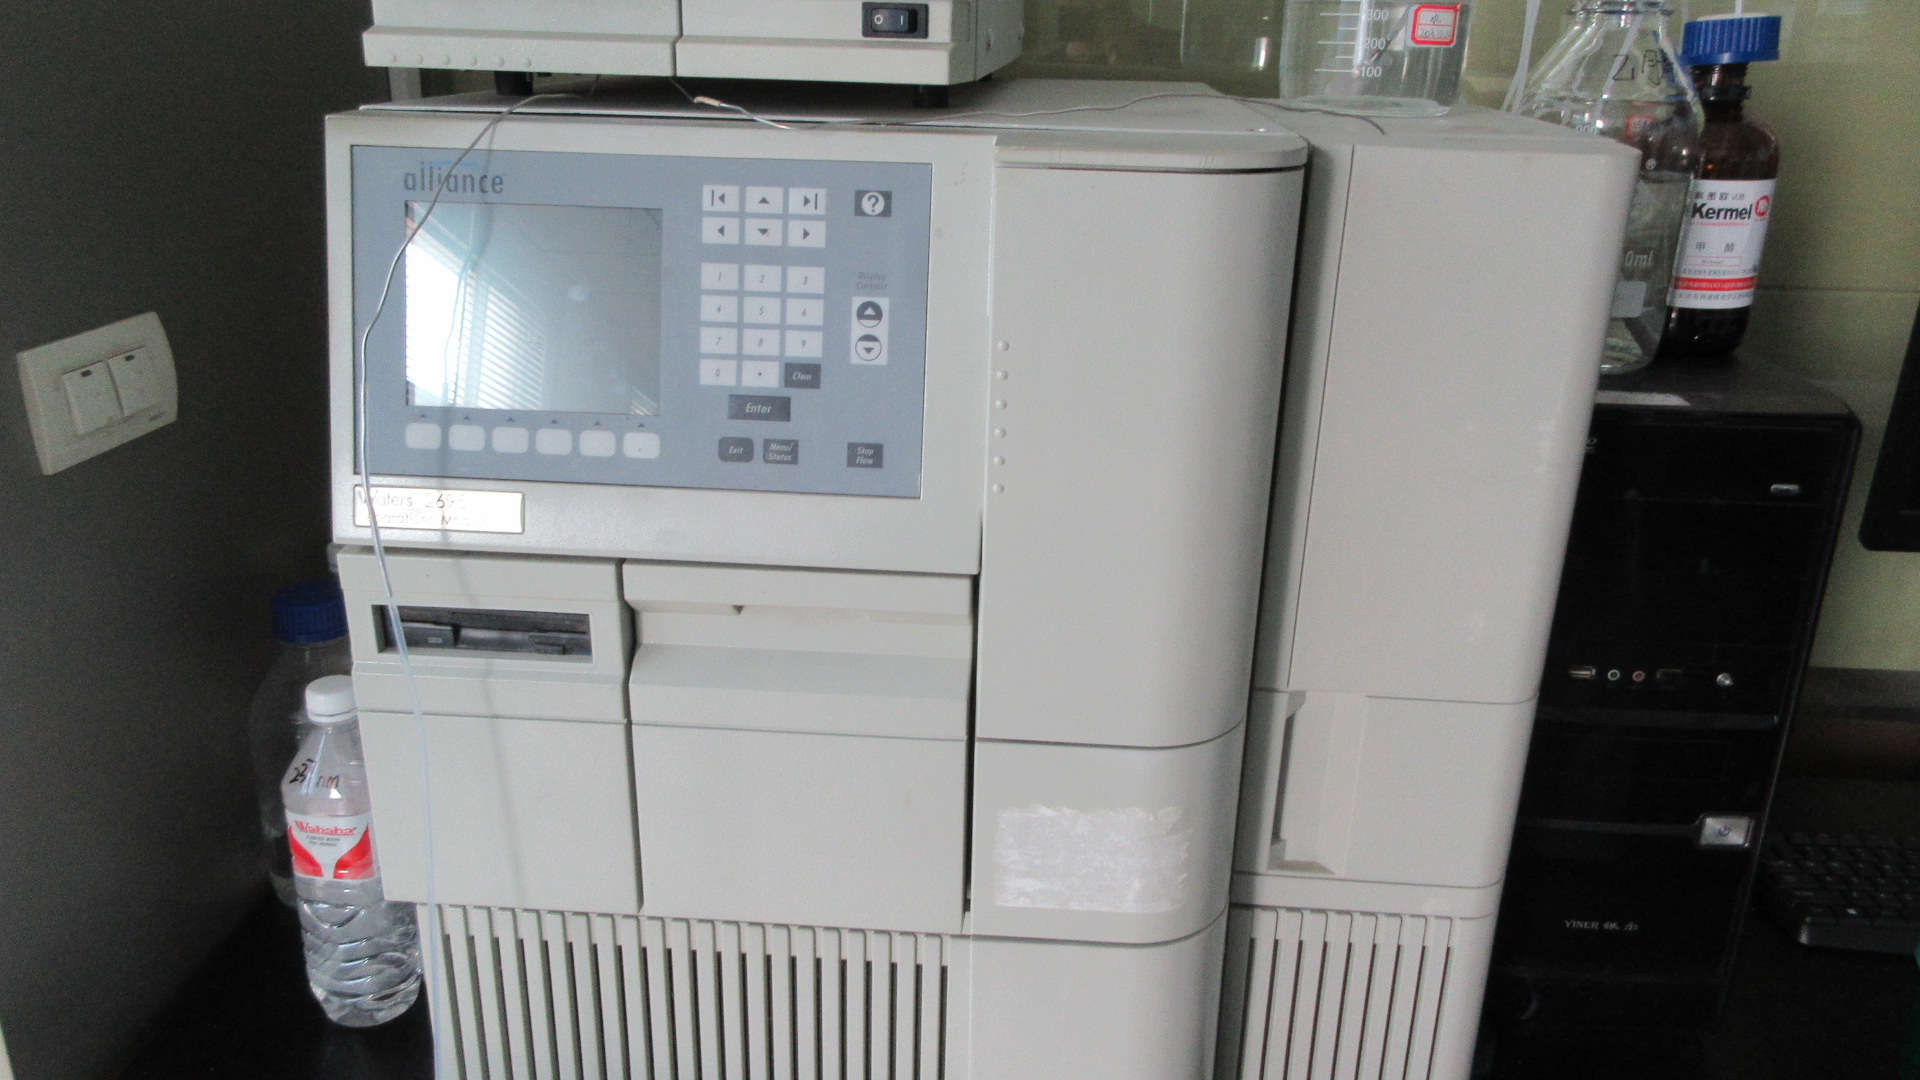
HPLC Purity Testing
In-house Shimadzu and Agilent HPLC systems for accurate assaying against USP/EP reference standards.
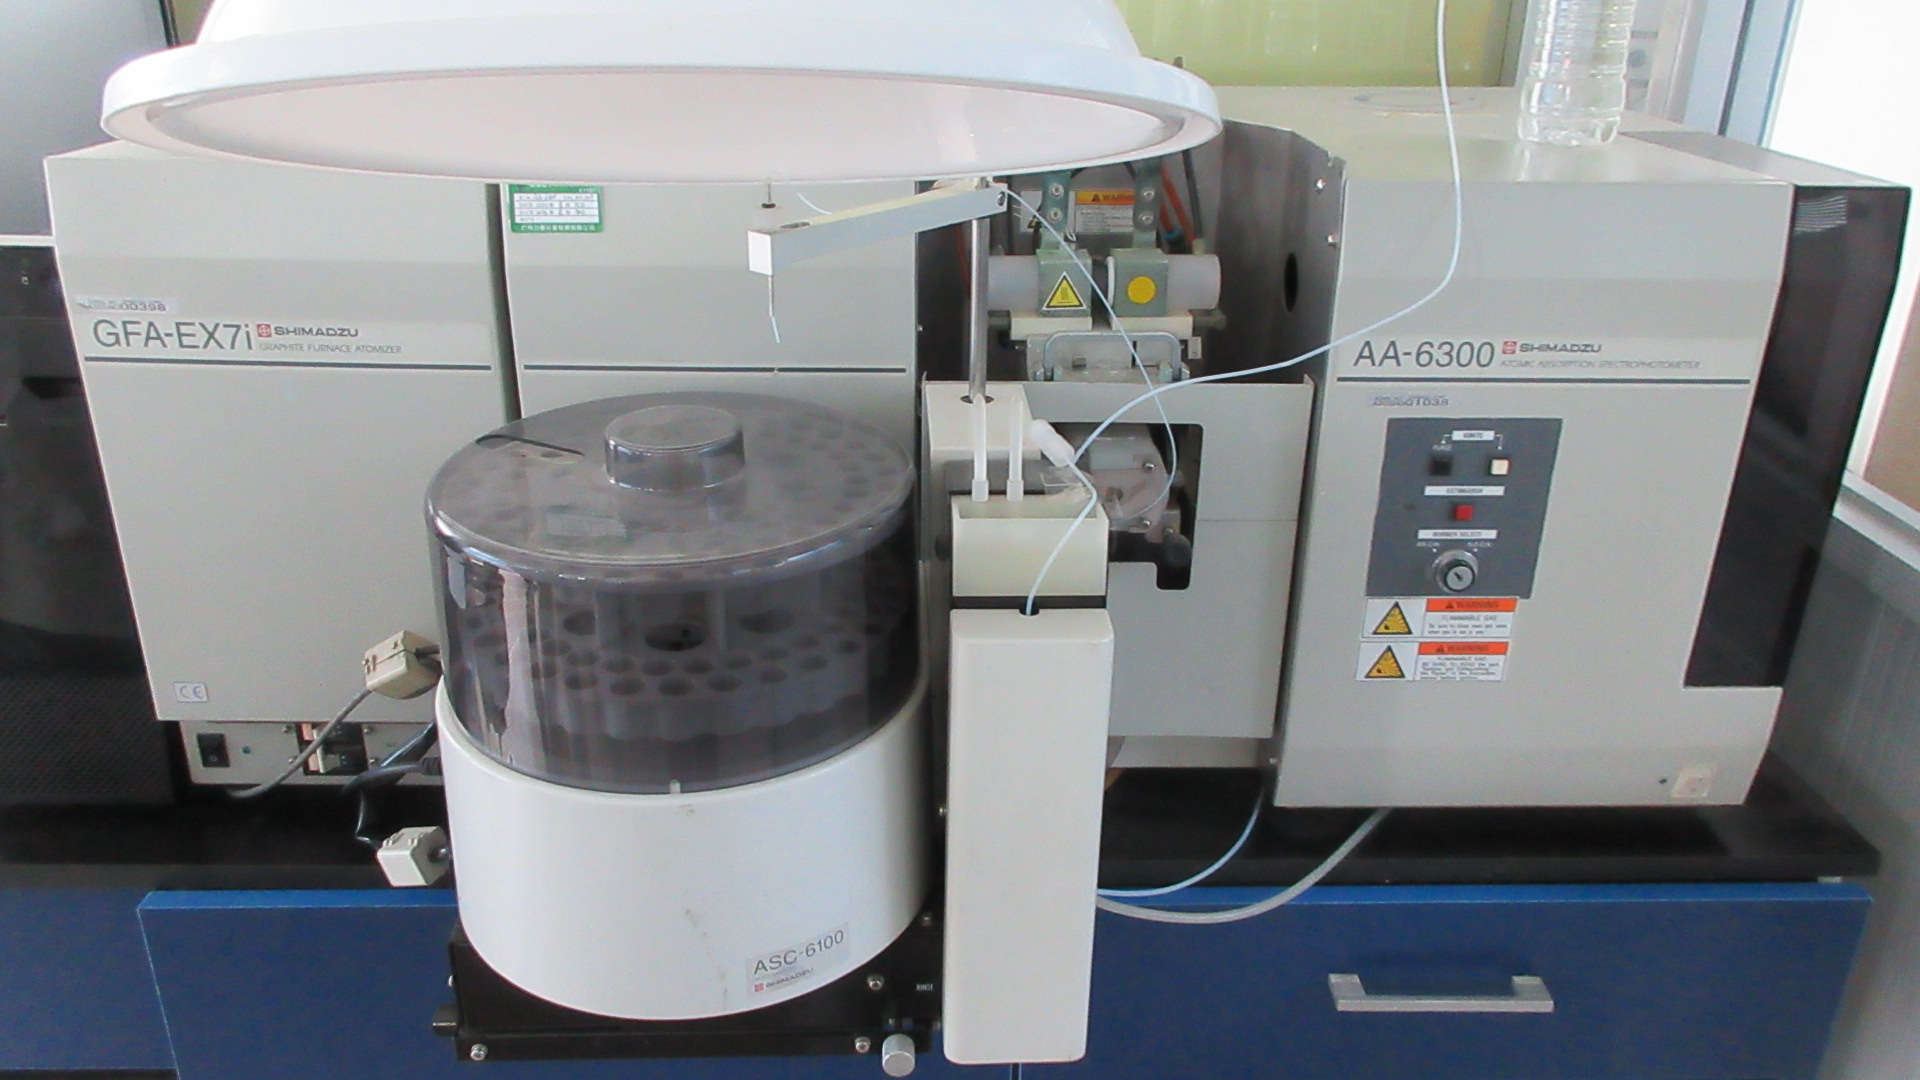
AAS Trace Profiling
Atomic Absorption and Fluorescence spectrometry verifying trace element purity across every batch.
Frequently Asked Questions for Fruit Extract Sourcing
Essential technical, logistical, and commercial answers for purchasing managers and contract manufacturers.
What is the standard MOQ across spray-dried vs. freeze-dried powders?
Standard bulk production runs require an MOQ of 25 kg packed in fiber drums with twin food-grade poly-liners. For specialty extracts (e.g., standardized Acerola VC, Stevia 98%, or custom organic ube), we support initial trial orders from 1 kg to 5 kg to facilitate pilot-line trial runs and stability testing.
How do you guarantee batch-to-batch solubility and color consistency?
Every commercial batch is standardized through uniform enzymatic maceration, automated disc stack centrifugal clarification, and microfiltration prior to low-temperature spray or vacuum freeze drying. We specify Hunter Lab color space parameters (L*, a*, b*) on each COA to verify consistent appearance across repeat deliveries.
Can you provide custom mesh sizing for high-speed tableting lines?
Yes. Our cleanroom milling and vibrating sifter arrays can produce custom granulometry from free-flowing coarse granular forms (40–60 mesh for direct compression tableting) to ultrafine powders (100–200 mesh for instantaneous cold-liquid dissolution in functional beverage applications).
What documentation accompanies international shipments?
Every delivery includes a batch-specific Certificate of Analysis (COA) containing HPLC/UV analytical data, heavy metals (AAS), microbial plate assays, and solvent tests. On request, we provide MSDS, Non-GMO declarations, Allergen Statements, Kosher & Halal certificates, and official Customs Certificates of Origin.
Partner with an SGS-Verified Chinese Extraction Pioneer
Eliminate intermediary fees, reduce batch lead times, and secure fully documented botanical ingredients backed by our dedicated analytical chemistry lab. Request your custom quotation, technical dossiers, and lab samples today.
Send an Inquiry