Standardized Bioactive & Flavonoid Ingredient Portfolio
Precision-milled botanicals, polyphenol fractions, and active phytochemical carriers manufactured under strict ISO22000 and USDA Organic protocols.
Galium Aparine (Cleavers) Botanical Extract
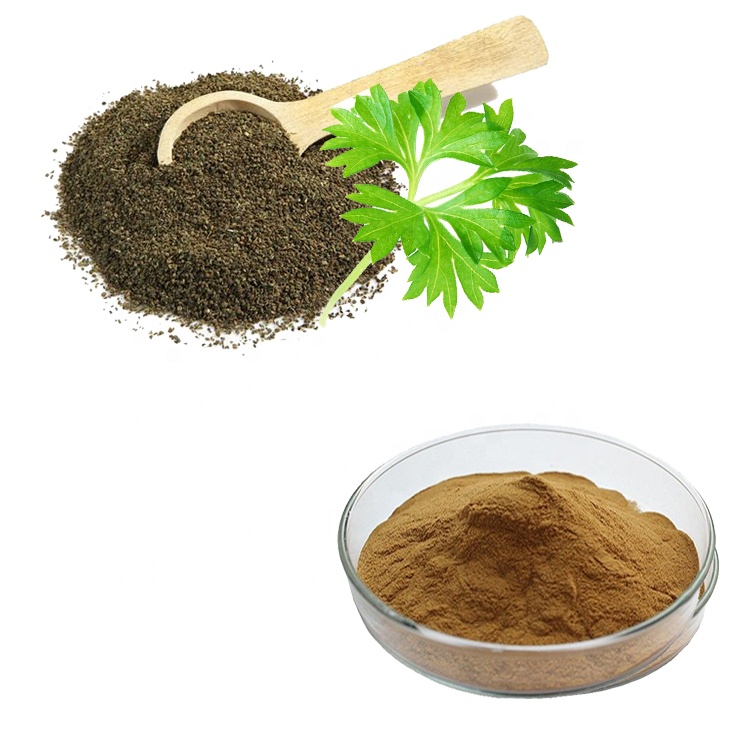
Celery Seed Extract Powder (10:1 / 20:1)
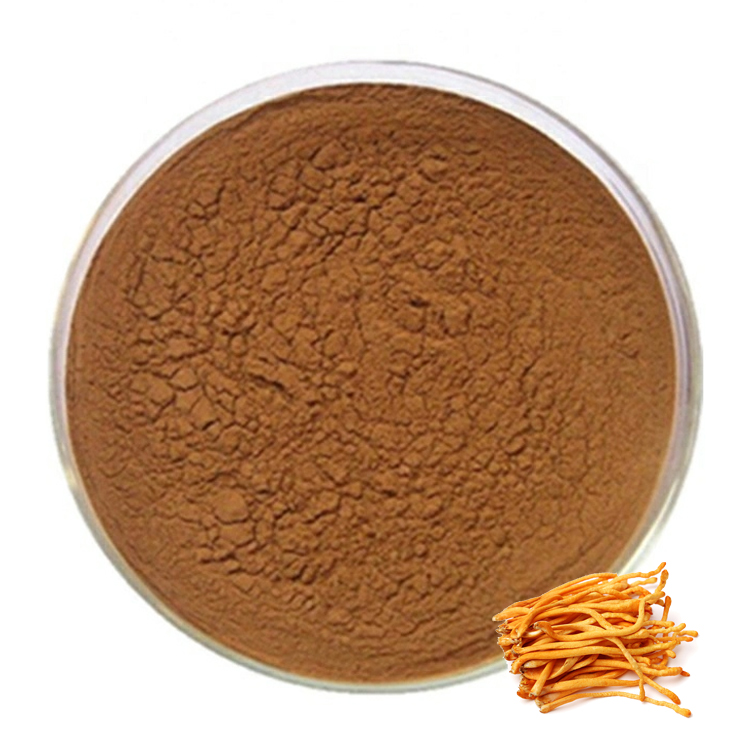
Cordyceps Sinensis / Militaris Powder
Stevia Extract Powder (98% Steviol Glycosides)
Standardized Flavonoid Fractionation & Supply Reliability in the Capital Region
The bio-pharmaceutical and specialized nutraceutical corridors flanking Washington DC—spanning the prestigious research corridors along the I-270 Technology Corridor in Montgomery County, Maryland, through the Northern Virginia health technology centers—demand raw botanical active pharmaceutical ingredients (APIs) with zero tolerance for specification drift. Bioactive polyphenolic compounds, specifically quercetin, rutin, hesperidin, kaempferol, and naringin derivatives, are increasingly utilized not only in dietary supplements but in investigational immuno-metabolic therapeutics, clinical cosmetics, and longevity medical foods. Torzi Biotech functions as a direct cGMP extraction factory, bridging high-yield Qinling botanical resources with rigorous US Pharmacopeia (USP) and European Pharmacopoeia (EP) compliance standards.
Natural flavonoid manufacturing requires delicate equilibrium between multi-stage dynamic solvent countercurrent extraction and macroporous resin adsorption chromatography. In crude plant tissues, target polyphenols exist bound within complex lignocellulosic matrices or as glycosylated conjugates. Shaanxi Torzi Biotech employs specialized low-temperature vacuum evaporative concentration and automated thin-film falling recovery towers, completely removing toxic carrier residuals while ensuring that thermosensitive flavonoid chromones remain intact. By integrating high-resolution liquid chromatography (HPLC) with diode array detection (DAD) and atomic absorption spectrometry (AAS), our testing facilities verify the exact monomer retention index, establishing clear certificates of analysis (COAs) that sail through FDA 21 CFR Part 111 audits in the Washington DC procurement matrix.
Target Applications in the Washington DC Life Sciences Belt
Engineered for high bioavailability, chemical stability, and cross-carrier synergy in clinical, contract manufacturing, and consumer wellness applications.
Clinical Trials & Pre-Formulation
Serving biomedical research institutes in Bethesda and the DC biomedical research cluster with ultra-pure monomer flavonoids (quercetin ≥98%, rutin ≥95%, apigenin). Standardized batch homogeneity allows reproducible cellular and pre-clinical research models.
Clean-Label Contract Encapsulation
Delivered to premier Mid-Atlantic OEM manufacturing lines in Virginia and Maryland. High bulk density powders designed for high-speed automated capsule filling, compressed tablets, and bilayer longevity formulas without flow additives or synthetic binders.
Functional Beverages & RTD Systems
Custom micronized and water-dispersible flavonoid preparations optimized for RTD botanical teas, nootropic tonics, and effervescent recovery drink sticks popular among the health-conscious consumer demographics in the Washington DC metropolitan sector.
Mid-Atlantic Botanical Formulation & Regulatory Trends
Strategic macro dynamics shaping ingredient procurement in Washington DC, Maryland, and Northern Virginia.
Tightening FDA cGMP Verification
Regulatory proximity to FDA headquarters in Silver Spring drives DC brands toward verified manufacturers offering complete supply chain traceability, avoiding secondary brokers.
Demand for Bioavailability Enhancement
Standard flavonoid monomers face gastrointestinal absorption limitations; regional developers focus heavily on liposomal delivery, phospholipid complexes, and MCT dispersion carriers.
Synergistic Polyphenol-Mushroom Stacks
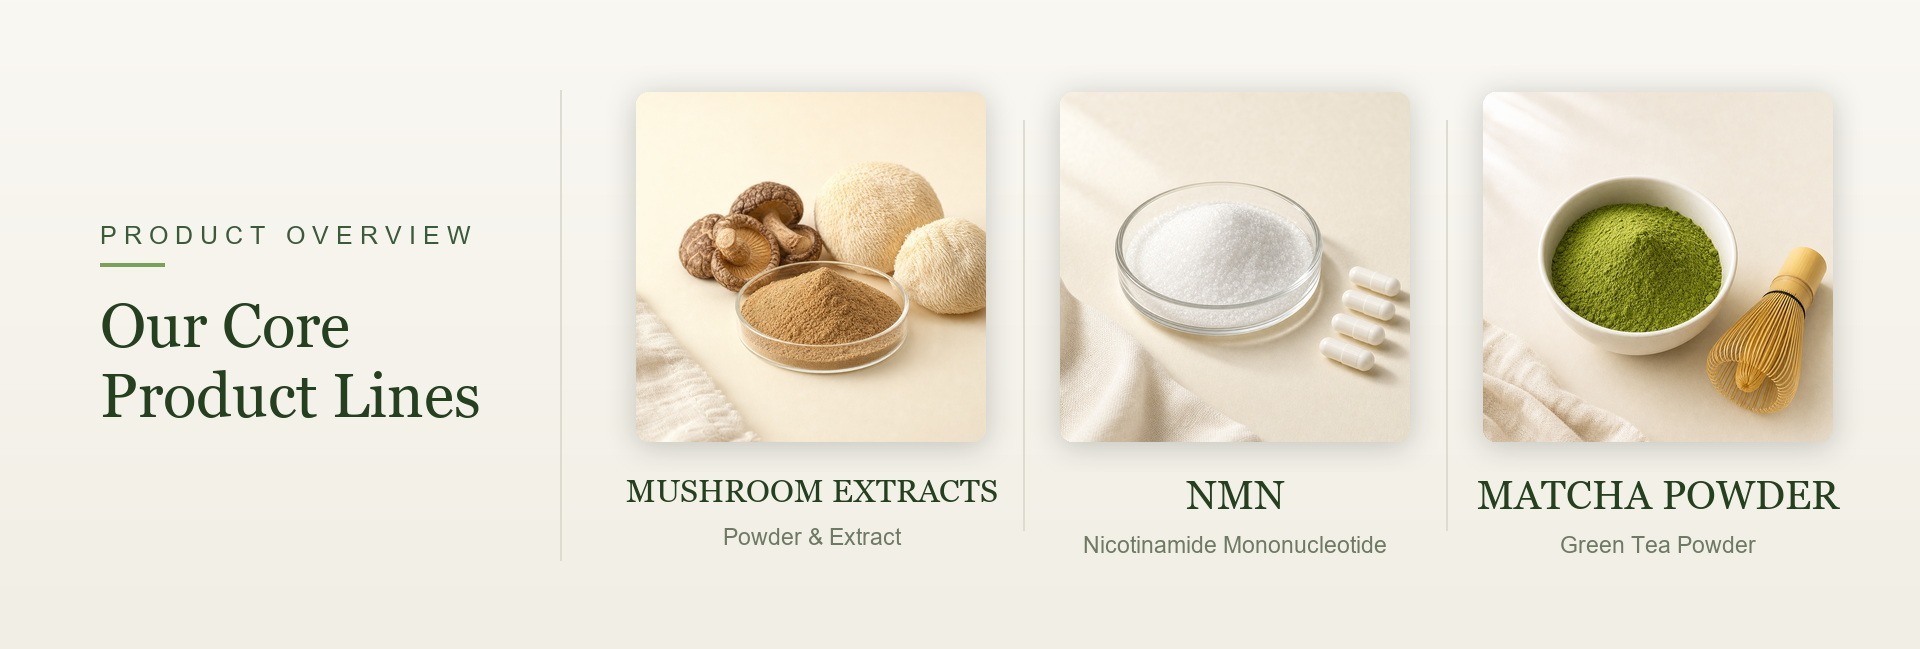
Rapid growth in clinical crossover formulations merging citrus/sophora bioflavonoids with functional mushroom beta-glucans (Lion's Mane, Cordyceps) for immune-cognitive resilience.
Strict Residual Solvent Controls
Regional procurement teams mandate Class 3 solvent protocols (USP <467>), demanding water or ethanol-only extraction routes with comprehensive GC headspace residue profiles.
Shaanxi Torzi Biotech Co., Ltd. Direct Production Advantages
Positioned at the nexus of the Qinling Mountains' immense botanical reserves, Torzi Biotech maintains complete backward integration. Unlike trading firms, we maintain end-to-end sovereignty over extraction kinetics, resin purification columns, low-temperature crystallization units, and sterile cleanrooms.
Frequently Asked Questions by Washington DC Importers
Direct answers addressing supply chain logistics, testing rigor, customs clearance, and quality assurance.
How are consignments routed into the Washington DC / Mid-Atlantic region?
Commercial full-container-load (FCL) orders typically clear via the Port of Baltimore (Seagirt Marine Terminal) with direct drayage transport into Maryland and Virginia manufacturing hubs. Expedited air parcels ship directly to Dulles International (IAD) or Baltimore/Washington International (BWI) with full customs broker coordination.
What documentation accompanies bulk botanical and flavonoid extracts?
Every commercial production batch is accompanied by an authenticated Certificate of Analysis (COA) specifying botanical origin, extraction solvent, HPLC active marker assay, heavy metals (Pb, As, Cd, Hg) via AAS, residual solvents (USP <467>), microbiological plate counts, and non-irradiation/pesticide compliance declarations.
Can you accommodate pilot runs or research institute MOQs?
Yes. While our commercial production lines handle multi-ton contract packaging in 25 kg fiber drums, our R&D pilot workshop provides smaller trial batches starting from 1 kg to 5 kg for pre-clinical evaluation, university labs, and prototype testing in DC scientific incubators.
Are custom mesh particle sizing and solubility enhancements supported?
Yes. We offer cryogenic micro-pulverization, granulating technology for high-speed tablet presses, and water-soluble micro-emulsification carriers (utilizing natural sunflower lecithin or organic coconut lipid systems) to overcome flavonoid hydrophobic properties.
Partner with a Primary Extraction Powerhouse
Consult with our technical engineering division, request comprehensive HPLC chromatographic fingerprints, or order ISO/USP standard qualification sample kits delivered directly to your Washington DC facility.