Every active botanical batch undergoes rigorous identity verification, chromatographic quantification (HPLC/GC), atomic absorption spectrometry for heavy metal clearance, and microbiological control according to EP/USP standards.
Pharma Grade
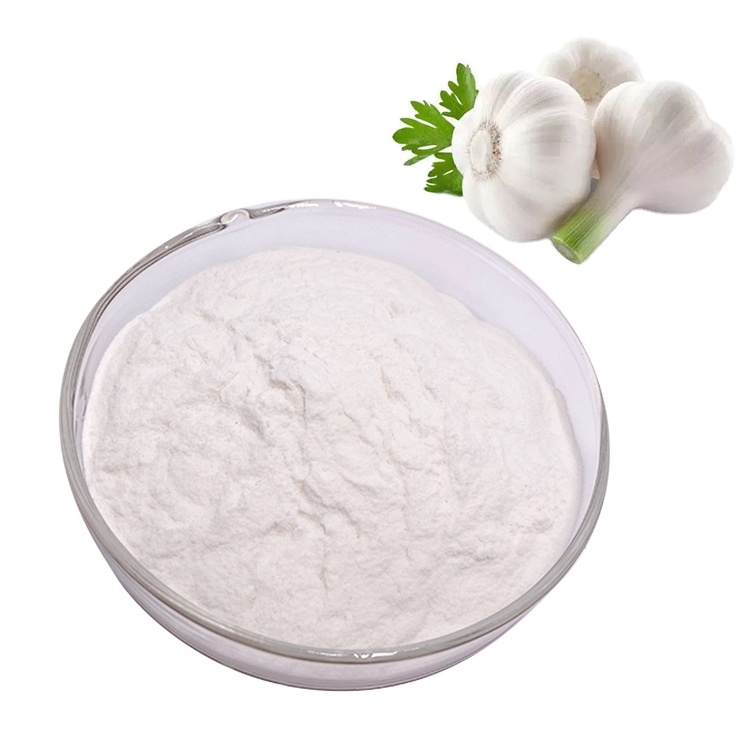
Garlic Extract Powder | 1% 5% Allicin | EP Standard
Standardized bioactive allicin matrix produced via low-temperature flash dehydration. Strict residual odor control compliant with European Pharmacopoeia (EP) specifications.
Natural non-GMO L-ascorbic acid derived straight from native Malpighia emarginata. Superior water solubility engineered for immunity sachets, softgels, and effervescent tabs.
Black Maca Root Extract Powder Capsules | Bulk OEM Supply
Concentrated 10:1 to 50:1 Lepidium meyenii root extract. Available as free-flowing bulk powder or packaged into custom HPMC/gelatin private-label two-piece capsules.
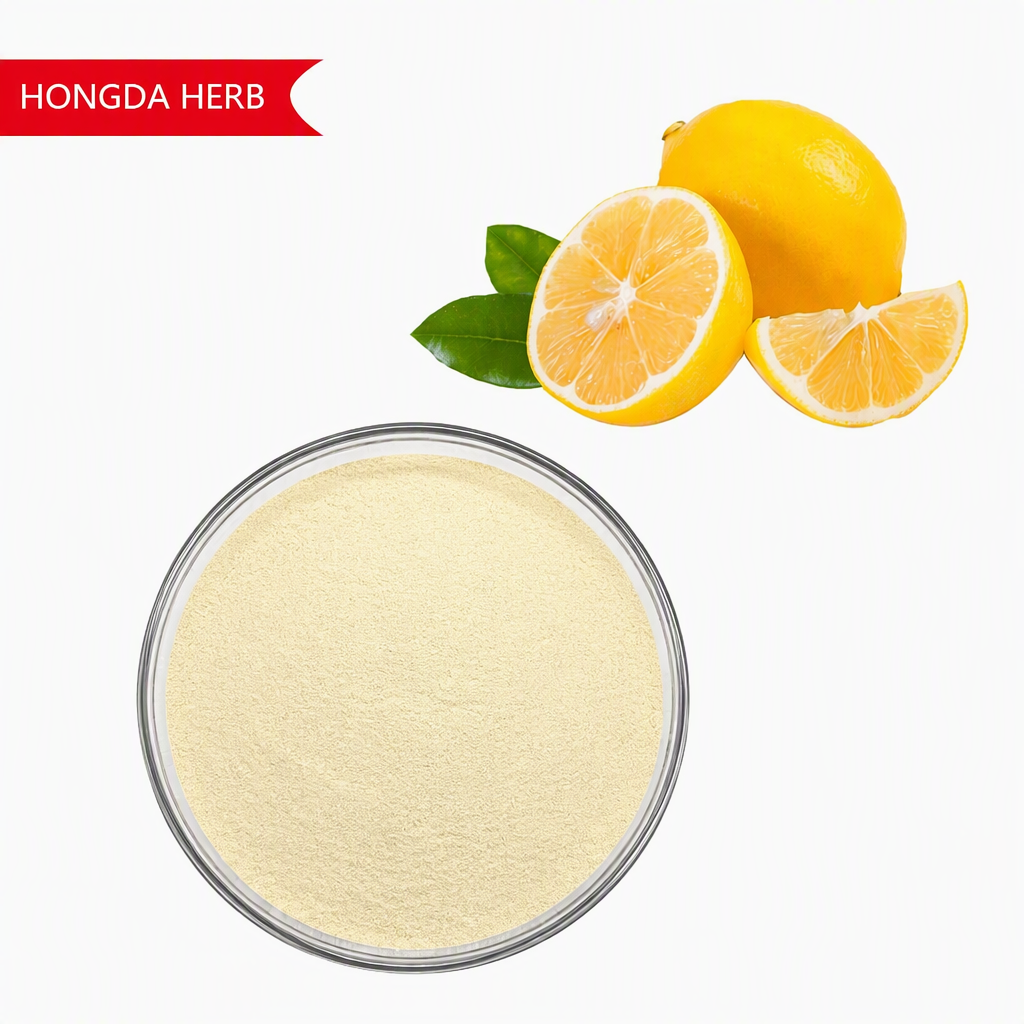
Natural Factory Supply Watersoluble Lemon Juice Powder
Spray-dried pure citrus fruit concentrate with preserved citric acid notes and bioflavonoids. Clarifies crystal clear in cold water without precipitation or sedimentation.
Low molecular weight depolymerized pectin designed for superior cellular bio-absorption. Highly calibrated esterification parameters supporting targeted detox and wellness formulas.
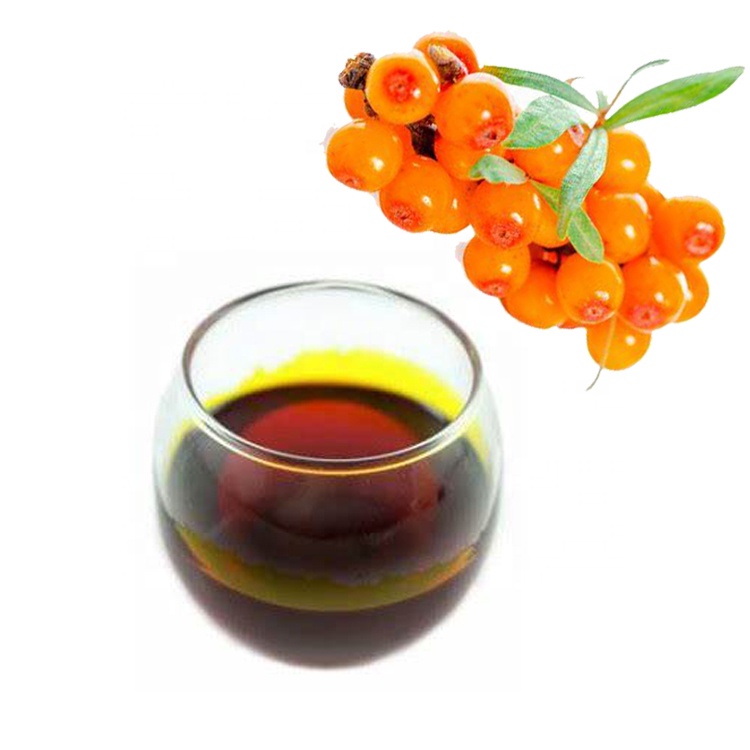
Seabuckthorn Fruit Oil Sea Buckthorn Berry Powder Supplement
Supercritical CO2 extracted lipid matrix paired with microencapsulated fruit powders boasting dense Palmitoleic Acid (Omega-7), carotenoids, and natural tocopherols.
Omega-7: ≥30% (Oil Form)Extraction: Supercritical CO2
Cosmetic Grade Gamma Polyglutamic Acid Powder PGA CAS 25513-46-6
Ultra-pure bio-polymer synthesized through Bacillus subtilis natto fermentation. Possesses 500x the moisture-locking capacity of traditional hyaluronic acid for derma formulations.
In modern phytochemistry, sourcing botanical leaf extracts demands rigorous control over biological variation, raw foliage degradation, and selective solvent fractionation. As a vertically integrated manufacturer and export partner headquartered in Xi'an, Shaanxi Torzi Biotech Co., Ltd. operates in direct geographical synergy with the Qinling Mountains—one of the planet's most bio-diverse temperate microclimates. Our comprehensive extraction infrastructure reconciles raw agricultural variability with exacting pharmaceutical requirements, delivering consistent batch-to-batch phytochemical signatures across global pharmaceutical, nutraceutical, cosmeceutical, and functional food landscapes.
Industrial foliage processing involves fragile target molecules, including polyphenols, flavones, triterpenoid saponins, and volatile organosulfur complexes. In leaf tissues, enzymatic hydrolytic cleavage begins immediately post-harvest. Without prompt stabilization, active concentrations of key markers such as catechins, allicin precursors, and natural L-ascorbic acid can drop significantly within hours. Torzi Biotech overcomes these degradative pathways via immediate microwave vacuum stabilization at dedicated plantation collection centers, followed by gentle hydrodynamic countercurrent extraction.
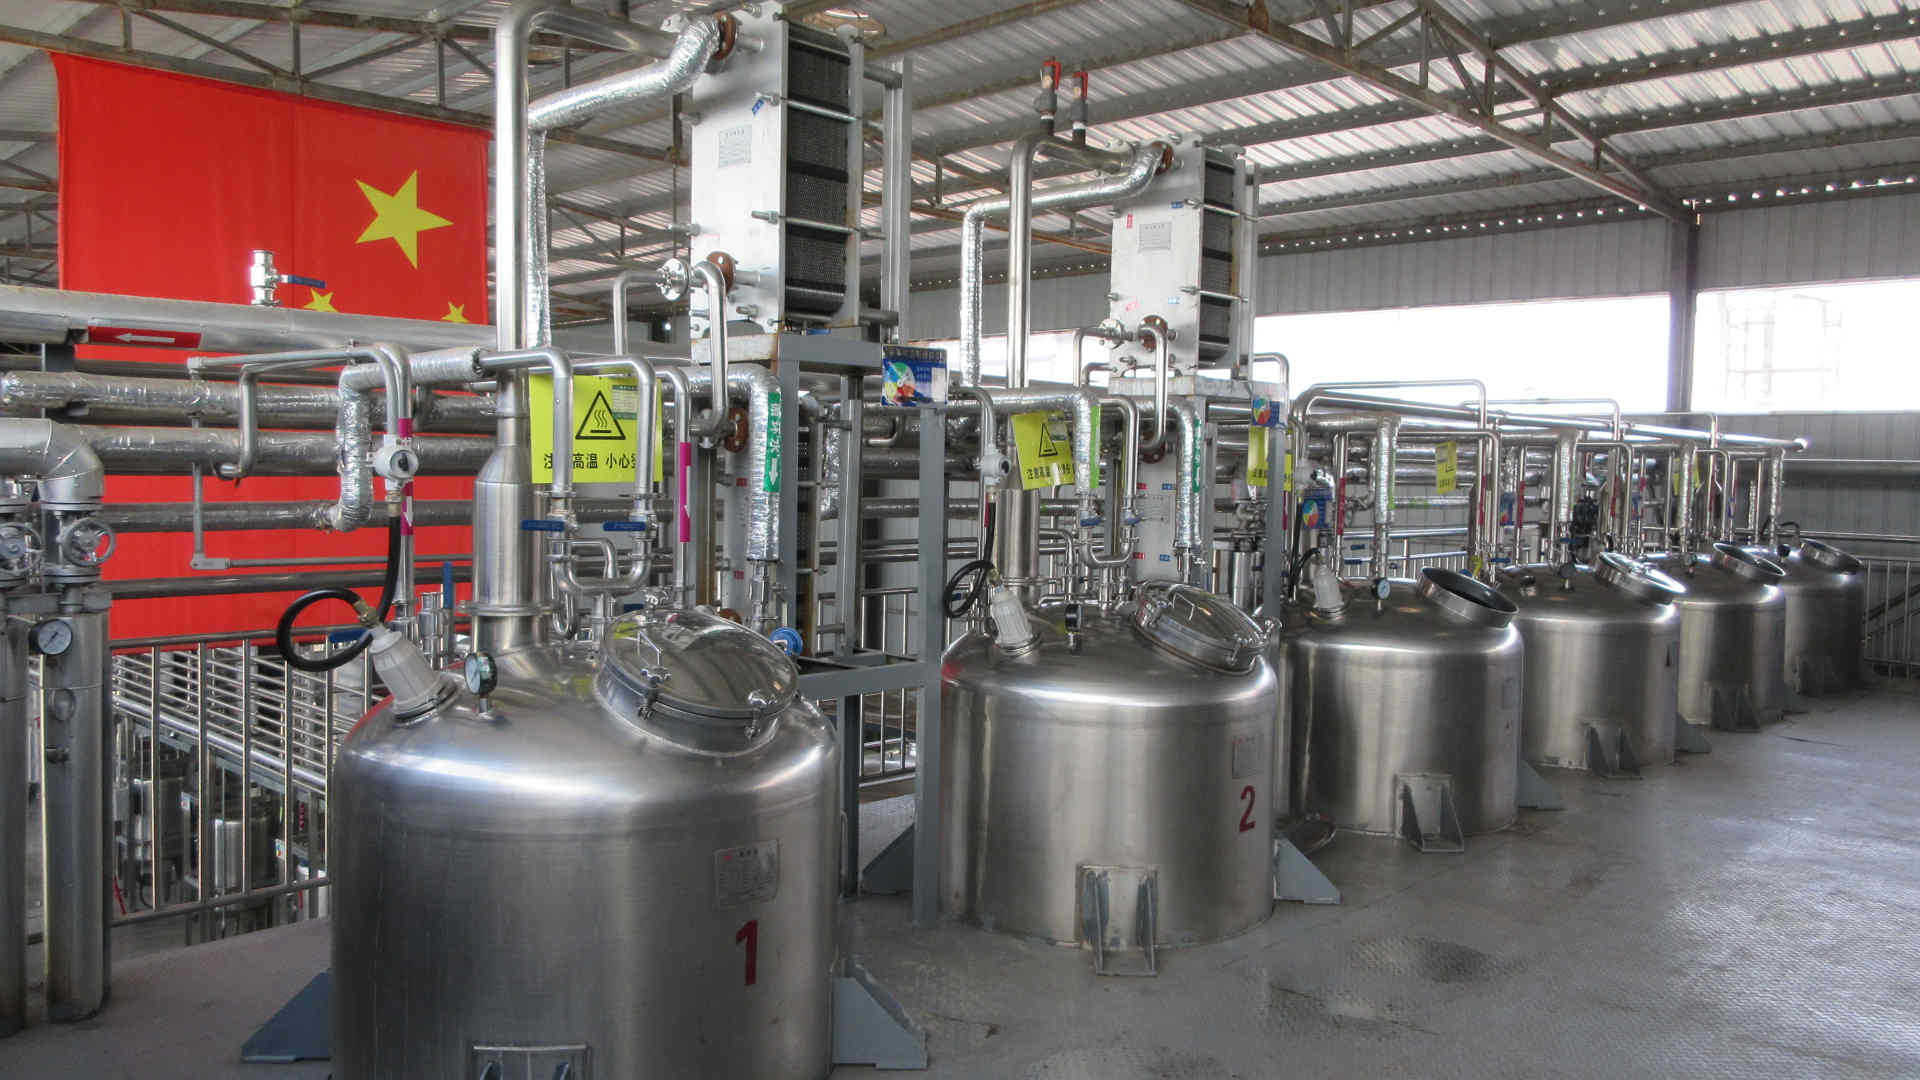
Extraction Tanks
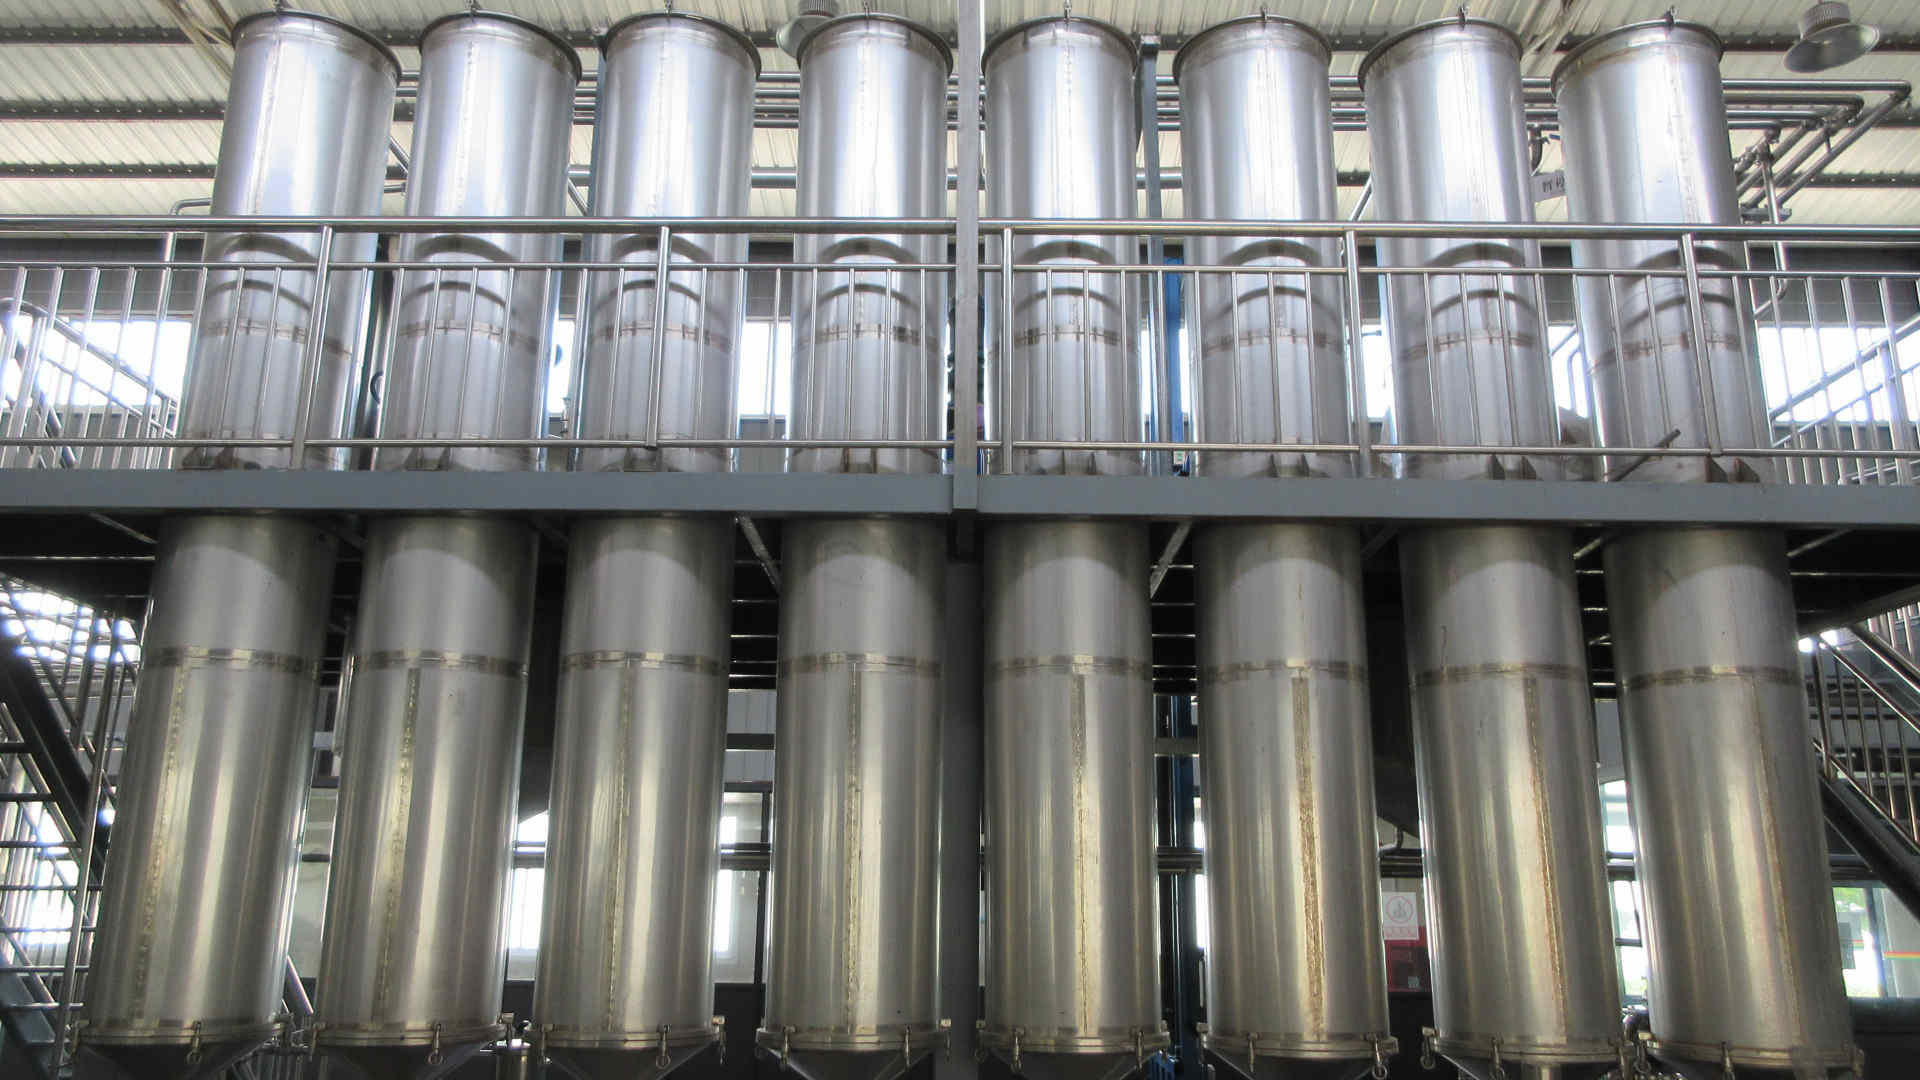
Resin Adsorption
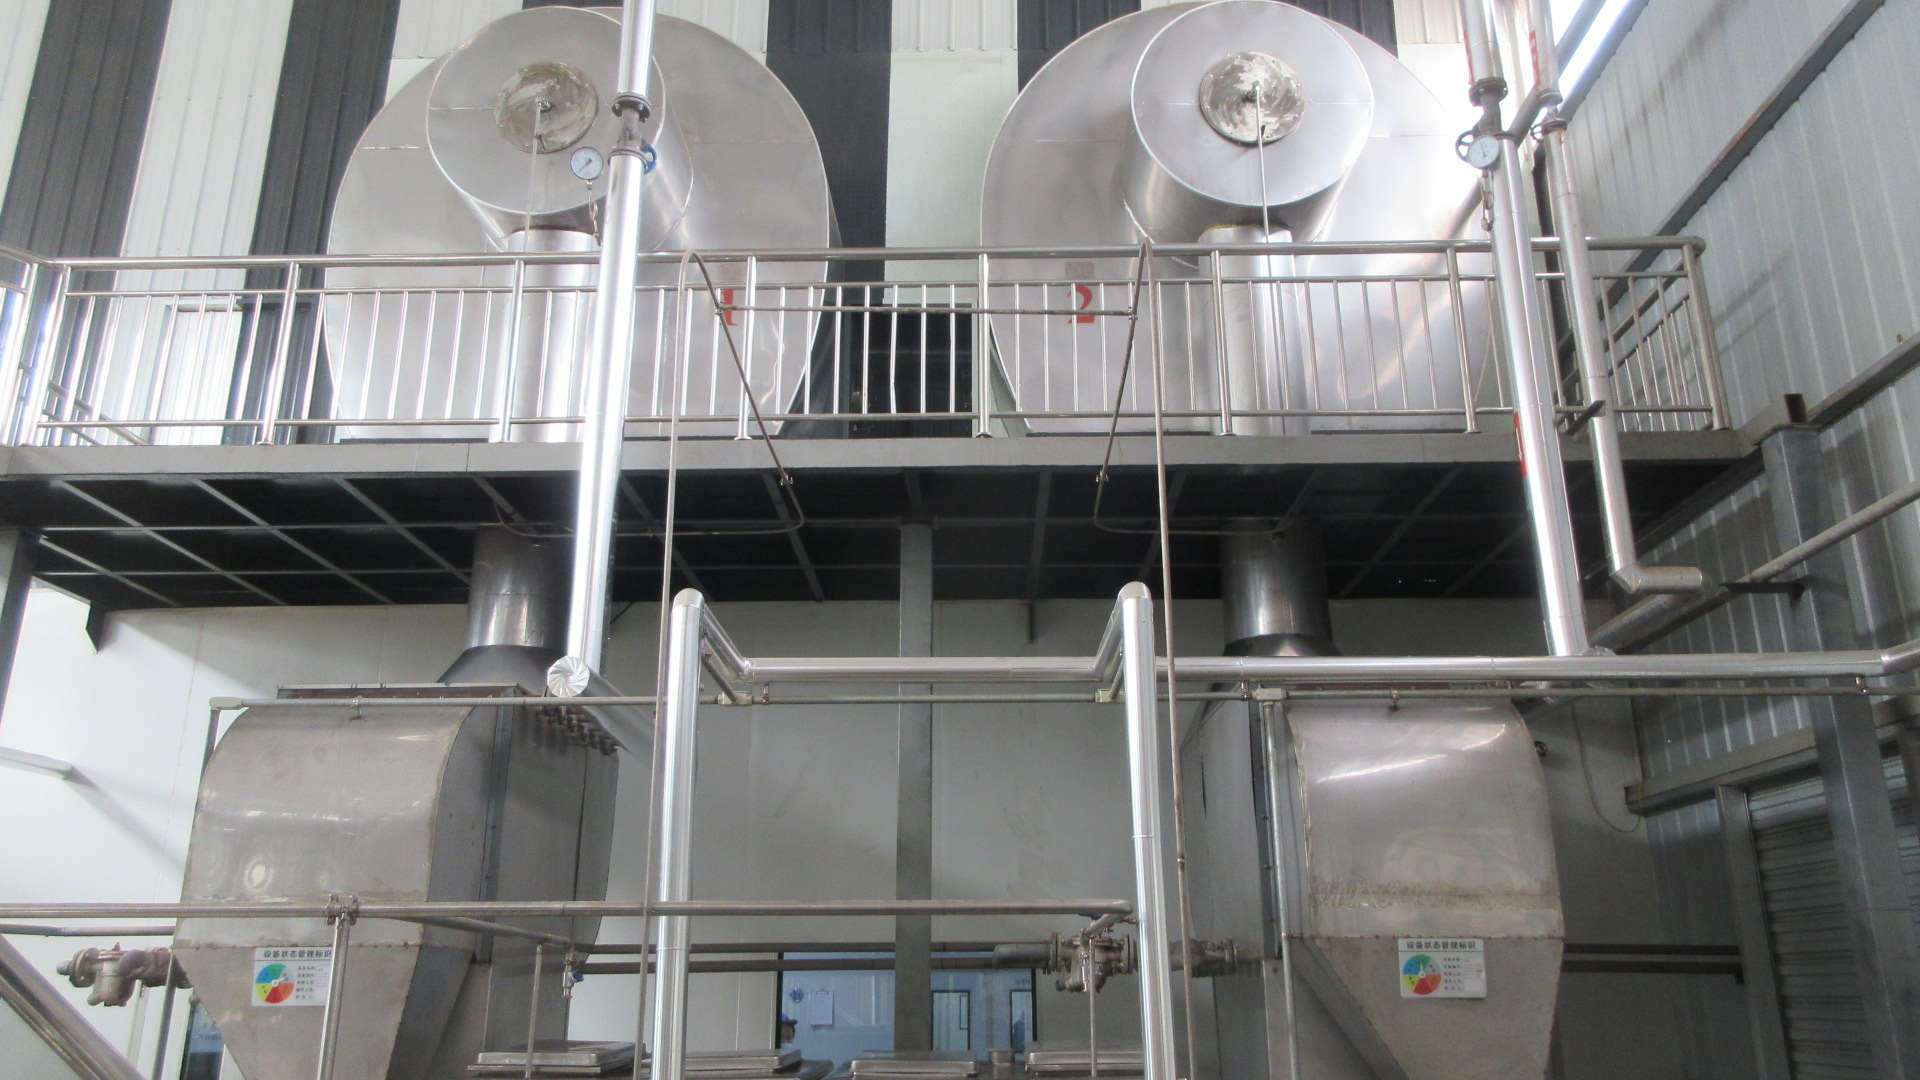
Spray Tower
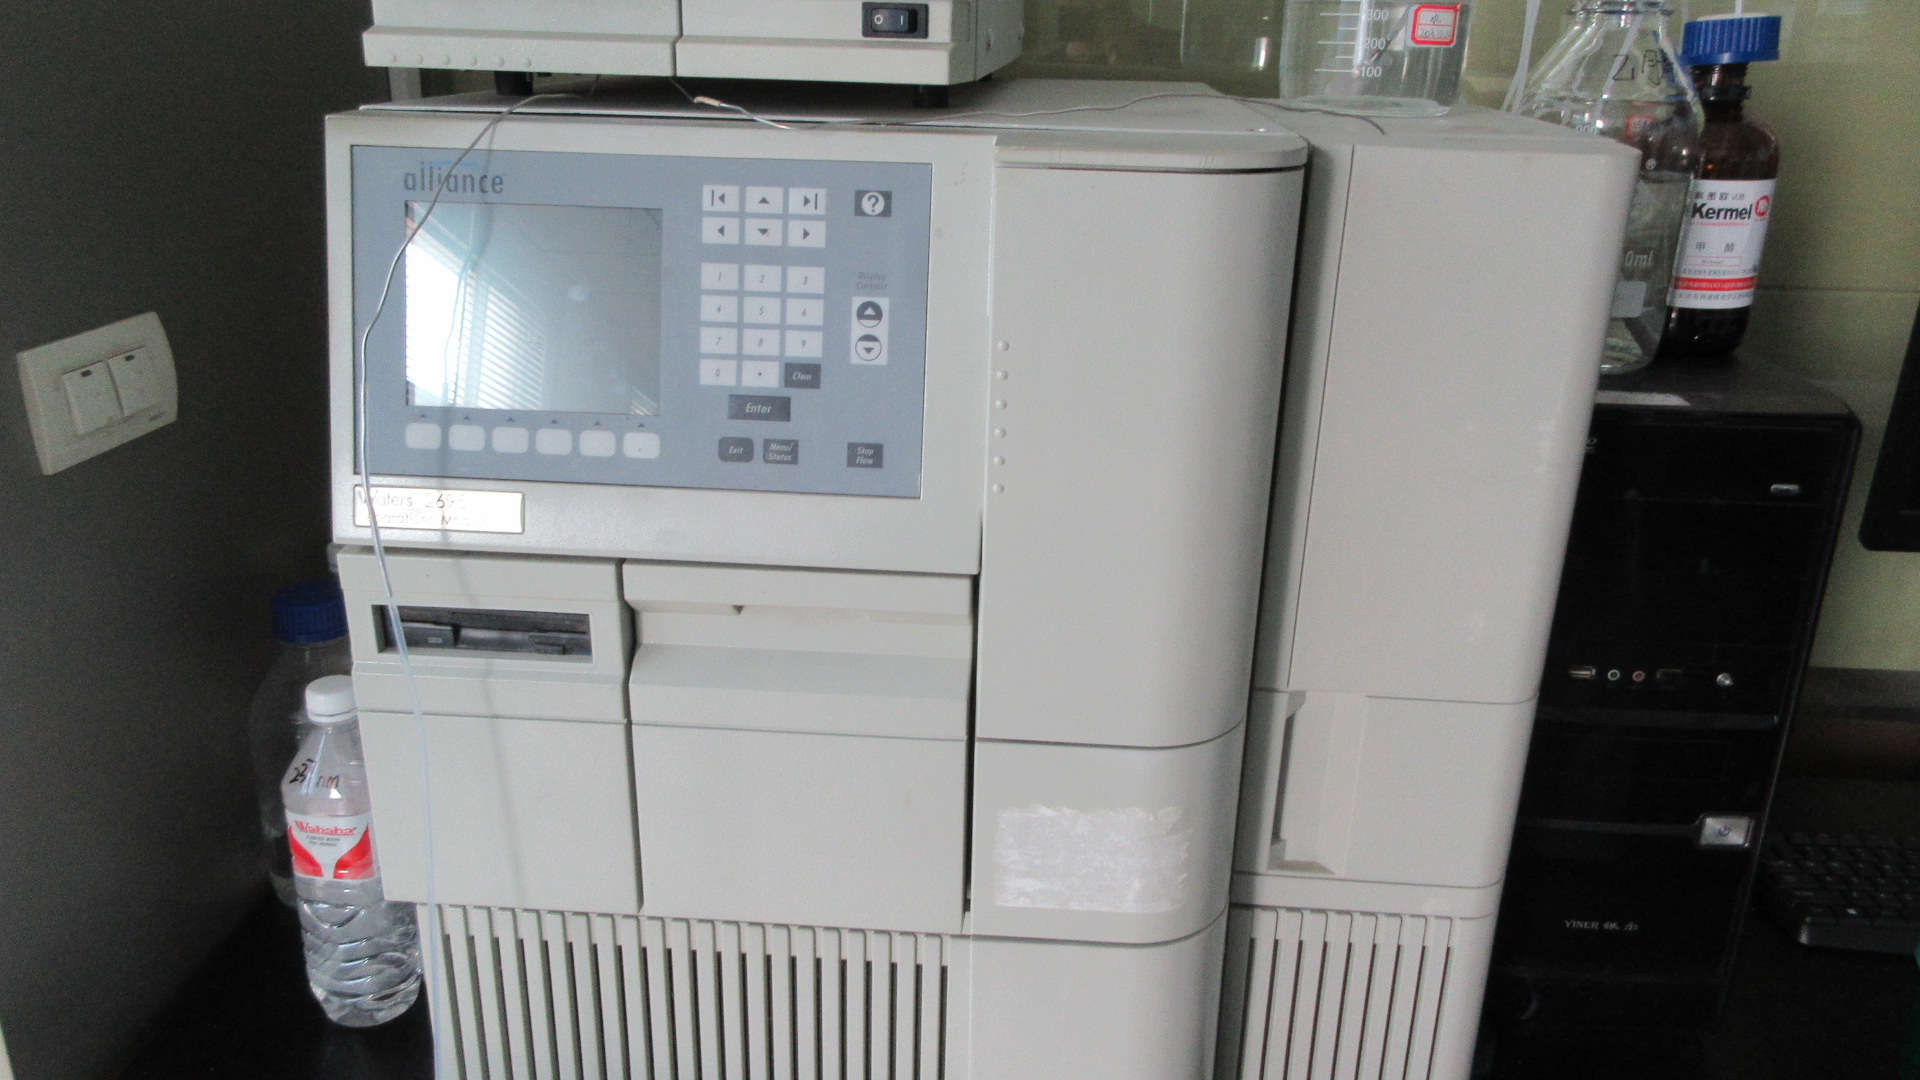
HPLC Analytical Suite
Supercritical CO2 & Low-Temp Vacuum
Preserving heat-sensitive bio-compounds through oxygen-free extraction media prevents oxidation and preserves volatile phytochemical structures.
Macroporous Resin Chromatographic Separation
Multi-stage polymeric resin beds isolate, concentrate, and refine target molecular fractions while eliminating unwanted sugars and heavy metals.
Validated In-Process QC Checkpoints
Eight sequential manufacturing controls continuously monitor density, alcohol concentration, drying curves, and mesh size distribution before lot packaging.
Strategic Market Foresight
Future Procurement Trends in the Global Leaf & Botanical Extract Industry
Procurement directors and formulation chemists face shifting regulatory landscapes, heightened transparency demands, and rapid clean-label ingredient adoption. When sourcing from foreign manufacturers, enterprise procurement teams are prioritizing standardized technical performance over raw commodity pricing.
Procurement Pillar
Legacy Sourcing Method
Next-Generation Sourcing Protocol
Impact on Brand Longevity
Phytochemical Profiling
Crude ratio claims (e.g., 4:1, 10:1) with UV total absorption
Digitally tracked farm-to-factory cultivation records with DNA barcoding
ESG & FSMA 204 Regulatory Ready
Three core market dynamics are driving international contract supply agreements:
1. The Migration Toward Standardized Molecular Biomarkers: Crude extraction ratios are being phased out by multinational brands. Global regulators are turning away from non-specific UV spectrophotometric polysaccharide assays—which can be inflated by added starches or maltodextrins—in favor of targeted chromatographic quantification (HPLC, GC-MS). Qualified procurement teams require HPLC-verified allicin, monomeric epigallocatechin gallate (EGCG), pure L-theanine, or distinct hydroxycinnamic acid percentages supported by certified chromatogram printouts for every production lot.
2. Clean-Label, Solvent-Free Extraction Protocols: Heightened scrutiny from the European Chemicals Agency (ECHA) and United States FDA has marginalized Class 1 and Class 2 solvents. Contemporary formulation designs prioritize aqueous extractions, certified organic grain ethanol solvents, and subcritical/supercritical CO2 systems. Clean extraction guarantees zero toxic volatile residues, eliminating Proposition 65 compliance alerts and easing cross-border customs acceptance.
3. Engineered Particle Mechanics for Fast-Paced Formulations: Raw botanical powders often suffer from poor flowability, high hygroscopicity, and inconsistent water solubility, creating bottlenecks on high-speed encapsulation and tableting lines. Global manufacturers now expect integrated physical engineering—such as fluid-bed agglomeration, microencapsulation, and uniform mesh distribution—to deliver free-flowing, dust-free powders that disperse instantly into clear solutions for modern ready-to-drink (RTD) mixes and effervescent delivery formats.
Industry Innovation Roadmap
Emerging Development Trends in Plant Extraction Technology
The botanical extraction sector is experiencing a technological evolution driven by green bio-manufacturing, synthetic biology integration, and precision delivery formats. Leading contract manufacturers are innovating along three clear trajectories:
Enzyme-Assisted Extraction (EAE)
Cell walls of lignified foliage contain cellulose, hemicellulose, and pectin complexes that trap target actives. Applying targeted food-grade pectinases and cellulases degrades these cellular barriers under mild conditions (40°C–50°C), increasing yield by 20% to 35% without thermal degradation of active phytochemicals.
Targeted Macroporous Polymeric Systems
Modern multi-bed chromatographic resin systems allow selective molecular separation based on polarity and size exclusion. This enables our chemical engineers to purify target polyphenols to ≥98% purity while efficiently scrubbing residual agricultural impurities and heavy metal residues down to sub-part-per-million levels.
Sub-Micron Liposomal Encapsulation
Hydrophobic botanical compounds—such as carotenoids, sea buckthorn oil lipids, and fat-soluble vitamins—suffer from low human gastrointestinal bioavailability. Micro-fluidized liposomal matrices wrap these actives in clean sunflower lecithin bilayers, boosting cellular uptake up to six-fold while eliminating organoleptic bitterness.
Enterprise Manufacturing Capabilities
Why Partner with Shaanxi Torzi Biotech Co., Ltd.?
Shaanxi Torzi Biotech Co., Ltd. is a vertically integrated, on-site SGS-assessed botanical manufacturer based in Xi'an, China. Operating across 12,447 square meters of modern production and warehousing space, we combine over two decades of extraction heritage with an established 17-year international export presence across 50+ countries.
Fully Audited & Certified
Our production facilities maintain active USDA Organic, Halal, Kosher, and ISO9001 certifications, supported by verified third-party SGS factory audit credentials.
Full Turnkey OEM/ODM Formats
We provide full white-label and contract packaging services: two-piece vegetarian HPMC capsules, multi-ingredient stick packs, PET packaging, and custom bottling from an accessible 500-unit minimum run.
Exhaustive Analytical Testing
Our QA lab operates Shimadzu HPLC arrays, Gas Chromatography (GC), Atomic Absorption Spectrometers (AAS), and moisture analyzers to verify chemical purity and safety on every batch.
Procurement Due Diligence
Frequently Asked Questions (FAQ) for B2B Importers
What parameters are documented on batch Certificates of Analysis?
Every commercial batch ships with an authoritative, lot-specific COA covering active marker potency (HPLC/UV), visual appearance, mesh analysis, moisture content, total ash, residual solvents (USP <467>), heavy metals (Pb, As, Cd, Hg via AAS/ICP-MS), and comprehensive microbiological profiling.
What are the minimum order quantities (MOQ) for bulk & OEM runs?
For catalog bulk extract powders, standard pilot MOQs begin at just 1 kg to 25 kg per lot, allowing your R&D team to complete small pilot runs. Custom private-label capsule manufacturing or bespoke packaging formats typically start at 500 units.
How do you safeguard sensitive extracts against transit degradation?
Our standard export packaging utilizes food-grade double polyethylene inner bags heat-sealed within heavy-duty aluminum foil barrier pouches, packed into 25kg fiber drums. Hygroscopic or oxygen-sensitive items can be packed with pharmaceutical desiccants and nitrogen flushed.
Can Torzi Biotech support custom specifications or extraction ratios?
Yes. Our in-house pilot laboratory develops tailor-made extraction parameters, customized carrier options (e.g., maltodextrin-free rice flour or acacia gum), standardized particle sizes from 40 to 200 mesh, and specialized water-soluble grades.
Ready to Qualify Your Next Direct Botanical Manufacturer?
Connect with our technical formulation engineers to request sample lots, chromatographic assay sheets, and contract pricing. Inquiries receive comprehensive responses within one business day.