B2B Pure Botanical Sourcing · Greater London & UK

Natural Vegetable Powder Factories & Supplier in London

Standardized Dehydrated Botanicals, Superfood Actives & Custom Extraction from an SGS-Assessed 12,447 m² Clean-Chain Facility

Factory Inventory

Precision Vegetable Powders & Botanical Extracts for London Formulators

Direct supply from our audited extraction workshops to London Gateway and Heathrow bonded warehouses. Standardized active ratios, certified microbial thresholds, and tailored mesh distributions for RTD beverages, functional baking, and nutraceutical blending.

Formulating for UK Retail or London Foodservice?

Request comprehensive batch-specific COAs, allergen certificates, and pilot test samples delivered directly to your R&D facility within 3 to 5 business days.

23+
Years Industry Experience
Continuous botanical engineering & precision extraction
12,447 m²
Modern Production Facility
On-site inspected cleanrooms & automated vacuum lines
89
Skilled Technical Staff
Dedicated HPLC, GC, AAS quality engineers & PhD chemists
17 Yrs
Global Export Track Record
Supplying B2B enterprise clients in over 50 nations
Strategic Sourcing Analysis

The London Vegetable Powder Market: Clean-Label Imperatives & Supply Chain Resilience

An authoritative industry whitepaper on navigating procurement requirements across the M25 corridor, Greater London food manufacturing hubs, and the evolving UK regulatory matrix post-Brexit.

HFSS Compliance & Nutrient Density

With the UK government's stringent High in Fat, Salt, and Sugar (HFSS) promotional restrictions reshaping supermarket shelves across London, Tier-1 food brands are actively turning to concentrated vegetable powders. Dehydrated celery, purple yam, and spinach derivatives provide unadulterated functional solids, color saturation, and inherent savory notes without penalizing nutrient profile scores (NPS). London product developers leverage our micro-milled powders to engineer clean labels that satisfy the Department of Health and Social Care (DHSC) mandates effortlessly.

Urban Artisanal Innovation Clusters

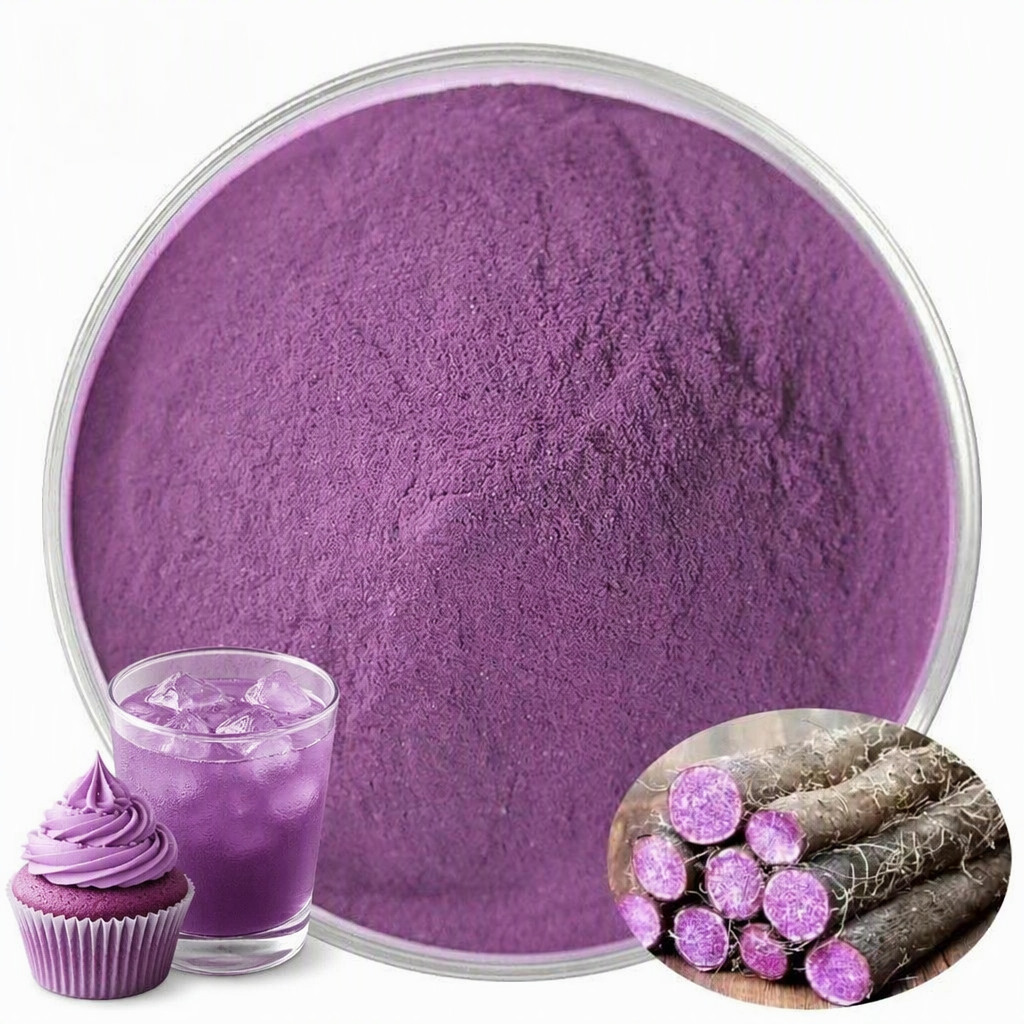
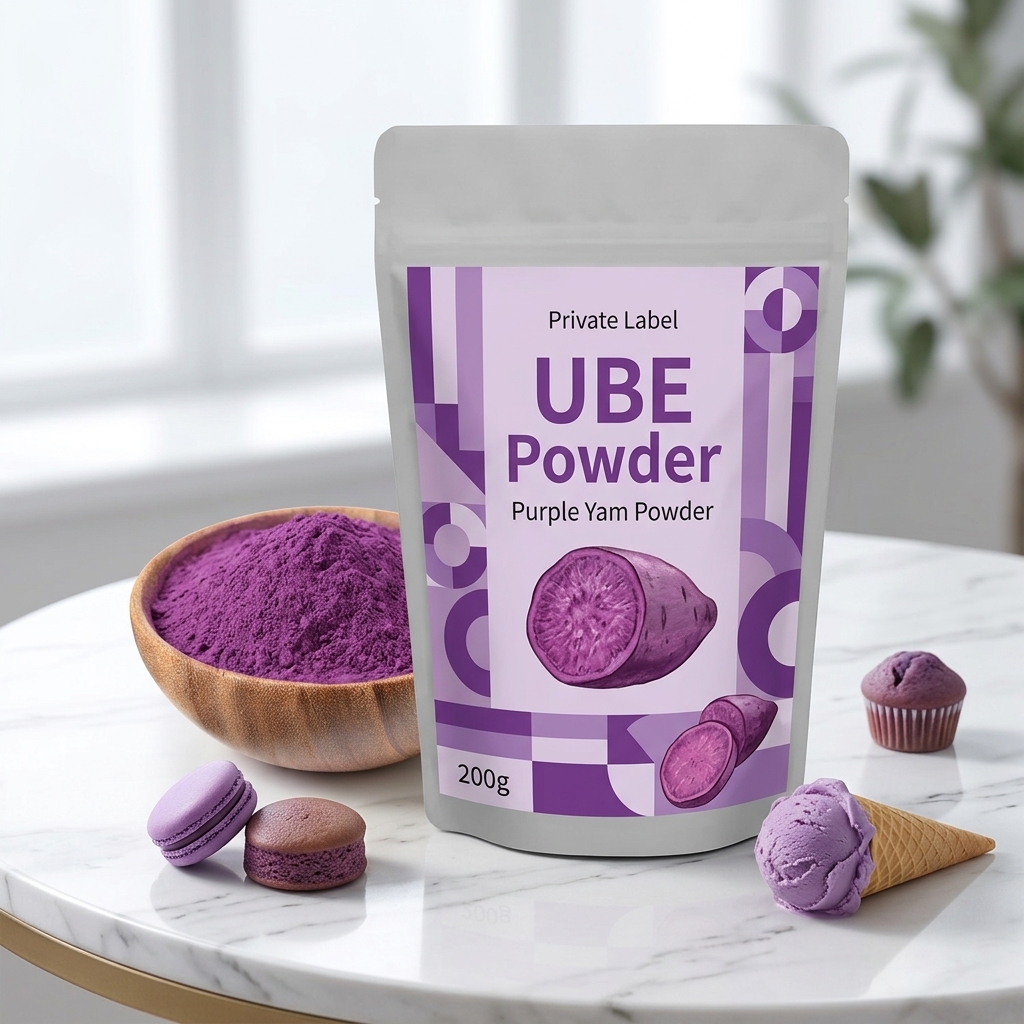
From the industrial bakeries of Park Royal and Bermondsey to cutting-edge craft beverage formulators in Hackney and Shoreditch, London is Europe's epicenter for experiential food culture. Sourcing bright natural colors—such as the vivid magenta anthocyanins from our organic Ube powder or deep chlorophyll greens from brassica extracts—allows brands to bypass artificial E-number colorants (like Allura Red AC or Tartrazine), answering consumer calls for clean-label, plant-powered authenticity in gourmet retail.

Cold-Chain Avoidance & Carbon Footprint

Freight economics within the UK capital dictate extreme spatial and energy efficiency. Fresh vegetable imports from mainland Europe carry volatile spoilage margins, high cold-storage overheads, and hefty carbon penalties under Scope 3 emissions audits. High-density, freeze-dried and vacuum-spray dried vegetable extracts reduce bulk shipping weight by upwards of 92%, offering 24-month ambient shelf stability while maintaining bio-active polyphenols and thermodynamic functionality upon rehydration.

Technical Evaluation: Industrial Dehydration & Extraction Modalities

Understanding how processing thermodynamics impact bulk density, sensory fidelity, enzyme denaturation, and solubility across London commercial processing lines.

Technology Format Core Thermal Range Nutrient / Vitamin Retention Rehydration Kinetics Bulk Density (g/mL) Target Formulation Applications
Freeze-Drying (Lyophilisation) -30°C to -45°C (Sublimation) 95% – 98% (Heat-labile VC & enzymes intact) Instant (< 5 seconds), porous lattice 0.25 – 0.40 Premium infant formulas, superfood blends, nootropic tonics
Vacuum Low-Temp Spray Drying 45°C to 65°C under negative pressure 82% – 90% (Polysaccharides stabilized) High water solubility, zero sediment 0.45 – 0.65 RTD beverages, effervescent drink tabs, clear broths
Superfine Air-Classified Milling Ambient controlled (< 35°C) 88% – 94% (Total dietary fiber preserved) Colloidal suspension, 120–200 mesh 0.50 – 0.70 Extruded meat analogues, vegan pastry doughs, pasta matrices
Dual Hydro-Ethanolic Extraction Controlled reflux (40°C–75°C) Concentrated actives (Triterpenes, Polyphenols) Carrier-dependent (Maltodextrin/Fiber) 0.40 – 0.55 Hard-shell capsules, pharmaceutical sachets, dietary tablets
Localised Case Studies

Engineering Solutions for Greater London's Specialized Manufacturing Segments

From high-throughput bottling lines to craft confectionery kitchens, here is how leading UK food technologists formulate with our plant-derived powders to resolve complex rheological and shelf-life challenges.

Bespoke Bakery & Patisserie

Thermal Stability in Artisan Bread & Sweet Treats

The Formulation Challenge: Commercial pastry and sourdough bakeries across Kentish Town and Richmond struggle with color fading when utilizing fresh purees, alongside excess moisture disrupting the gluten structure.

The Technical Solution: Our micro-milled Organic Ube Powder and freeze-dried vegetable concentrates undergo gentle thermal stabilization during spray crystallization. When folded into high-hydration laminated doughs, the anthocyanin matrix resists oven temperatures up to 215°C without turning brown, preserving radiant violet hue while adding structural crumb stability.

Request Bakery Trial Spec →
Plant-Based Dairy & Ready-to-Drink

Dispersion & Viscosity in Plant-Based Beverages

The Formulation Challenge: Plant-based RTD beverage brands co-packing along the London-M4 corridor face severe sedimentation, grittiness, and phase separation in oat and pea-protein bases.

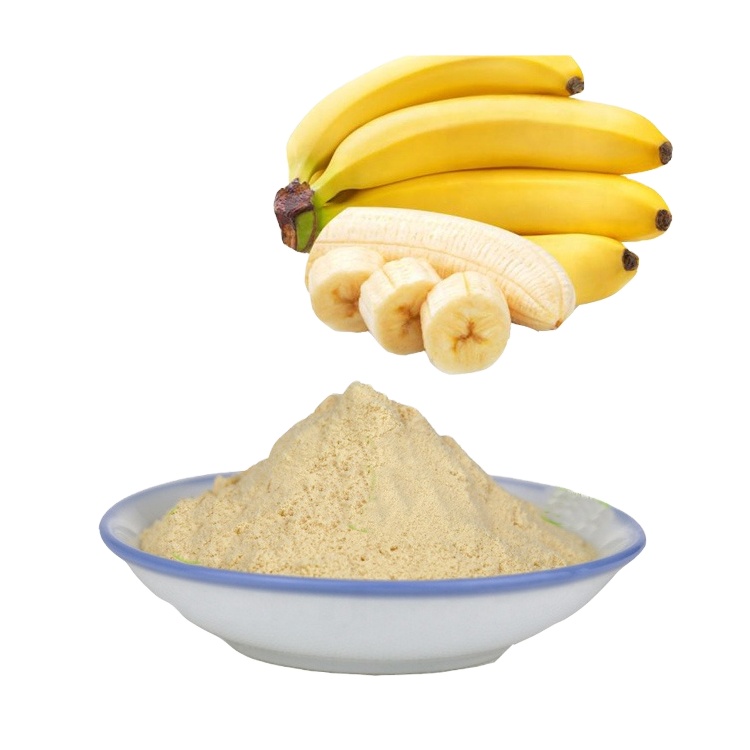
The Technical Solution: Our enzymatic digestion processes and 200-mesh air-classifier ensure that powders like Acerola Cherry, Celery Extract, and Banana solids exhibit an average particle diameter ($D_{90}$) below 45 microns. This allows effortless cold-water dispersion, laminar fluid stability without curdling, and prevents mouthfeel chalkiness.

Request RTD Sample Protocol →
Clinical & Sports Nutrition

Active Homogeneity in Dry Capsule Blending

The Formulation Challenge: Supplement manufacturers operating under cGMP requirements in Hertfordshire and Essex require zero active segregation in high-speed rotary tablet presses and encapsulators.

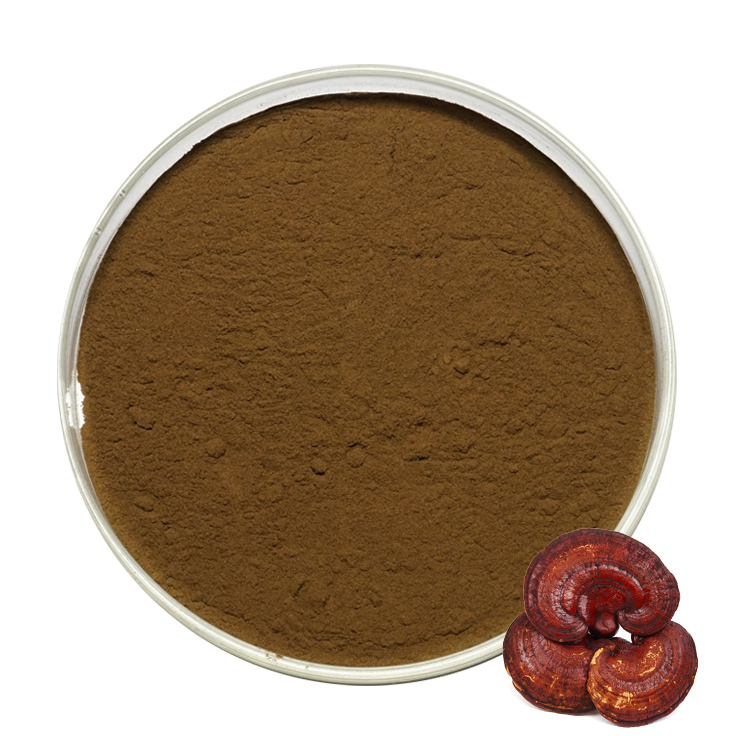
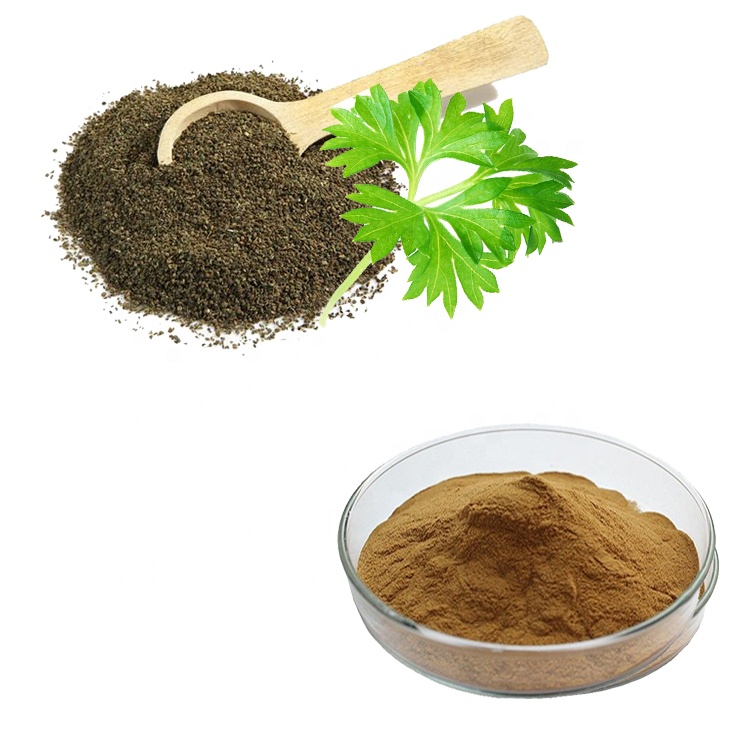
The Technical Solution: Standardizing active botanicals like Reishi Ganoderma and Celery Seed Extract with certified moisture content (<5.0%) and precise tapped density (0.45–0.58 g/mL) ensures uniform flowability (Hausner ratio < 1.20). This eradicates static clumping and guarantees content uniformity per capsule without synthetic flow lubricants.

Request cGMP Encapsulation Data →
Production Prowess

Inside Torzi Biotech: A Proven 12,447 m² Extraction Powerhouse

Unlike regional traders and intermediaries, Shaanxi Torzi Biotech Co., Ltd. operates a vertically integrated production infrastructure nestled near the mineral-rich Qinling botanical belt, combined with rigorous European standard export controls.

SGS On-Site Audited Cleanliness

Torzi Biotech has successfully cleared comprehensive on-site factory assessments conducted by SGS Group. Our GMP-designed extraction cleanrooms minimize any potential cross-contamination, ensuring full compliance with UK Food Standards Agency (FSA) standards and British Retail Consortium Global Standards (BRCGS) raw ingredient thresholds.

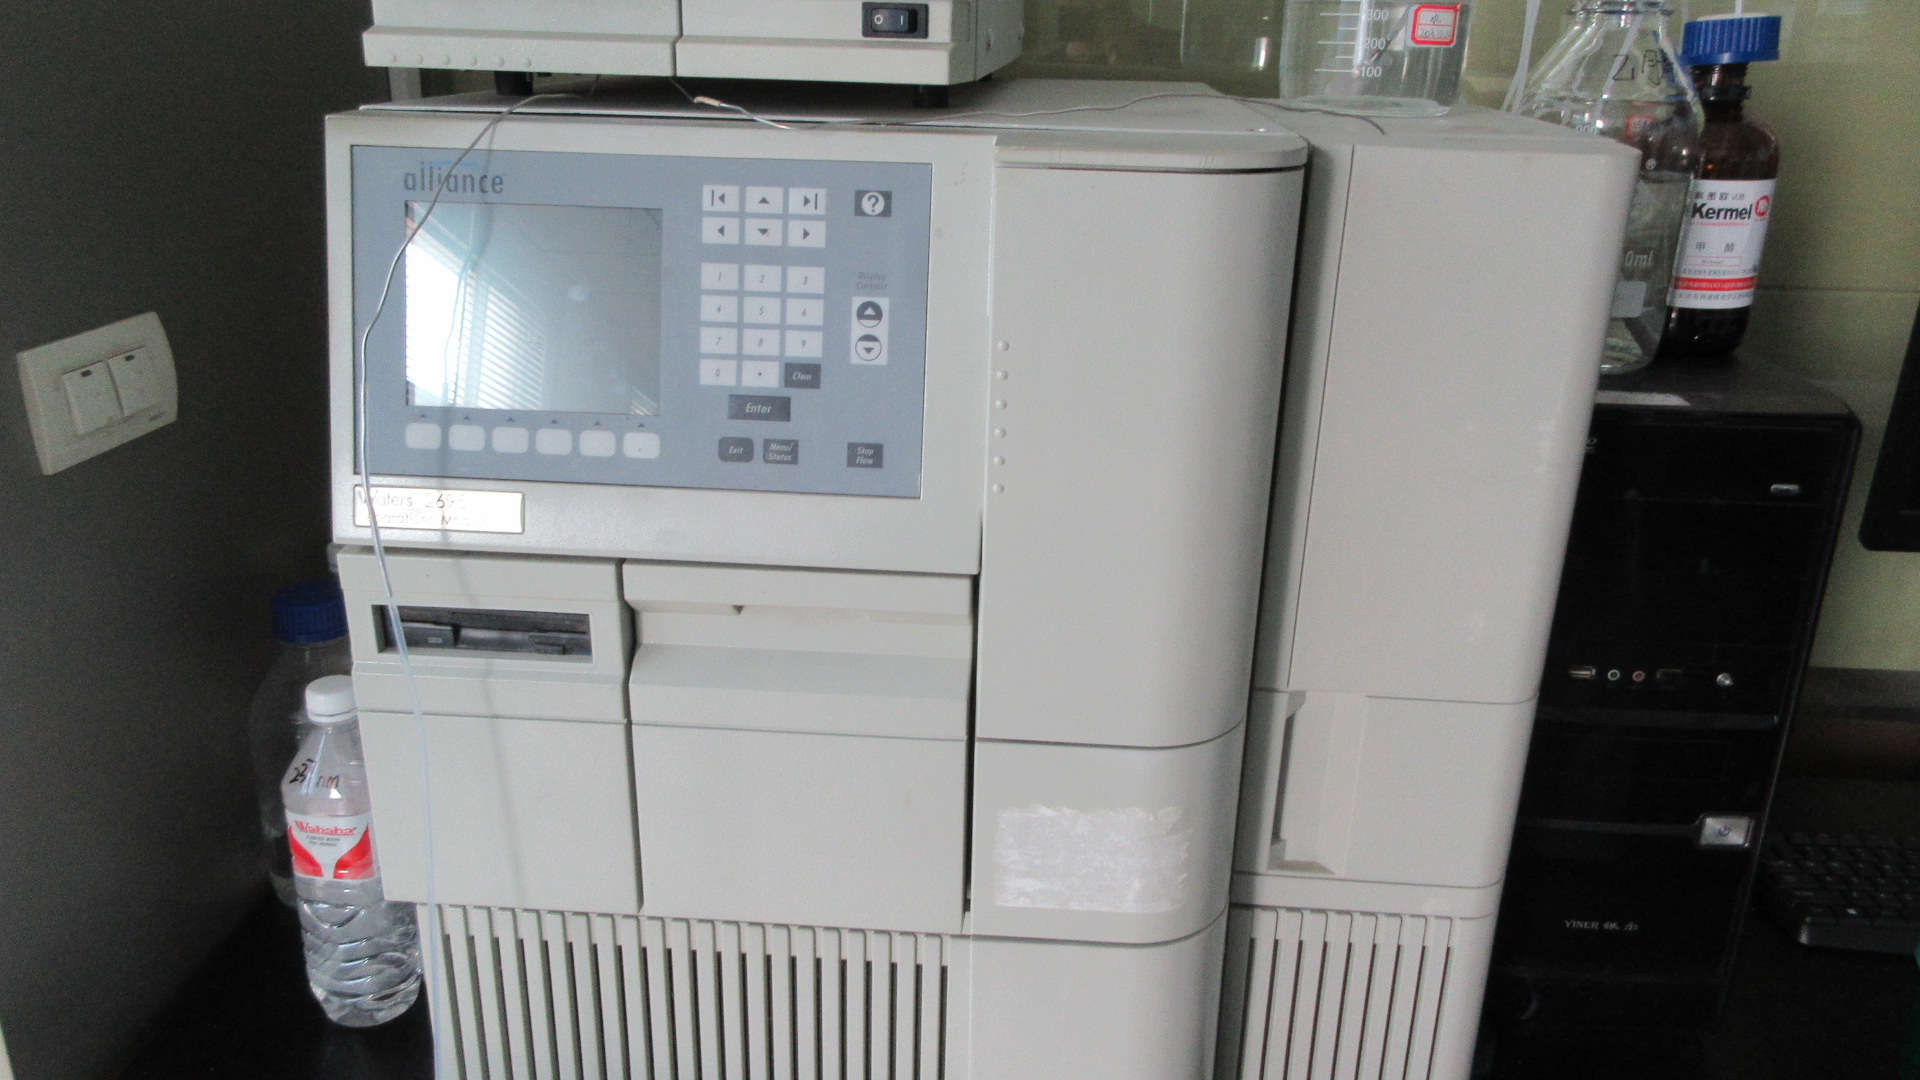
State-of-the-Art Laboratory Instrumentation

Every single batch that heads to London undergoes exhaustive instrumental validation. Our in-house testing complex is equipped with High-Performance Liquid Chromatography (HPLC), Gas Chromatography (GC), Atomic Absorption Spectrophotometers (AAS), and Atomic Fluorescence Spectrometers to quantify actives and guarantee heavy metal exclusion (Pb, As, Cd, Hg).

Dual Retention & Full Traceability

We maintain physical retention samples of raw input botanicals, intermediate concentrates, and final sieved powders for a minimum of 36 months. With full lot code linkage, your London quality assurance team can trace any drum back to its precise farming cooperative, extraction date, and spray tower parameters.

End-to-End Extraction & Refining Architecture

Stage 01

Botanical Selection

GAP-certified raw botanicals undergo botanical ID verification, moisture checking, and initial heavy metal screening.

Stage 02

Low-Temp Extraction

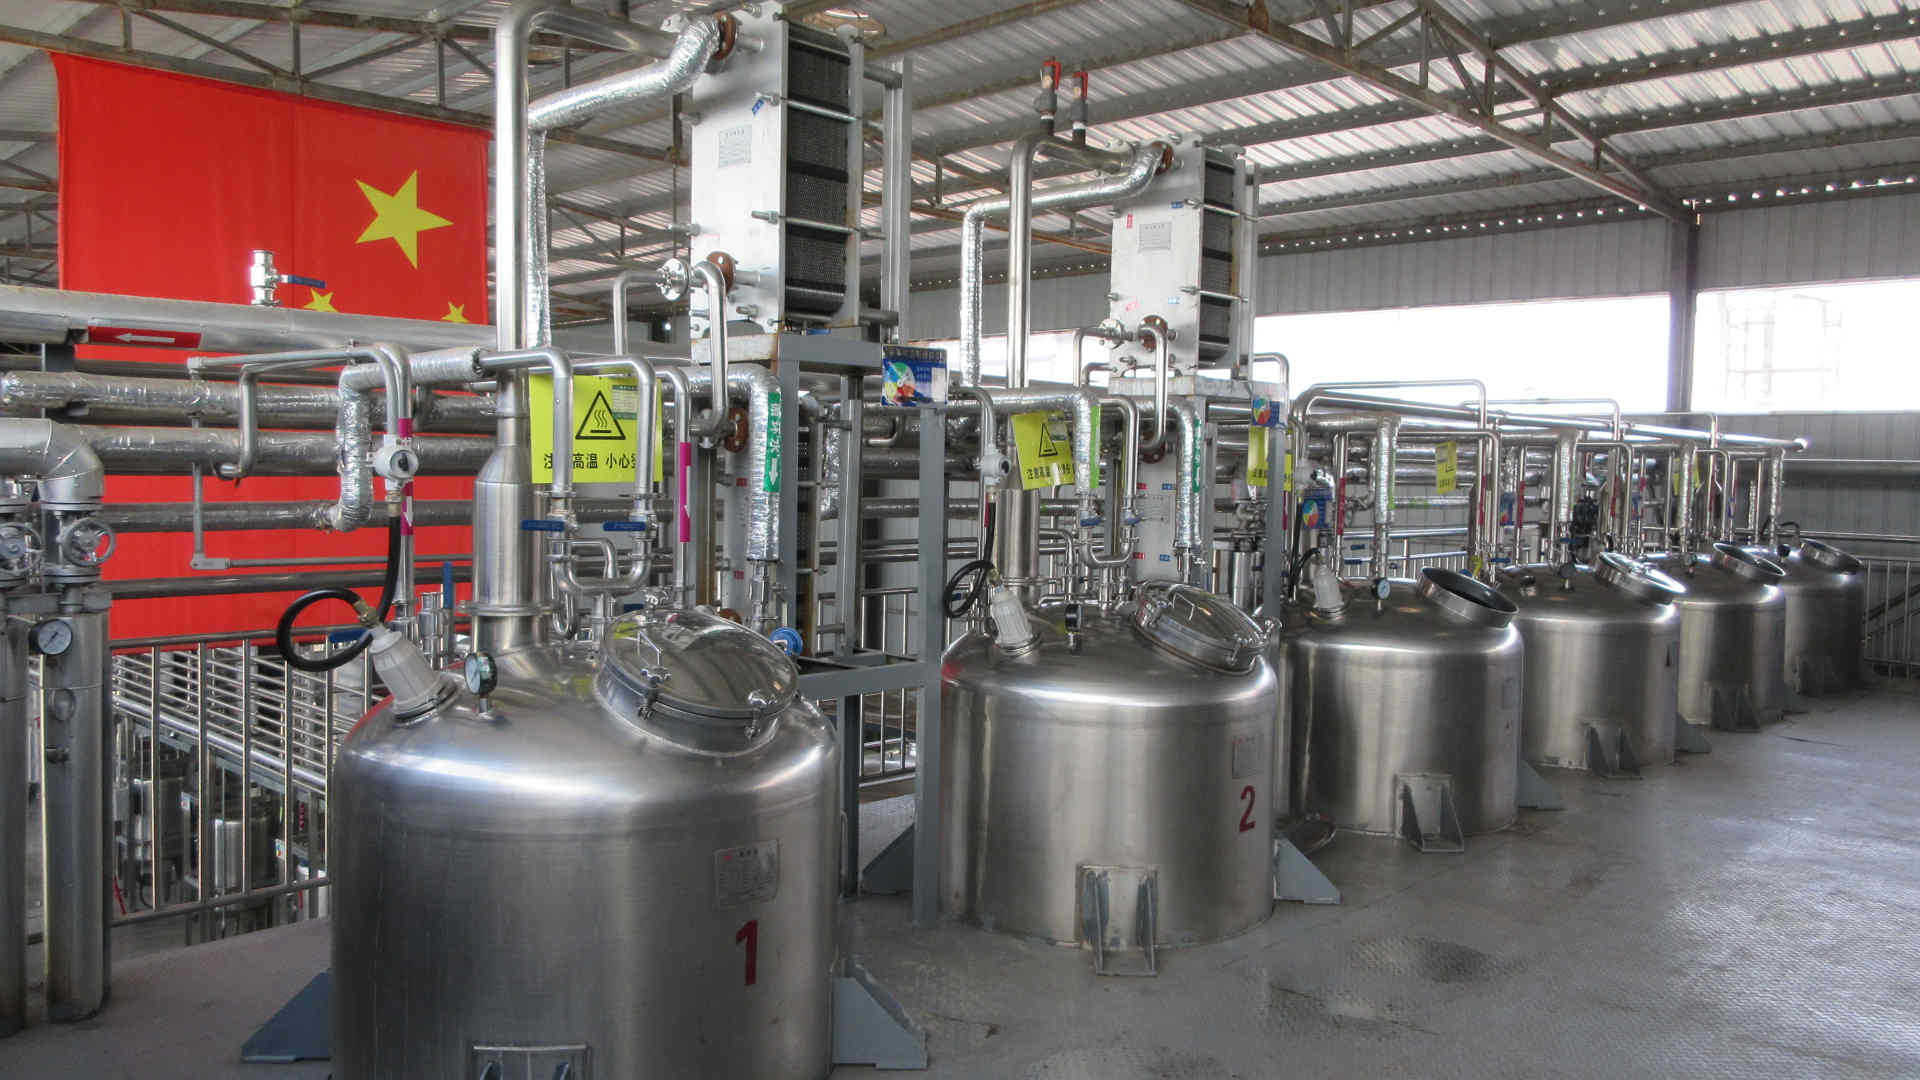
Stainless steel dynamic tanks extract target phytonutrients using purified demineralized water or bio-ethanol.

Stage 03

Membrane Clarification

Multi-stage disc stack centrifugation and ultrafiltration remove insoluble cellulosic debris, maximizing clarity.

Stage 04

Resin Adsorption

Macroporous resins selectively enrich target flavonoids and active polysaccharides while discarding unwanted impurities.

Stage 05

Vacuum Concentration

Falling film low-temperature evaporation protects heat-vulnerable micronutrients against thermal degradation.

Stage 06

Aseptic Spray Drying

Micro-droplet spray drying towers atomize liquid extract into uniform, free-flowing crystalline powder spheres.

Stage 07

Homogenization & Sieving

Double-cone ribbon blenders and 80–200 mesh vibrating sieves ensure lot-to-lot batch uniformity and granulometry.

Stage 08

Cleanroom Packaging

Class 100,000 cleanroom packaging in nitrogen-purged double food-grade PE bags inside tamper-evident fiber drums.

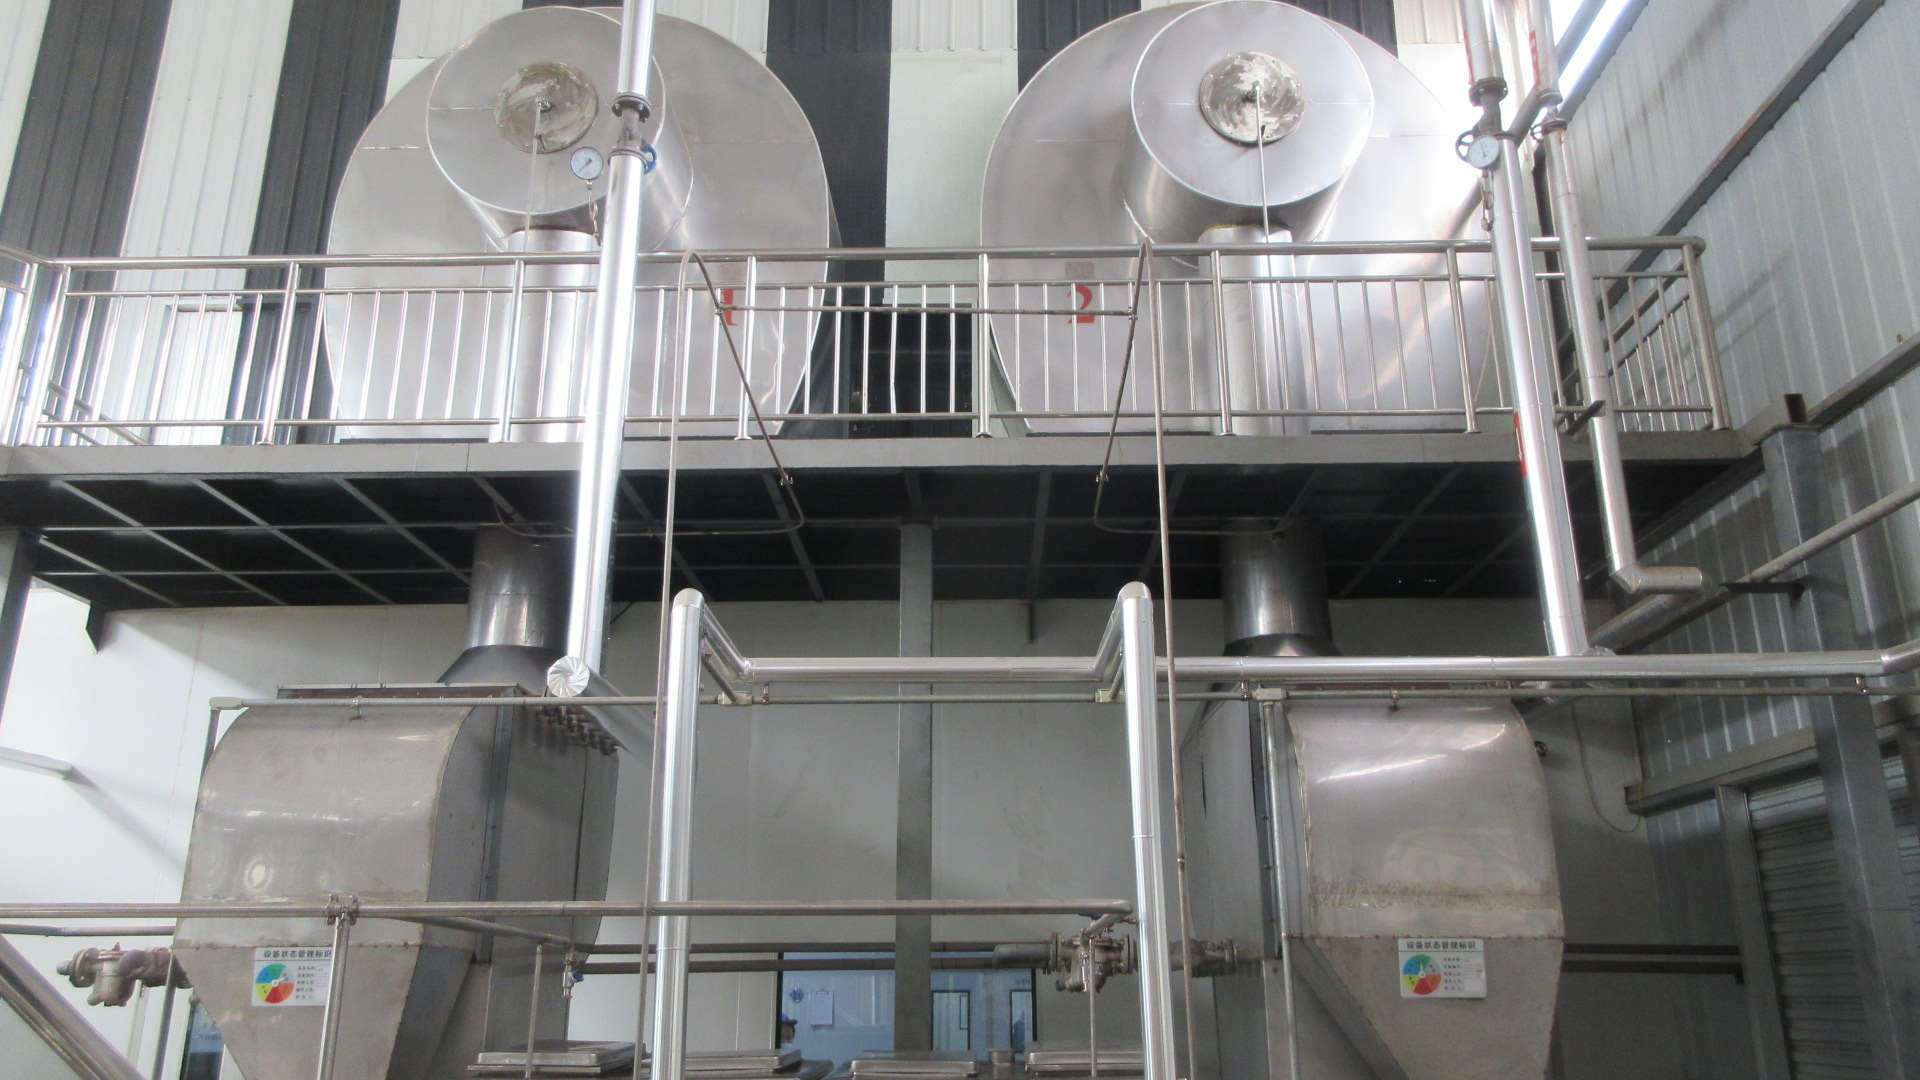
Industrial Extraction Tank System
Multi-Ton SS316 Extraction Units
Spray Drying Tower Facility
Precision Spray Atomization Tower
HPLC Analytical Testing Laboratory
High Performance Liquid Chromatography
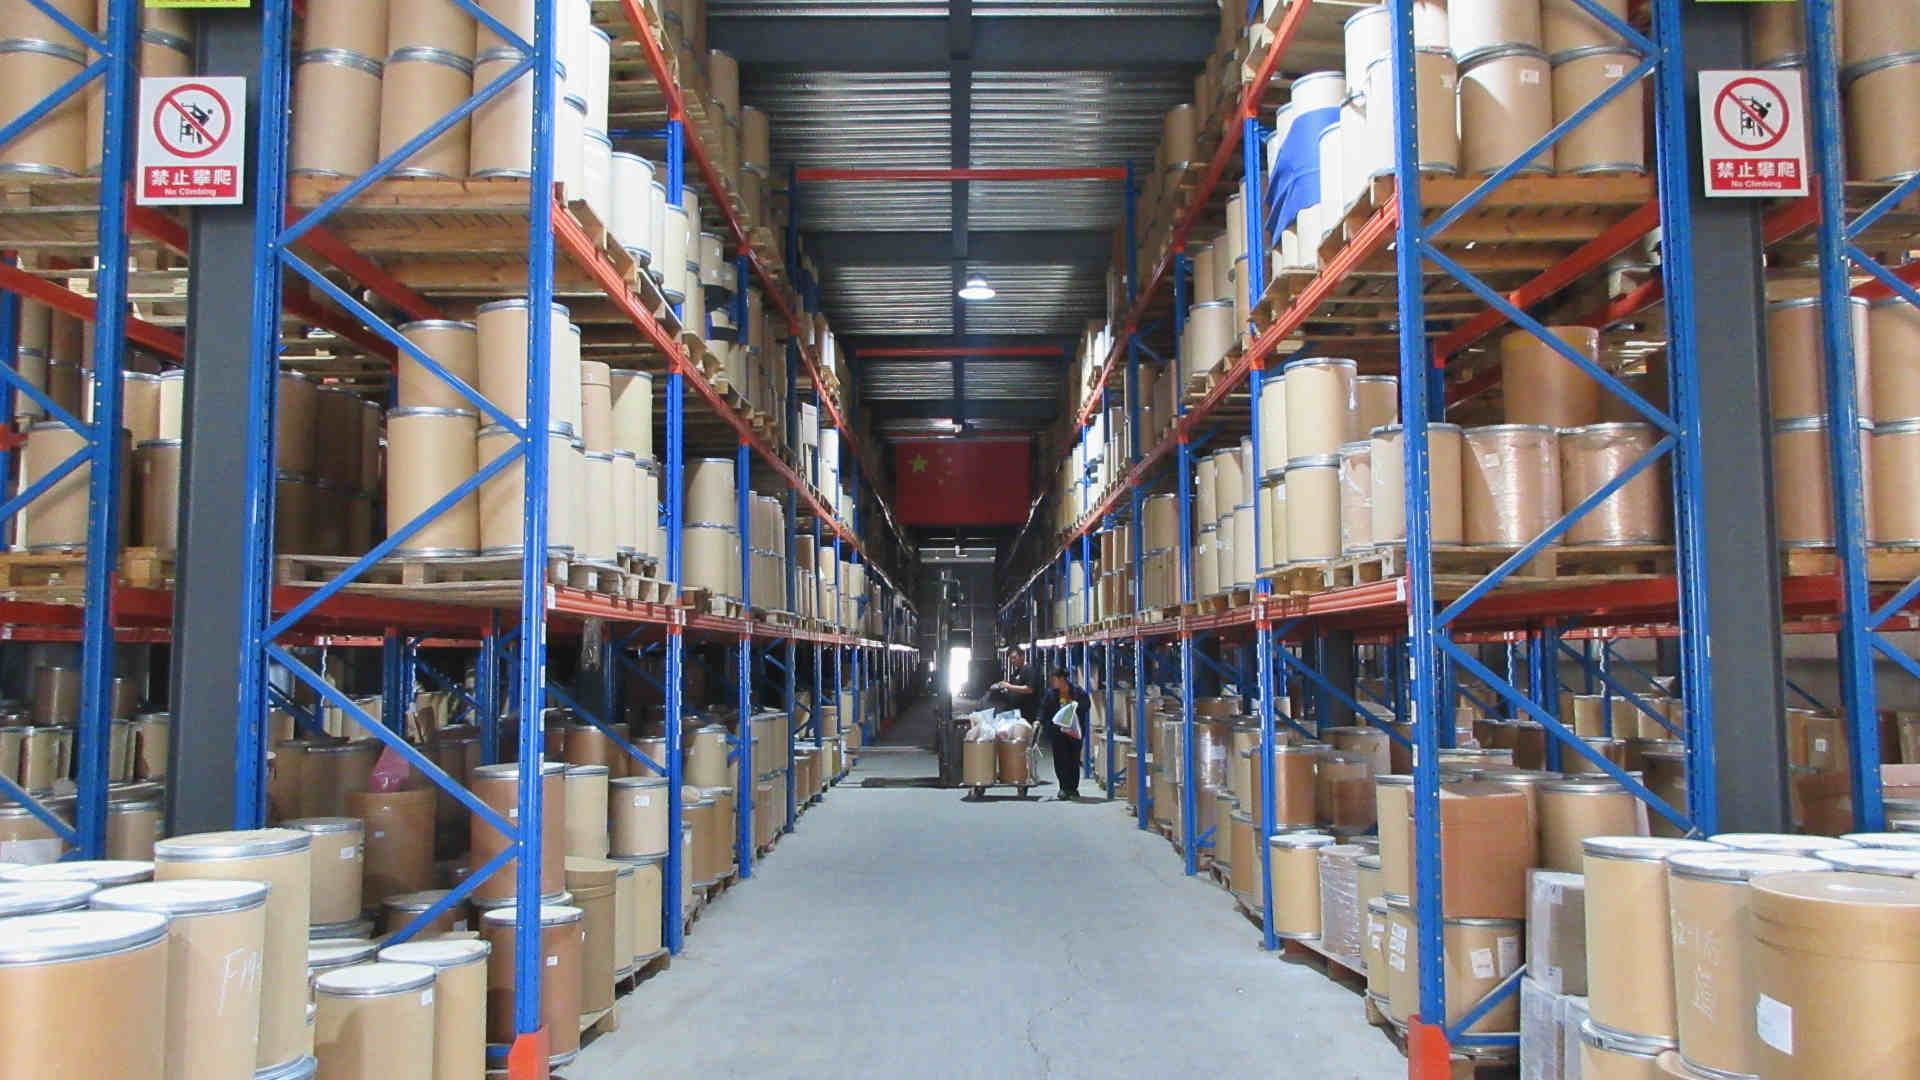
Export Warehouse and Logistics Packing
Climate-Controlled Export Warehouse
Regulatory & Logistics Protocol

Navigating UK Import Compliance, Customs Duties & FSA Guidelines

A comprehensive roadmap for London procurement directors ensuring zero customs friction, total food law adherence, and streamlined sea and air port clearance.

UK FSA & Novel Foods Status

Navigating post-EU regulations in the UK requires verified legal qualification. All standard vegetable powders supplied by Torzi Biotech (e.g., Celery, Purple Yam, Banana, Acerola) possess well-documented history of consumption across the UK and the European Union prior to May 1997, thereby fully exempt from onerous Novel Food Authorisation delays under assimilated Retained EU Regulation 2015/2283.

Pesticide MRLs & Contaminant Screen

UK Maximum Residue Limits (MRLs) for plant protection substances are among the most stringent globally. Torzi Biotech screens all botanical lots against multi-residue LC-MS/MS panels covering 500+ agrochemical markers. We guarantee compliance with UK Statutory Instruments regarding Polycyclic Aromatic Hydrocarbons (PAHs), Dioxins, and Aflatoxins (B1, B2, G1, G2).

London Port Clearance & Tariffs

Our experienced export documentation desk handles direct DDP, CIF, and FOB shipments into major UK ports including London Gateway (Thurrock), Port of Felixstowe, and Port of Southampton, alongside rapid air cargo into London Heathrow (LHR). We provide precise UK Trade Commodity Codes (HS Codes), Certificates of Origin (CO), Phytosanitary Certificates, and full packing lists.

Procurement Intelligence

Frequently Asked Questions: Sourcing Vegetable Powders in London

Answers to technical, logistical, and commercial inquiries routinely posed by UK quality assurance directors, purchasing managers, and product innovation leads.

What is the typical transit duration from your factory to our manufacturing hub in London?

For expedited R&D trials or seasonal inventory crunches, air freight direct to London Heathrow (LHR) averages 4 to 7 business days from dispatch, including customs release. For bulk commercial containers (FCL/LCL), ocean freight landing at London Gateway or Felixstowe ranges between 26 to 32 days. We coordinate bonded clearance through trusted UK freight handlers to prevent domestic distribution hold-ups along the M25.

How do you safeguard hygroscopic powders from moisture uptake during maritime transit?

Vegetable powders—particularly freeze-dried fruit powders like banana and pure vegetable roots like yam—exhibit extreme natural hygroscopicity. We pack our materials inside dual pharmaceutical-grade low-density polyethylene (LDPE) liners, sealed with ultrasonic heat binders and secondary vacuum barrier closures. This is enclosed inside high-strength kraft fiberboard drums with interior silica desiccant packs, guaranteeing zero caking or clumping throughout variable humid marine routes.

Can you provide custom particle sizes (mesh distribution) for specialized beverage and capsule equipment?

Yes. Our engineering facilities feature closed-loop cryogenic air-classifier mills allowing customizable particle size outputs from 60 mesh (granular, anti-dusting) up to 200 mesh (superfine, colloidal dispersion). If your blending setup in London requires specific bulk density constraints to match high-speed filling hoppers, our technical team can calibrate granulating passes accordingly.

What specific quality documentation accompanies each commercial batch shipment?

Every lot leaves our plant with a comprehensive Certificate of Analysis (COA) containing batch-specific HPLC or UV assay figures, organoleptic indices, moisture, ash content, microbial enumeration (Total Aerobic Plate Count, Yeast & Molds, Salmonella negative in 25g, E. Coli negative), and heavy metals tested via atomic absorption spectrophotometry. Additional Allergen Declarations, Non-GMO Statements, and TSE/BSE Free statements are provided standard.

Do you support pilot-scale Minimum Order Quantities (MOQs) for UK FMCG startups?

We actively support London's vibrant food startup ecosystem. While our standard manufacturing lines are designed for multi-ton outputs, we maintain dedicated pilot runs with MOQs as low as 1 kg to 25 kg across core stock items like Reishi Mushroom Extract, Celery Seed Extract, and Organic Ube Powder. This enables local formulators to finalize benchtop trials and organoleptic testing before committing to large commercial volumes.

Are your botanical ingredients certified for Halal, Kosher, and Organic product lines?

Yes. Our extraction facility holds internationally validated USDA Organic, Halal, and Kosher certifications. If your retail product lines target specialized dietary demographics in London and European retail stores, we provide batch-specific religious and organic transaction certificates upon request.

Direct Commercial Liaison

Request Your Batch Quotation & Technical Dossier

Connect directly with our senior botanical ingredients export team. Receive detailed technical specifications, full regulatory documentation, transparent freight rate breakdowns for London delivery, and complimentary pilot testing samples.

Shaanxi Torzi Biotech Co., Ltd. · Verified Supplier Assessment by SGS Group · Rapid Email Turnaround Within 24 Business Hours