High-Potency Concentrated Herbal & Functional Botanical Extracts
Engineered via multi-stage column chromatography, vacuum concentration, and low-temperature flash drying to guarantee intact active molecular weights and rapid thermodynamic solubility across nutraceutical and functional beverage applications.
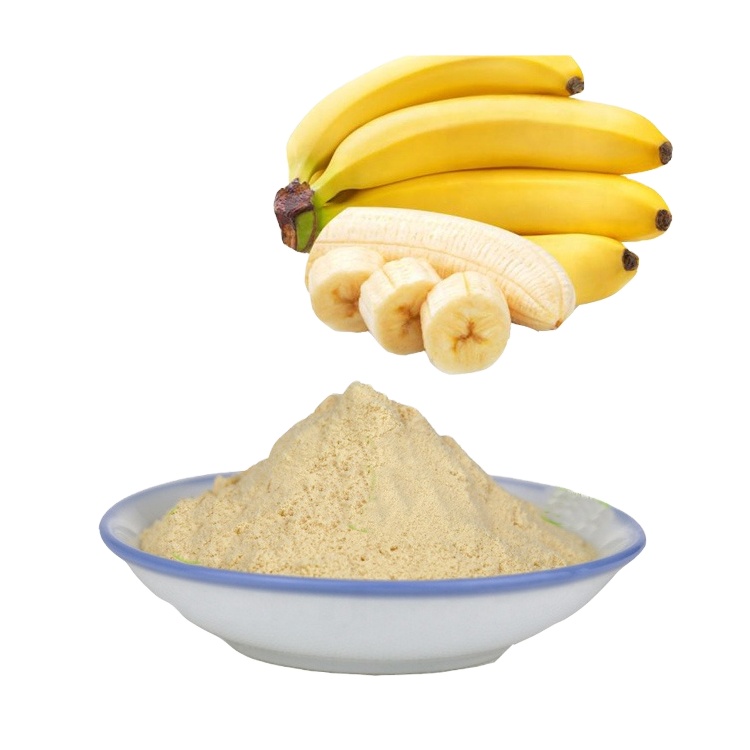 100% Organic
Freeze Dried Pure Organic Banana Fruit Powder
Sublimation-preserved potassium, native pectin, and organic prebiotic fiber. Zero maltodextrin carrier; instant reconstitution.
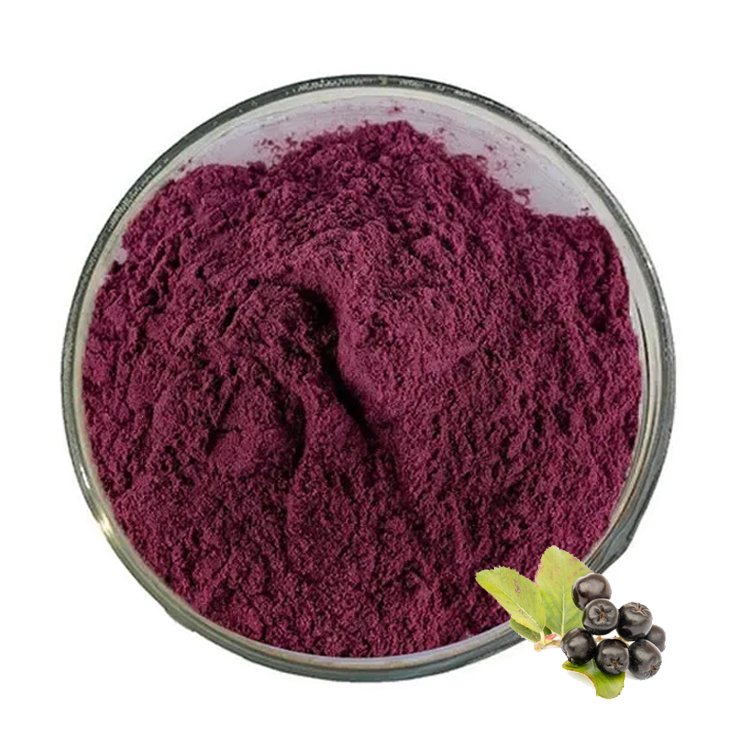 High ORAC
Water-Soluble Acai Berry Extract Powder (Anthocyanins)
Standardized anthocyanin & polyphenol complex. Cold-spray refined for clarifiable, residue-free RTD beverage formulation.
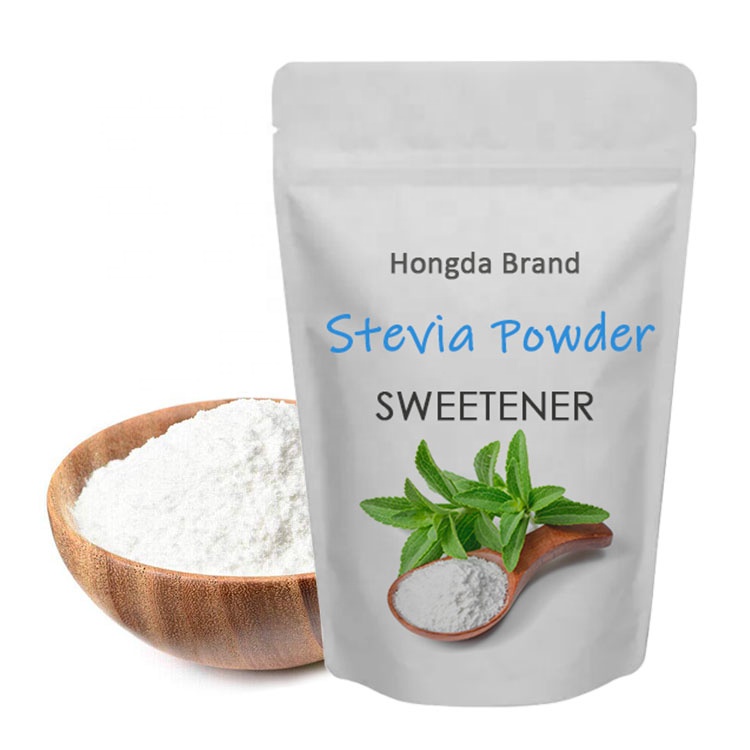 RA 98%
Stevia Extract Powder | 98% Steviol Glycosides (Reb-A)
High Reb-A glycoside purification delivering 350x sucrose equivalence without bitter secondary aftertaste. Zero glycemic index.
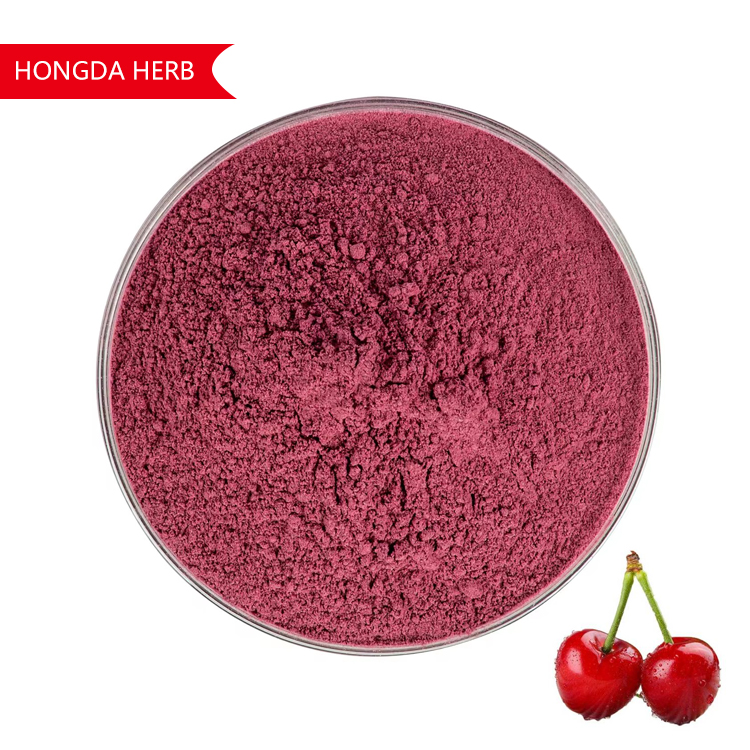 Natural VC
Acerola Cherry Extract Powder (Natural L-Ascorbic Acid)
Naturally derived 17% and 25% Vitamin C verified by titration and HPLC. Preserves synergistic bioflavonoids for superior bioavailability.
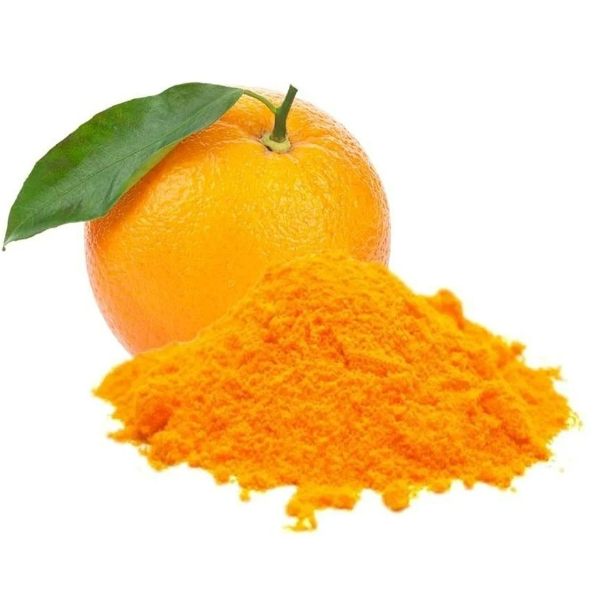 Instant Dispersion
Spray-Dried Sweet Orange Juice Concentrate Powder
Micro-encapsulated natural citrus aroma and essential terpenes. Highly resistant to caking; optimized for sports powder sticks and tablets.
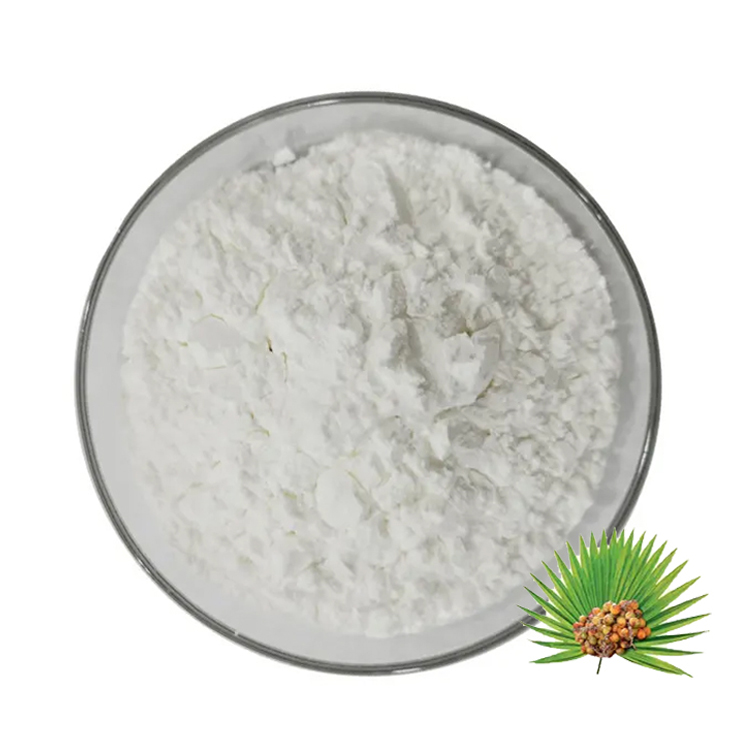 Sterols & Lipids
Saw Palmetto Extract Powder (25%, 45%, 85% Fatty Acids)
Supercritical CO2 extract micro-encapsulated into a free-flowing, odorless powder. Standardized total fatty acids & beta-sitosterol.
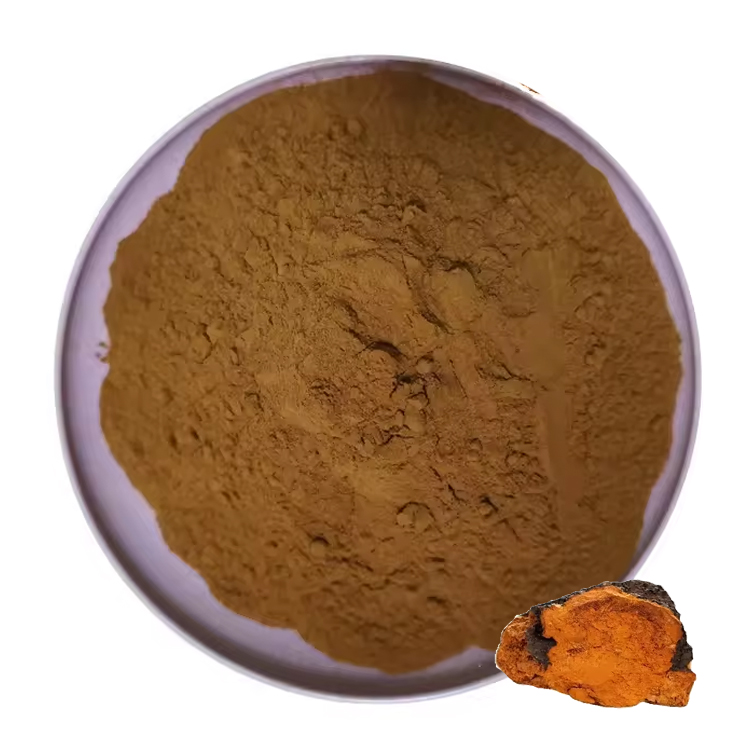 Wild Harvested
Chaga Mushroom Extract (Inonotus Obliquus) Polysaccharides
Dual-extracted sclerotium standardized to 30%-50% Polysaccharides, 20% Beta-Glucans (Megazyme method), and betulinic acid.
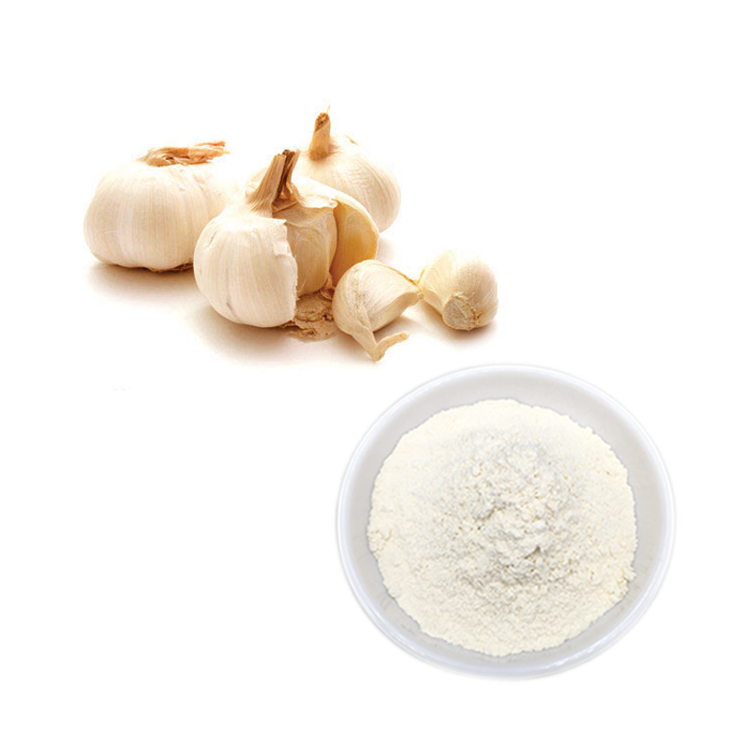 High Allicin
Hongda Standardized Dehydrated Garlic Extract Powder
Low-temperature dehydrated Allium sativum with stabilized alliin and allicin yield. Meets international pharmacopoeial microbiological criteria.
Engineering Principles of Concentrated Herbal Extractions: Solvent Partitioning, Molecular Selectivity, and Analytical Integrity
In modern pharmaceutical and nutraceutical supply chains, the term "Concentrated Herbal Extract" has transcended crude decoction reductions. Modern B2B procurement leaders demand verifiable molecular concentration profiles where bioactive monomers—such as polyphenols, triterpenoids, polysaccharides, and lipidic sterols—are selectively concentrated while pesticide residues, heavy metals, and carrier bulking agents are eliminated. Shaanxi Torzi Biotech executes this selective separation through an orchestrated balance of thermodynamic control, continuous counter-current solid-liquid extraction, macroporous resin adsorption chromatography, and aseptic vacuum spray drying.
1. Chromatographic Purification vs. Native Extraction Ratios
A prevalent discrepancy in bulk botanical importing is the ambiguity between standardized extracts and ratio extracts (e.g., 10:1 vs. 50:1). Historically, ratio claims were exploited by unscrupulous brokers relying on maltodextrin dilution or inflated dry-weight math. At our Xi'an manufacturing complex, our engineering framework prioritizes Active Compound Target Standardization verified via High-Performance Liquid Chromatography (HPLC) and Gas Chromatography (GC).
For example, in our Saw Palmetto (Serenoa repens) line, fatty acid recovery is not simply concentrated through heat distillation, which degrades delicate linoleic and oleic acids. Instead, we utilize supercritical CO₂ fluid extraction at 31.1°C and 73.9 bar pressure, generating dense lipid matrices up to 85% total fatty acids without residual solvents. Similarly, our Acerola Cherry (Malpighia glabra) extract is processed via gentle tangential ultrafiltration to retain natural L-ascorbic acid bonded to rutin and bioflavonoids, preventing thermal oxidation.
2. Solving Beta-Glucan & Polysaccharide Analytical Fallacies
Within functional fungi extracts such as Chaga (Inonotus obliquus) and Lion's Mane (Hericium erinaceus), conventional UV spectrophotometric assays (e.g., the Phenol-Sulfuric Acid method) are notoriously vulnerable to false-positive inflation caused by alpha-glucans, dextrins, and residual starch from grain substrates. Torzi Biotech enforces the Megazyme Enzymatic Assay Protocol across all batches. By enzymatically breaking down non-structural starches and quantifying purified 1,3-1,6 beta-D-glucans, our technical COAs provide formulate-ready assurance that your label claims reflect actual therapeutic immunomodulators, not adulterated grain fillers.
| Botanical Monomer | Standardized Target Active | Assay Methodology | Solvent Residue Spec (USP <467>) | Heavy Metal Compliance (ICP-MS) |
|---|---|---|---|---|
| Stevia Rebaudiana | Rebaudioside A ≥ 98.0% | HPLC-UV Column C18 | Ethanol < 5,000 ppm / Methanol < 50 ppm | Pb < 0.5 ppm, As < 0.5 ppm, Cd < 0.1 ppm |
| Serenoa Repens (Saw Palmetto) | Total Fatty Acids 25% - 85% | GC-FID (Capillary Column) | Solvent-Free (Supercritical CO₂) | Pb < 1.0 ppm, As < 0.5 ppm, Hg < 0.1 ppm |
| Malpighia Glabra (Acerola) | Natural Vitamin C 17% - 25% | HPLC / Redox Titration | 100% Deionized Aqueous Extraction | Compliant with EU EC 1881/2006 |
| Inonotus Obliquus (Chaga) | β-Glucan ≥ 20%, Polysaccharides ≥ 40% | Megazyme Enzymatic + UV | Aqueous-Ethanol Dual Extraction | Pb < 0.2 ppm, As < 0.2 ppm, Cd < 0.05 ppm |
| Euterpe Oleracea (Acai) | Anthocyanins 5% - 15%, ORAC > 120,000 | HPLC / Spectrophotometric | Aqueous Low-Temperature Filtration | USP <2232> Dietary Supplement Limits |
Future Procurement Trends Reshaping the Global Extract Market
Global nutraceutical brands are navigating heightened regulatory rigor and supply-chain scrutiny. To stay competitive, contract procurement teams must align with four irreversible purchasing developments over the 2025–2030 horizon.
1. Transition from Ratios to Verified Monomers
Global regulatory bodies like the FDA, EFSA, and TGA are increasing scrutiny of nondescript "10:1" extracts. Sourcing departments now demand strict quantitative marker profiling (e.g., specific steviol glycoside ratios, fatty acid isomers, or L-theanine optical purity) through standardized HPLC batch releases.
2. Green Chemistry & Solvent-Free Mandates
Strict European bans on petroleum residues, ethylene oxide (EtO), and chlorinated hydrocarbons have forced brands away from hexane and ethyl acetate. Clean water extractions, food-grade hydroethanolic partitioning, and high-pressure subcritical water are the baseline qualification criteria for global importers.
3. Instant Solubility for Functional Beverages
Functional drinks, effervescent tablets, and stick-pack RTDs demand botanical powders that dissolve cleanly without flocculation, gritty sedimentation, or turbidity. Particle micronization (120 to 200 mesh) combined with vacuum fluid bed agglomeration is now a prerequisite specification.
4. Transparent DNA & Soil-to-Drum Traceability
Adulteration with synthetic biomimetic chemicals or lower-species substitutes is an existential threat to supplement brands. Advanced buyers require DNA barcoding, stable isotope ratio mass spectrometry (IRMS), and complete farm-level traceability before issuing purchase orders.
A Vertically Integrated Extraction Facility: Real Manufacturing, Not a Broker Desk
Headquartered in Xi'an, Shaanxi Province, Torzi Biotech commands direct access to the rich botanical reserve of the Qinling Mountain corridor. Operating across an SGS-audited 12,447 m² industrial facility, our production capability guarantees complete batch accountability from raw botanical sorting to your factory floor.
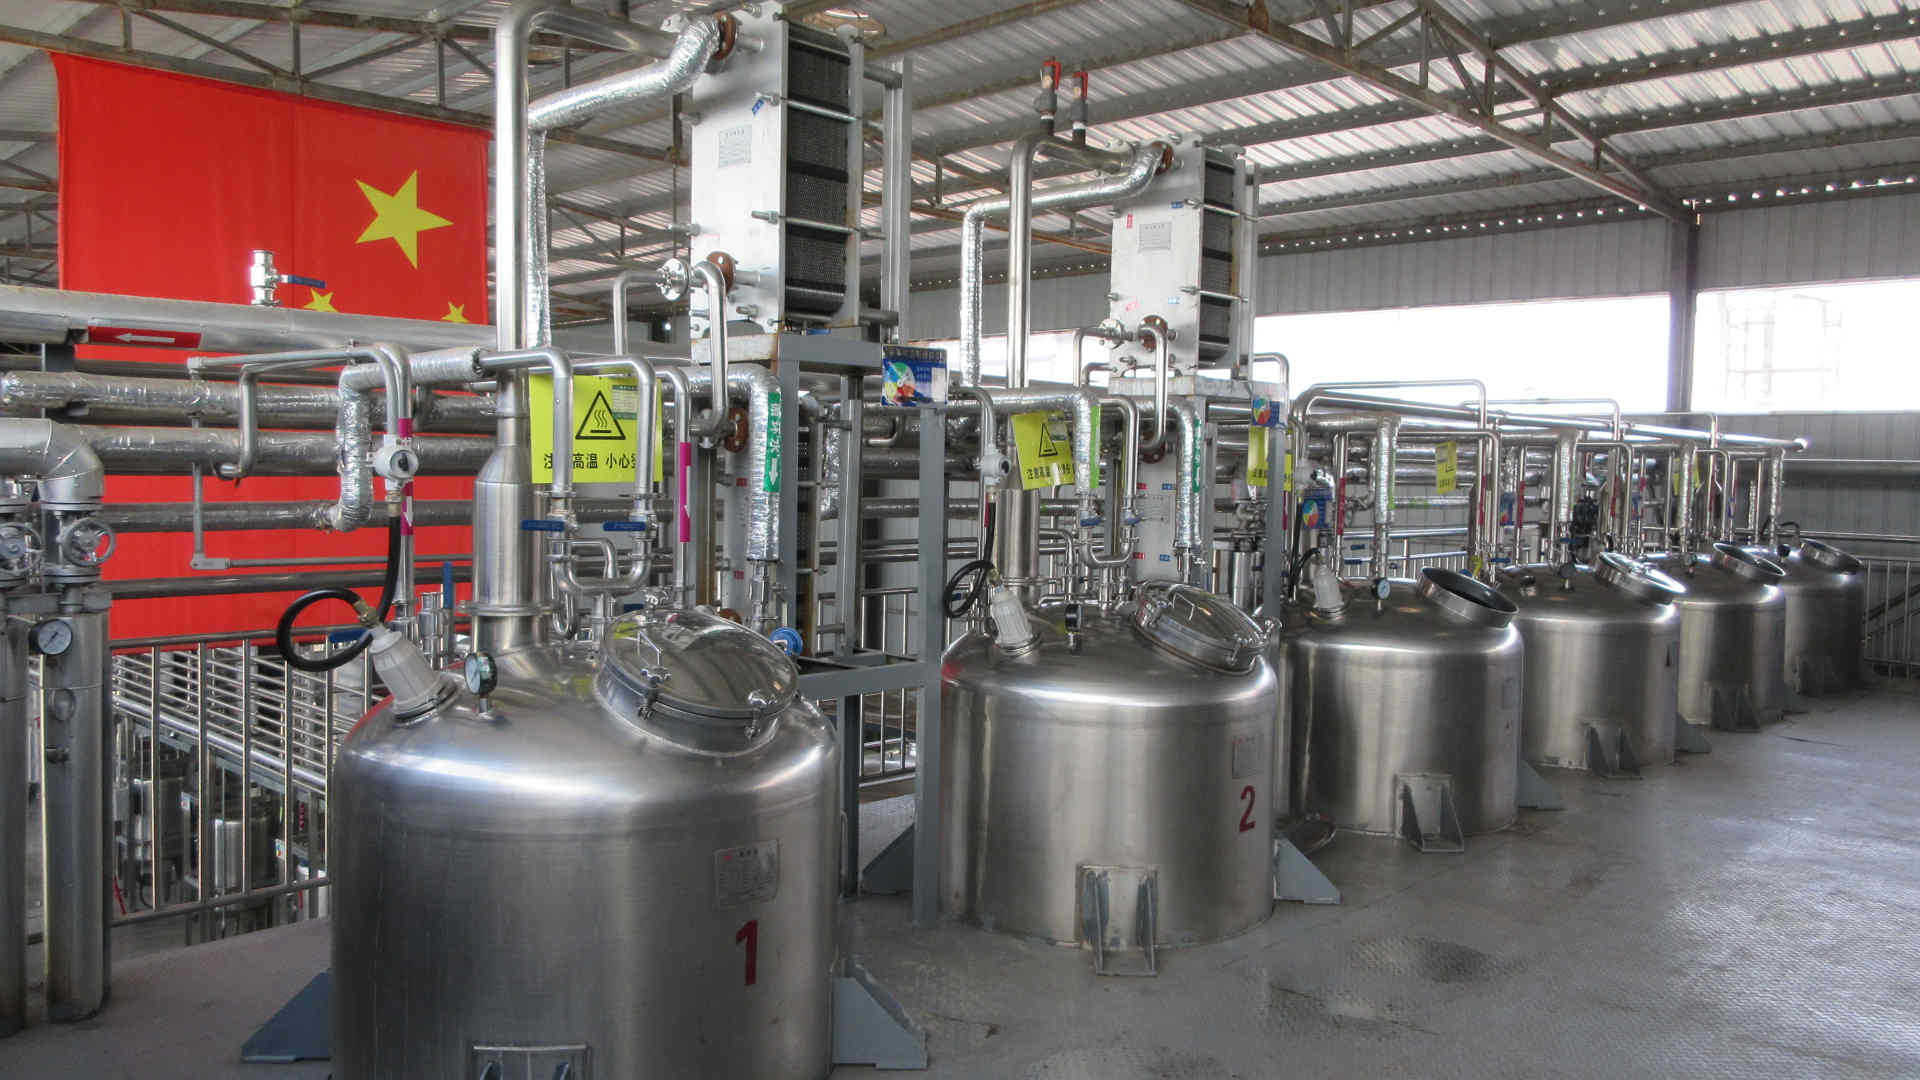
Multi-Stage Solvent & Aqueous Extraction
Our workshop houses multiple 6-cubic-meter food-grade 304/316L stainless steel extraction vessels equipped with ultrasonic transducers, low-temperature vacuum evaporators, and dynamic counter-current circulating systems that optimize active extraction kinetics.
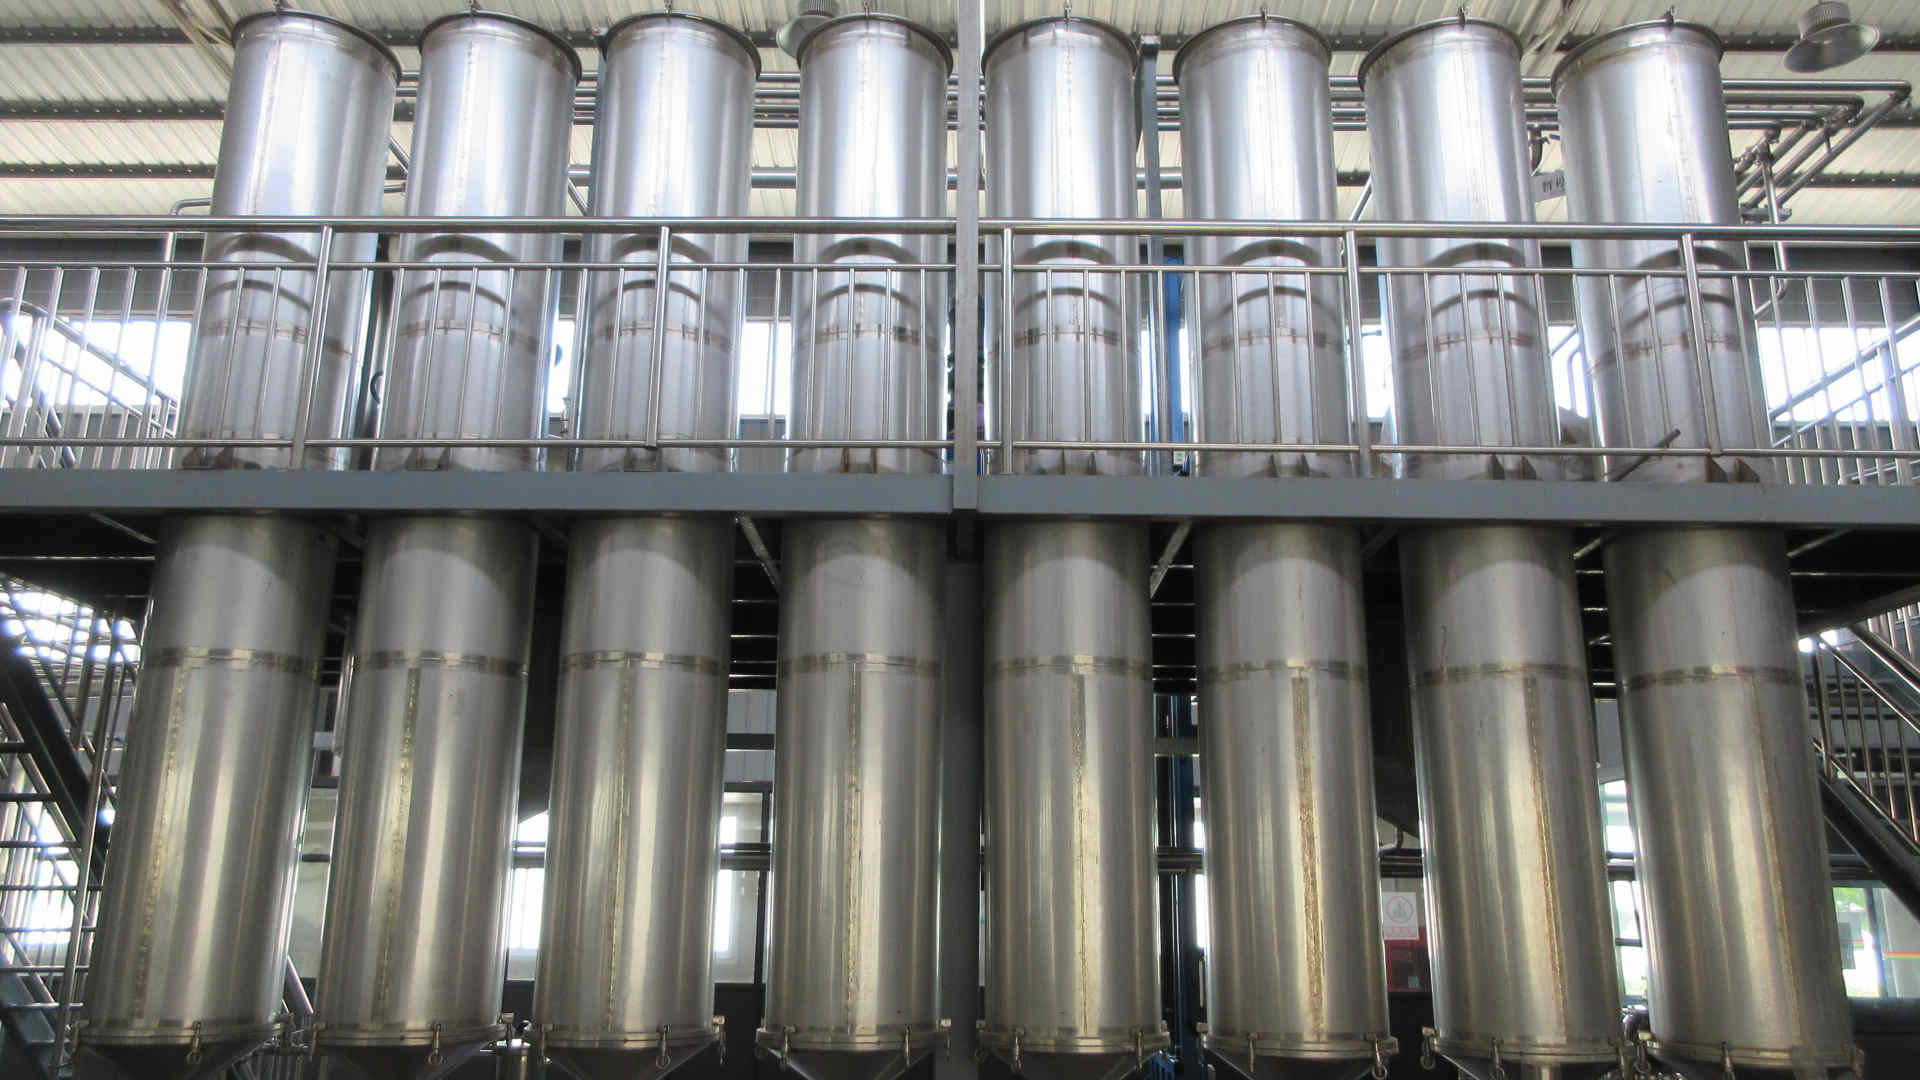
Macroporous Resin Chromatographic Columns
High-precision fractionation towers selectively concentrate target bioactives—such as Sophora japonica flavonoids, steviol glycosides, or saw palmetto phytosterols—while stripping unwanted lipids, tannins, and pesticide traces down to undetectable limits.
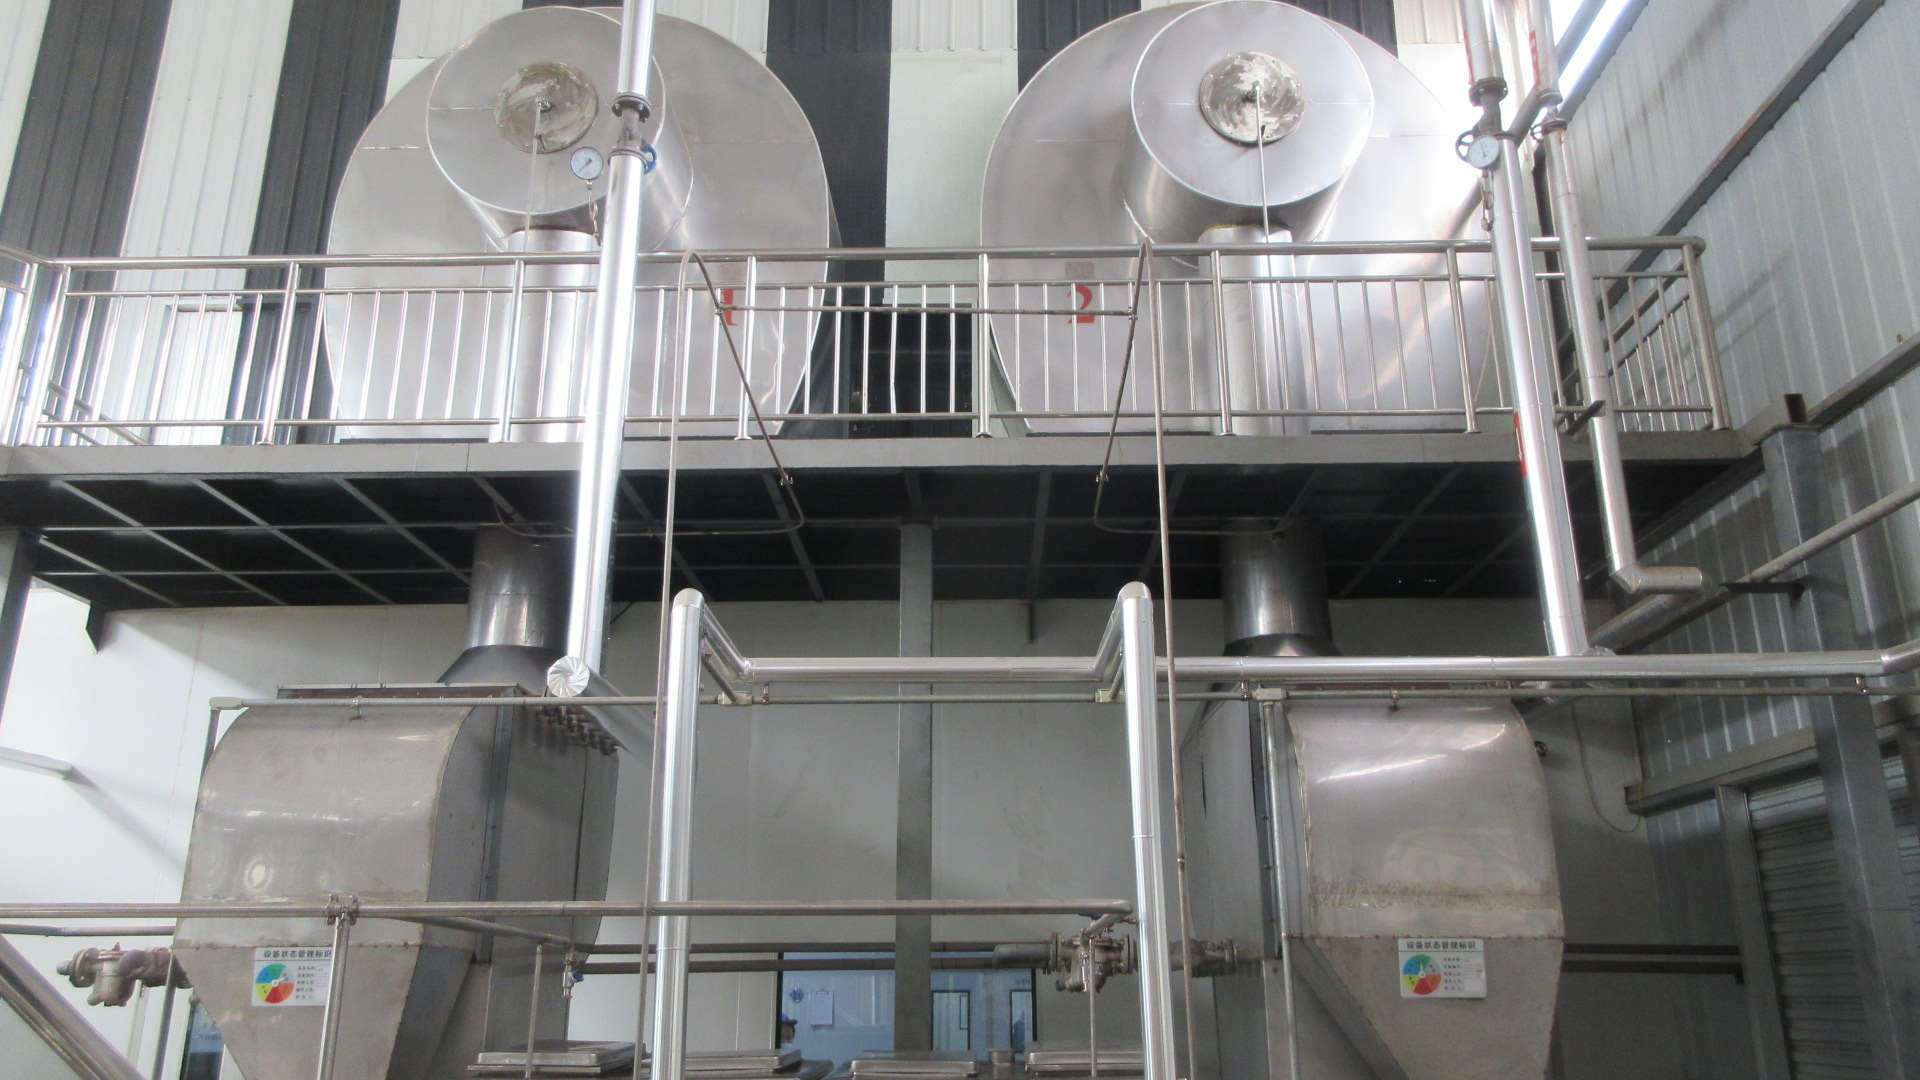
Centrifugal Low-Heat Spray Drying & Agglomeration
Equipped with HEPA-filtered cleanroom air inputs, our high-tower spray drying unit prevents active degradation from thermal exposure, ensuring optimal particle fluidity, density, and immediate solubility for instant beverage powder blends.
In-House Physical & Analytical Testing Laboratory
Every single production batch processed at Torzi Biotech is retained and systematically assayed across our in-house testing complex. We do not rely on generic third-party certificates of analysis without primary batch verification. Our QA/QC laboratory is outfitted with:
- Dual HPLC Systems (High-Performance Liquid Chromatography): Paired with photodiode array (PDA) detectors for definitive fingerprint identification and monomer assay quantification against USP reference standards.
- Gas Chromatography (GC-FID/MS): Dedicated to quantifying volatile terpenes, fatty acid profiles, and monitoring residual solvent limits per USP <467> and EP guidelines.
- Atomic Absorption & Atomic Fluorescence Spectrometry (AAS & AFS): Strict heavy metal detection (Lead, Arsenic, Cadmium, Mercury) calibrated to meet the most stringent California Proposition 65 limits.
- Class 100,000 Cleanroom Microbiology Suite: Real-time pathogen monitoring (Total Aerobic Plate Count, Yeasts & Molds, Salmonella, E. Coli, Staphylococcus aureus).
Beyond raw powder supply, we provide custom OEM/ODM contract solutions starting from 500 units, offering custom hard-gel capsules, stick packs, liquid sachets, and specialized multi-ingredient premixes engineered for swift commercial launch.
Frequently Asked Questions for B2B Importers & Formulators
Essential technical insights covering Minimum Order Quantities (MOQ), third-party lab verification, export compliance documents, and custom formulation options.
For trial orders, pilot formulations, and R&D sampling, our standard MOQ starts from just 1 kg to 5 kg for catalog powders such as Organic Banana, Lion's Mane, and Stevia Extract. Standard commercial production runs ship in 25 kg fiber drums with dual polyethylene food-grade protective liners.
Yes. In addition to our factory batch COA, we routinely collaborate with ISO 17025 accredited international testing bodies, including SGS, Eurofins, and Intertek. We provide blind test reports covering pesticide multi-residue panels (USP <561> 500+ compounds), heavy metal limits, and irradiated residue screenings on request.
Absolutely. Extracts with naturally high lipid contents (e.g., Saw Palmetto 45-85% fatty acids, Beta-Carotene, or Coenzyme Q10) can be processed through our micro-encapsulation and cyclodextrin inclusion technologies. This creates free-flowing, completely water-dispersible powders ideal for functional drinks and effervescent mixes.
Every overseas container and air-freight consignment includes a comprehensive compliance dossier: Batch Certificate of Analysis (COA), Safety Data Sheet (SDS/MSDS), Technical Data Sheet (TDS), Certificate of Origin (Form A, Form E, or RCEP), Non-GMO Statement, Allergen Declaration, and certified Kosher/Halal documents.
We implement controlled agricultural sourcing contracts, strict harvest calendar parameters, and computerized homogenizers capable of mixing single 2,000 kg master batches. Colorimetric delta-E boundaries and spectrophotometric assays guarantee that your final product consistency remains uniform year after year.
For private-label capsule runs (vegetarian, gelatin, or delayed-release), our typical lead time is 10 to 18 business days from packaging artwork sign-off. Bulk ingredient shipments from standing warehouse inventory are dispatched within 48 to 72 hours via air express or temperature-controlled sea freight.
Partner with a Verified Botanical Extract Manufacturer
Whether you are developing a new functional beverage, looking to reduce production costs on high-purity stevia or fruit powders, or qualifying an audited secondary source, our technical applications engineering team is standing by.
Inquire Now