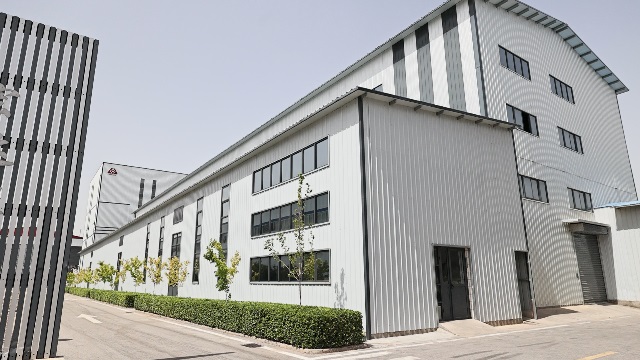
Global Botanical Extraction & Private Label Manufacturing Partner
Shaanxi Torzi Biotech Co., Ltd. is an established custom manufacturer and specialized exporter based in Xi'an, Shaanxi, China. Backed by 23+ years of extraction mastery and 17 years of direct overseas export experience, we deliver end-to-end solutions from pure botanical sourcing to finished private-label dietary supplements.
Our integrated facility covers 12,447 square meters, equipped with multi-stage dynamic extraction tanks, vacuum concentrators, multi-tier resin adsorption systems, high-efficiency spray drying towers, and continuous cleanrooms. Every manufacturing cycle complies strictly with cGMP, ISO22000, and FSSC22000 management frameworks.
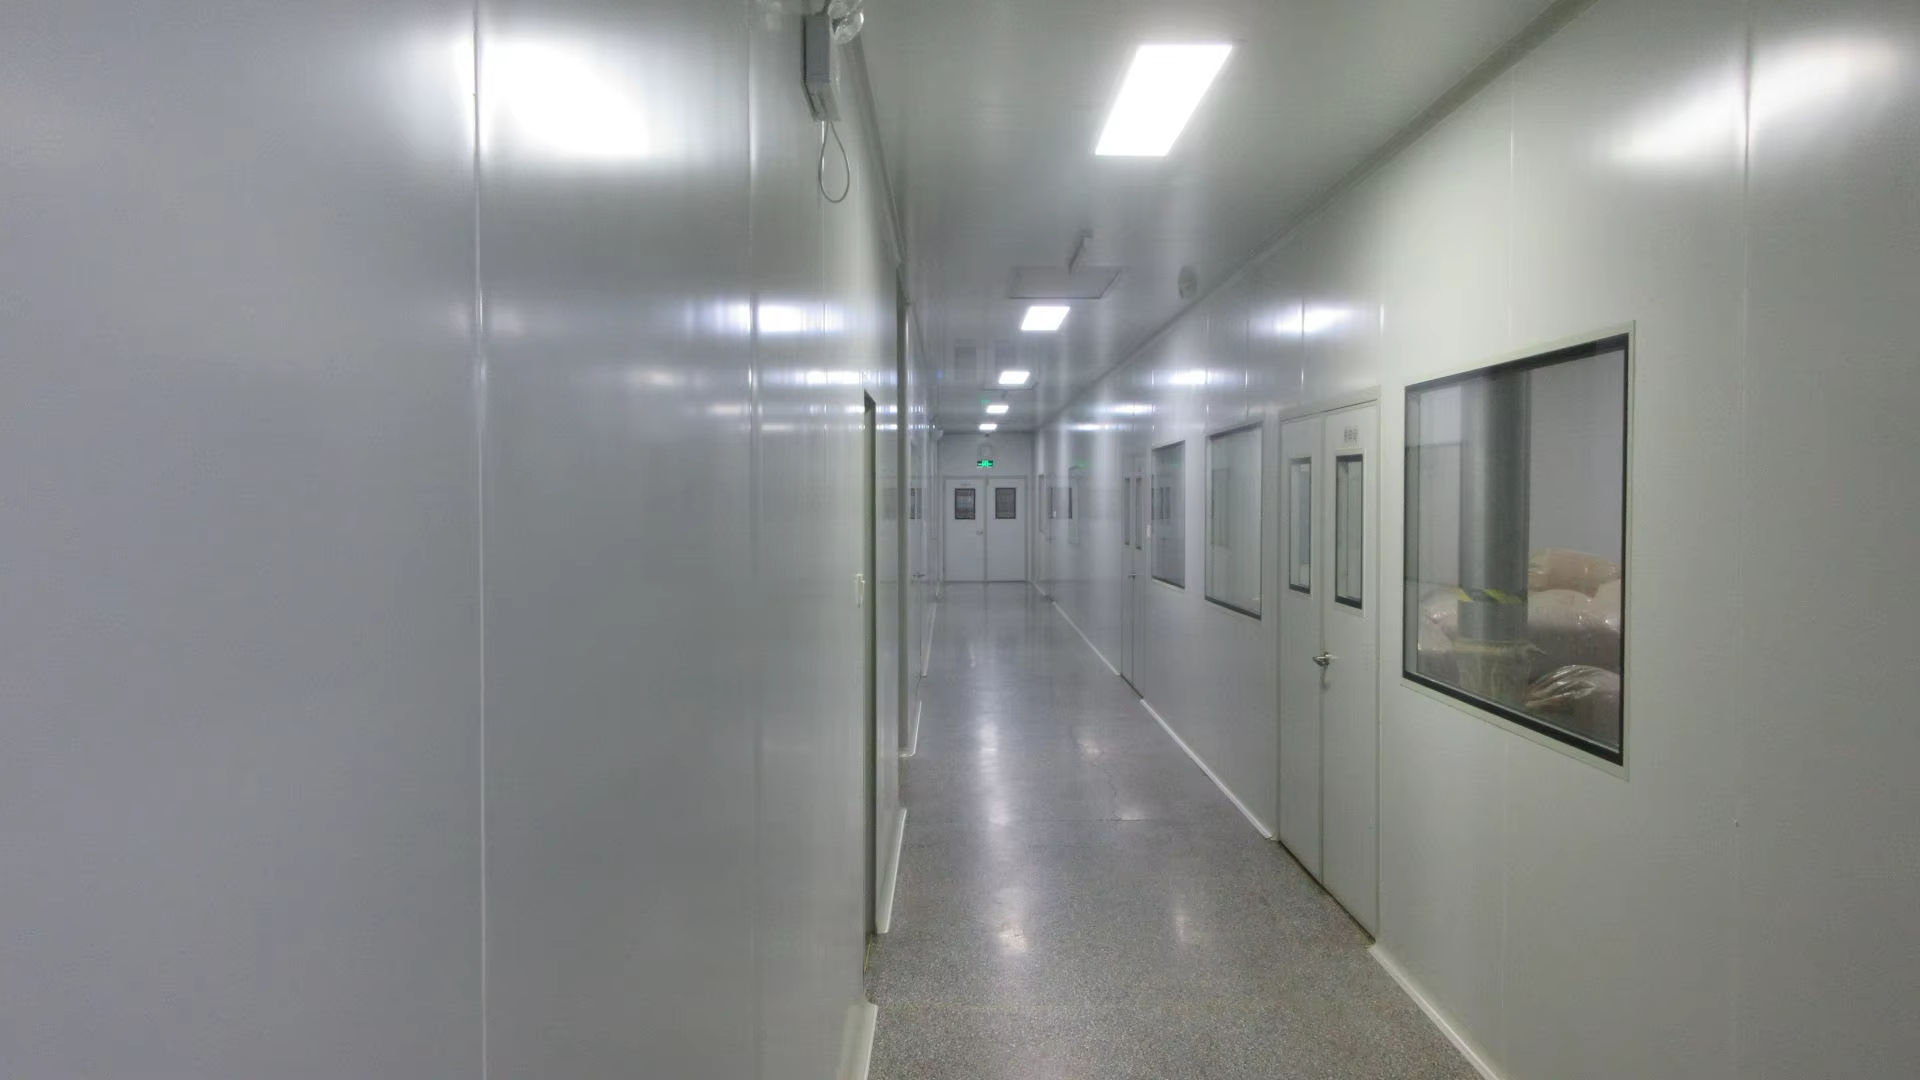 12,447 m² Verified Facility
Verified Supplier Benchmarks & Delivery Track Record
Independent operational data audited and monitored through platform transactions, reflecting superior dispatch performance, client retention, and market feedback.
- Export Standing#3 Leading Manufacturer in Extracts
- Popularity Ranking#6 Most Popular in Plant Extract
- Verified Staff89 Full-Time Personnel
- Online RevenueUS $200,000 − $500,000
Comprehensive Manufacturing & Technical Strengths
From custom active extraction formulas to global logistics compliance, Shaanxi Torzi Biotech Co., Ltd. provides robust manufacturing infrastructure for B2B procurement.
Customization & Formulation
- Formulation CustomizationVerified
- Sample Extraction ProcessingVerified
- Custom Packaging (Pouches/Tubs)Verified
- Drawing/Design Packaging CustomizationVerified
Trade Capacity & Markets
- Years Exporting23 Years
- Nearest Export PortsShanghai, Beijing, Qingdao
- Overseas WarehousingUnited States (US)
- Payment MethodsT/T, L/C, Trade Assurance
Research & Development
- Dedicated R&D Engineers6 Senior Chemists
- New Products Launched Annually5+ Formulations
- Technical Media PackagesAvailable
- Pilot Extraction TestingStandard
Production Infrastructure
- Factory Floor Space12,447 m²
- Production Flow StandardizationVerified
- Continuous Dynamic ExtractionOperational
- Controlled Cleanroom AreasStandard
Quality Assurance & QC
- Full-Time QA/QC Inspectors6 Specialists
- Material Inspection RecordsArchived per Lot
- Finished Product InspectionEvery Batch
- High-Precision Testing DevicesHPLC, GC, AAS, AFS
Specialized Enterprise Services
- Fortune 500 CollaborationAssessed
- Amazon FBA Labeling & PalletizingSupported
- International Trade ExposCPHI, Vitafoods
- One-Stop Contract ManufacturingAvailable
Eight-Stage Standardized Production Workflow
Every extraction, concentration, and pulverization step is rigorously logged, inspected, and cross-checked against internal quality baselines and international pharmacopoeia standards.
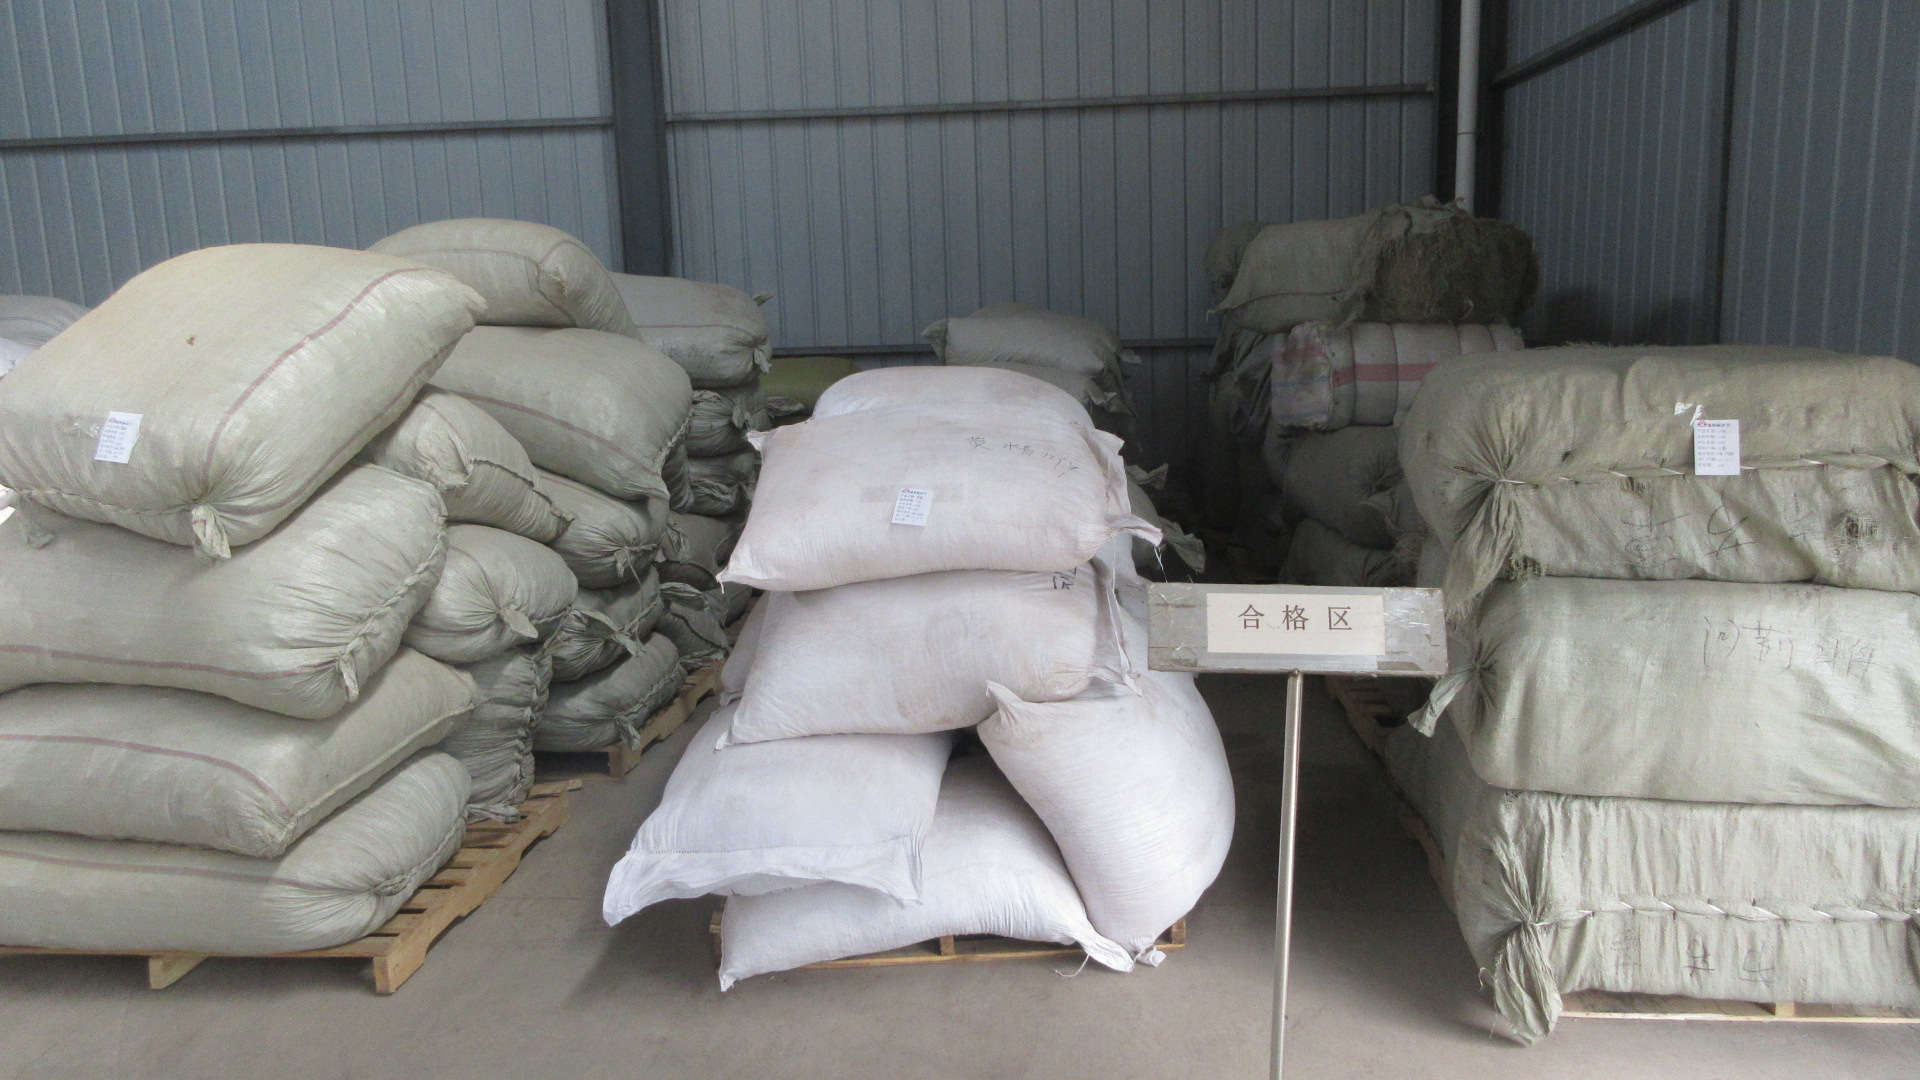
Raw Materials
Botanical identity identification, origin tracing, moisture, and pesticide screening.
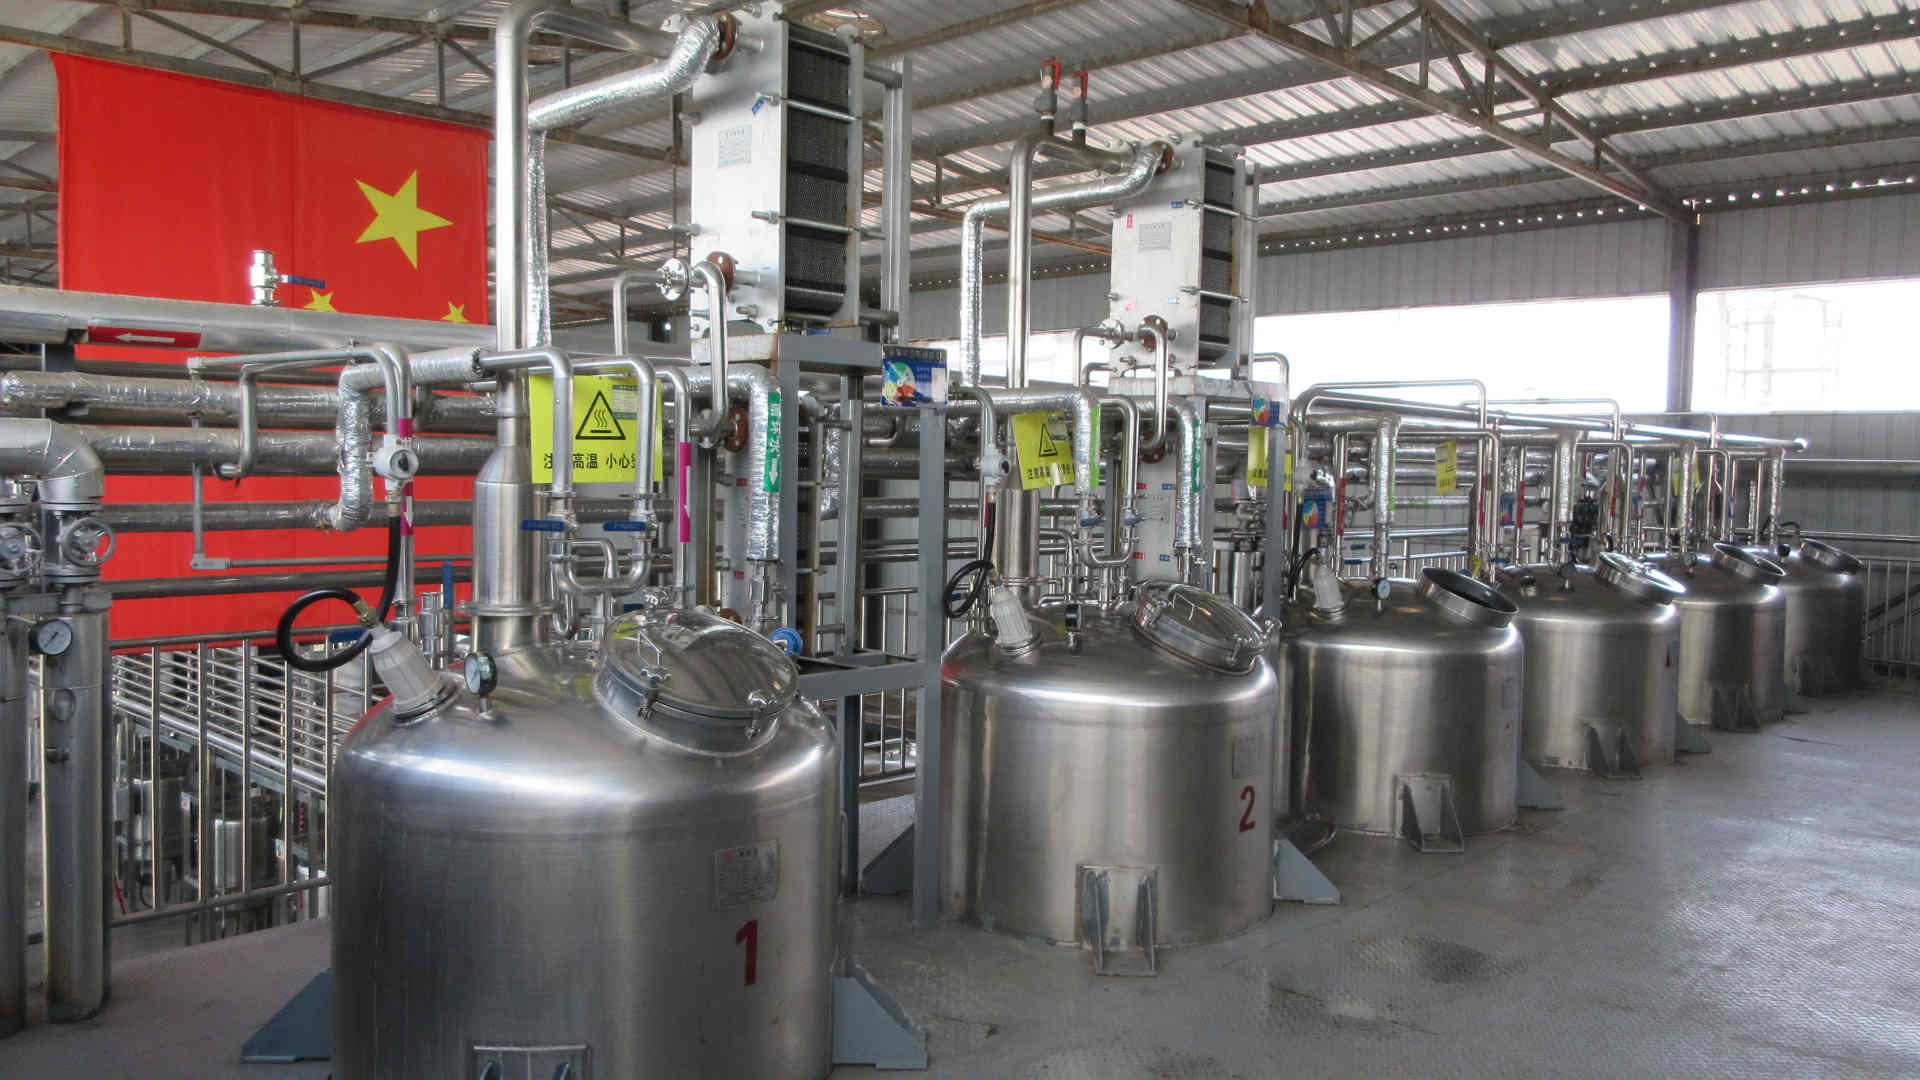
Extraction
Temperature-controlled aqueous or hydroalcoholic dynamic extraction tanks.
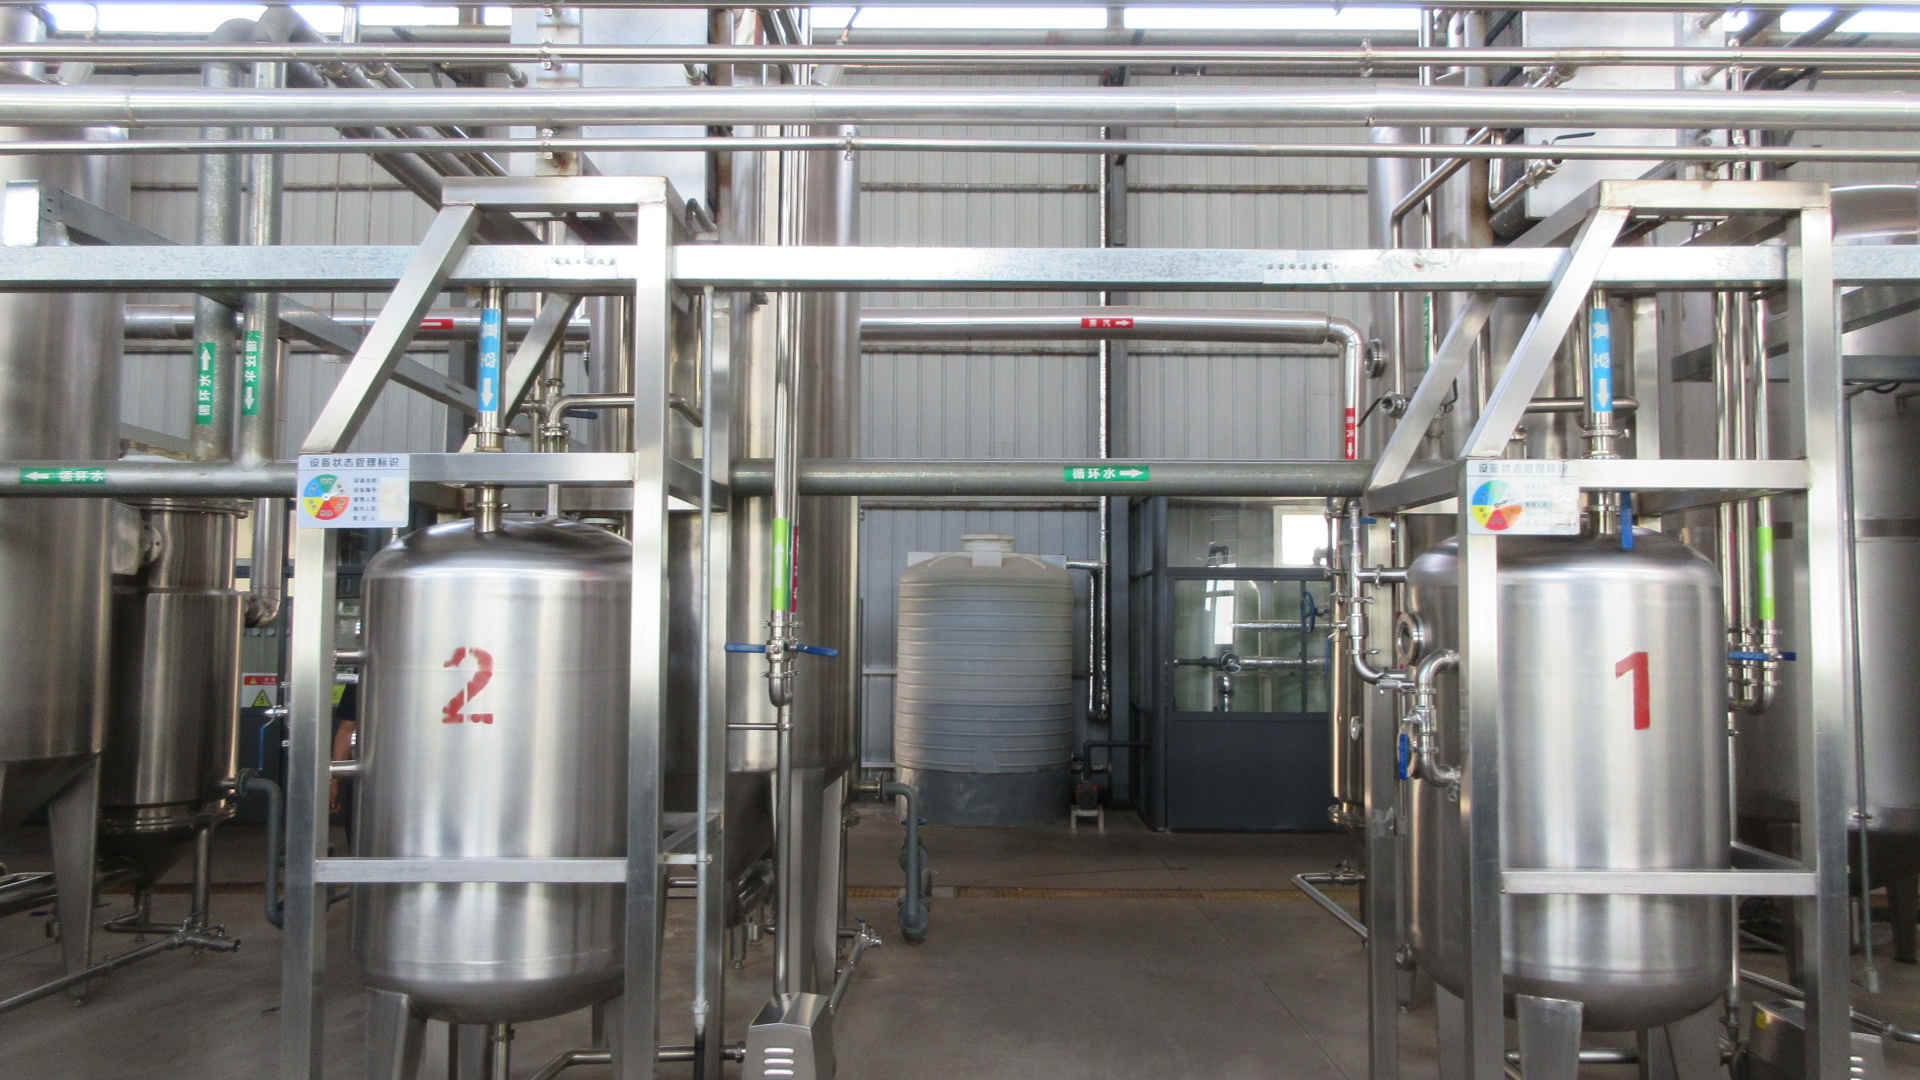
Concentration
Low-temperature vacuum concentration to protect heat-sensitive active compounds.
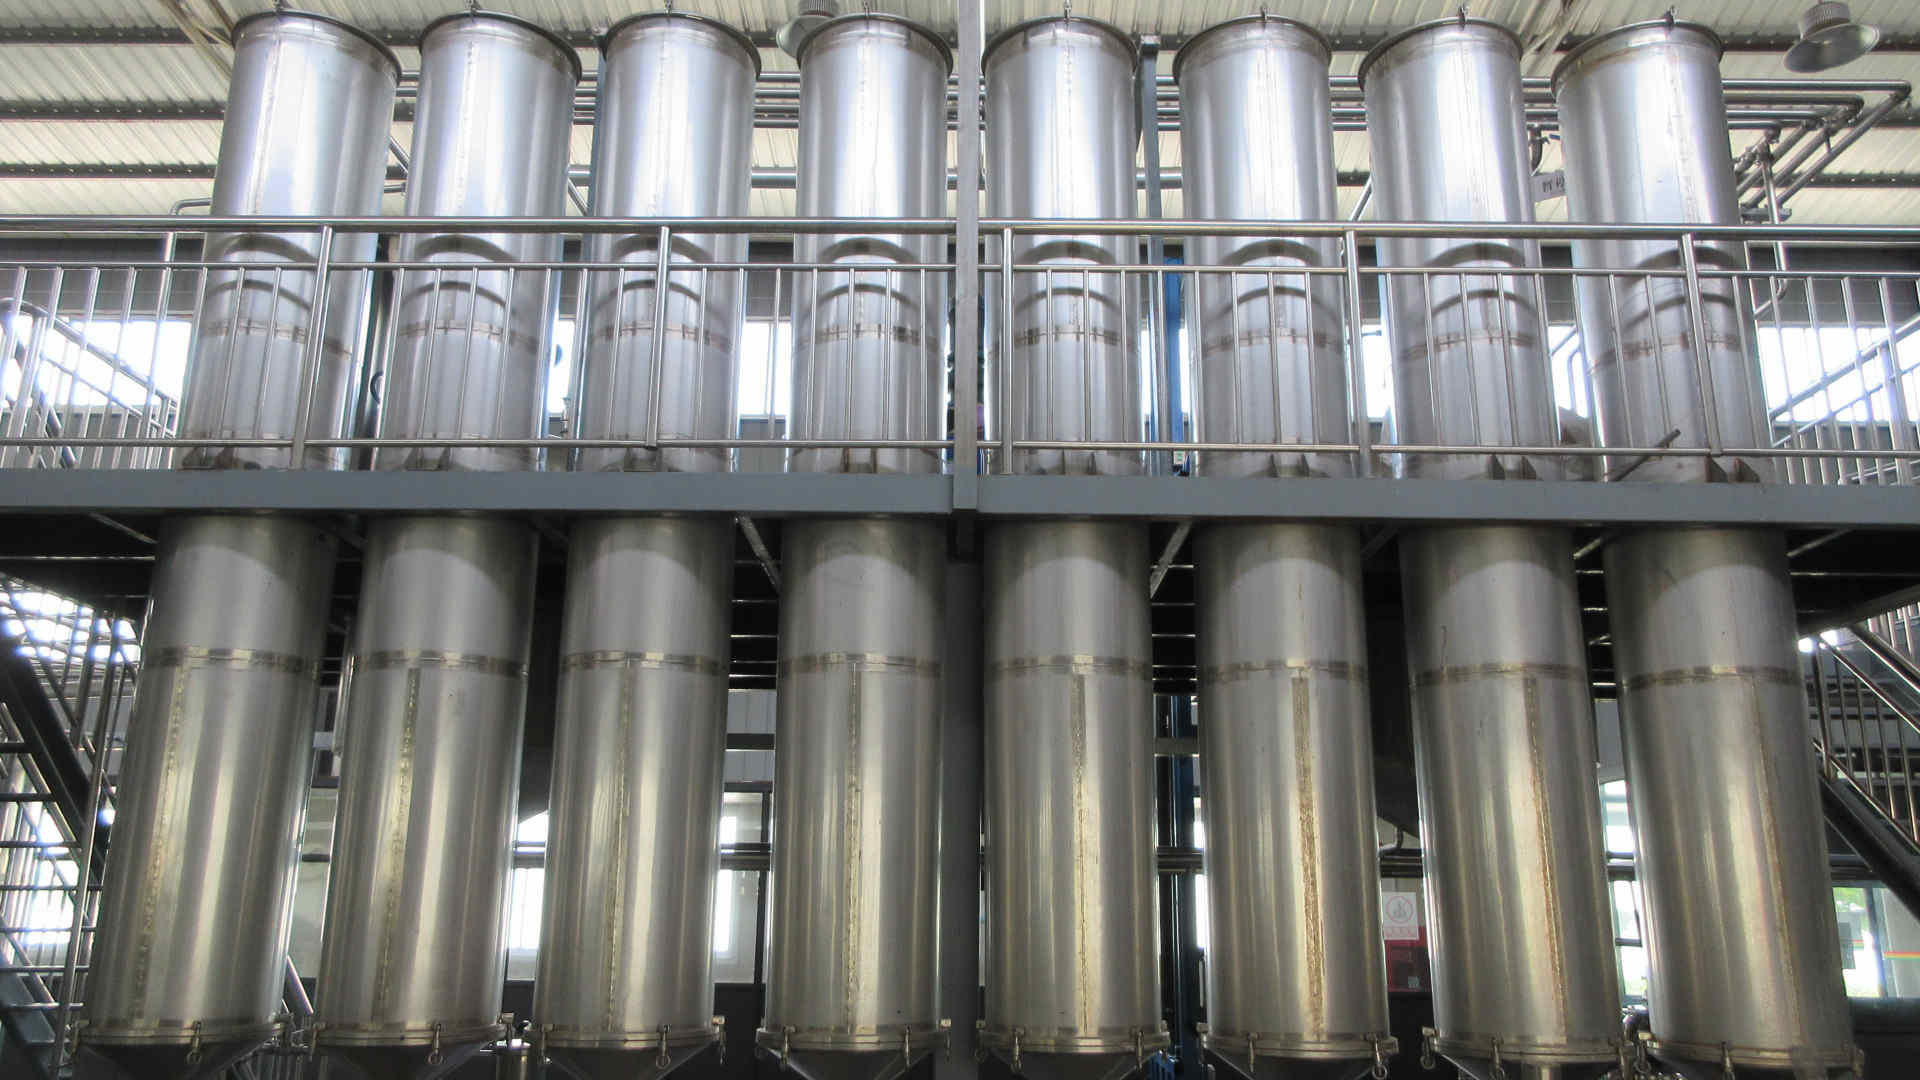
Adsorption
Macroporous resin adsorption chromatography columns for active compound isolation.
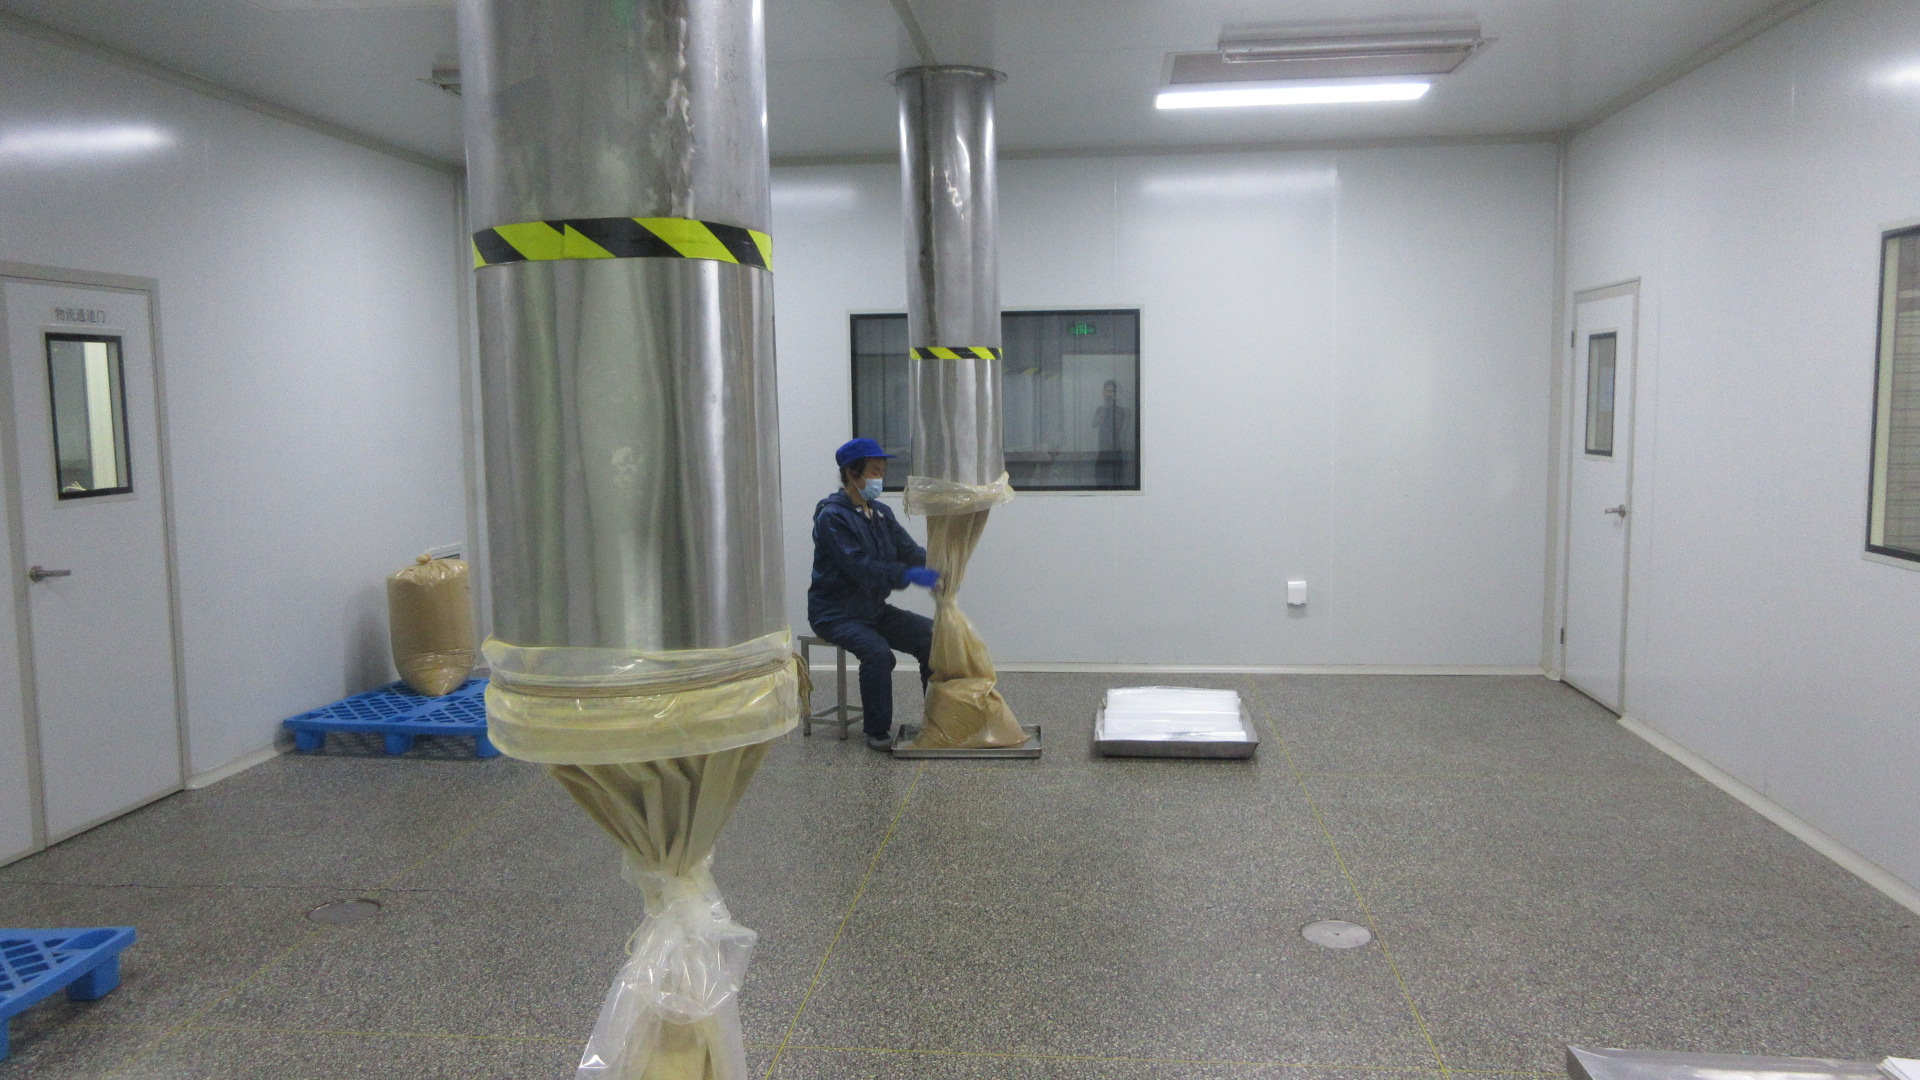
Drying & Spraying
Centrifugal spray drying and sterile vacuum drying for stable, free-flowing powder.
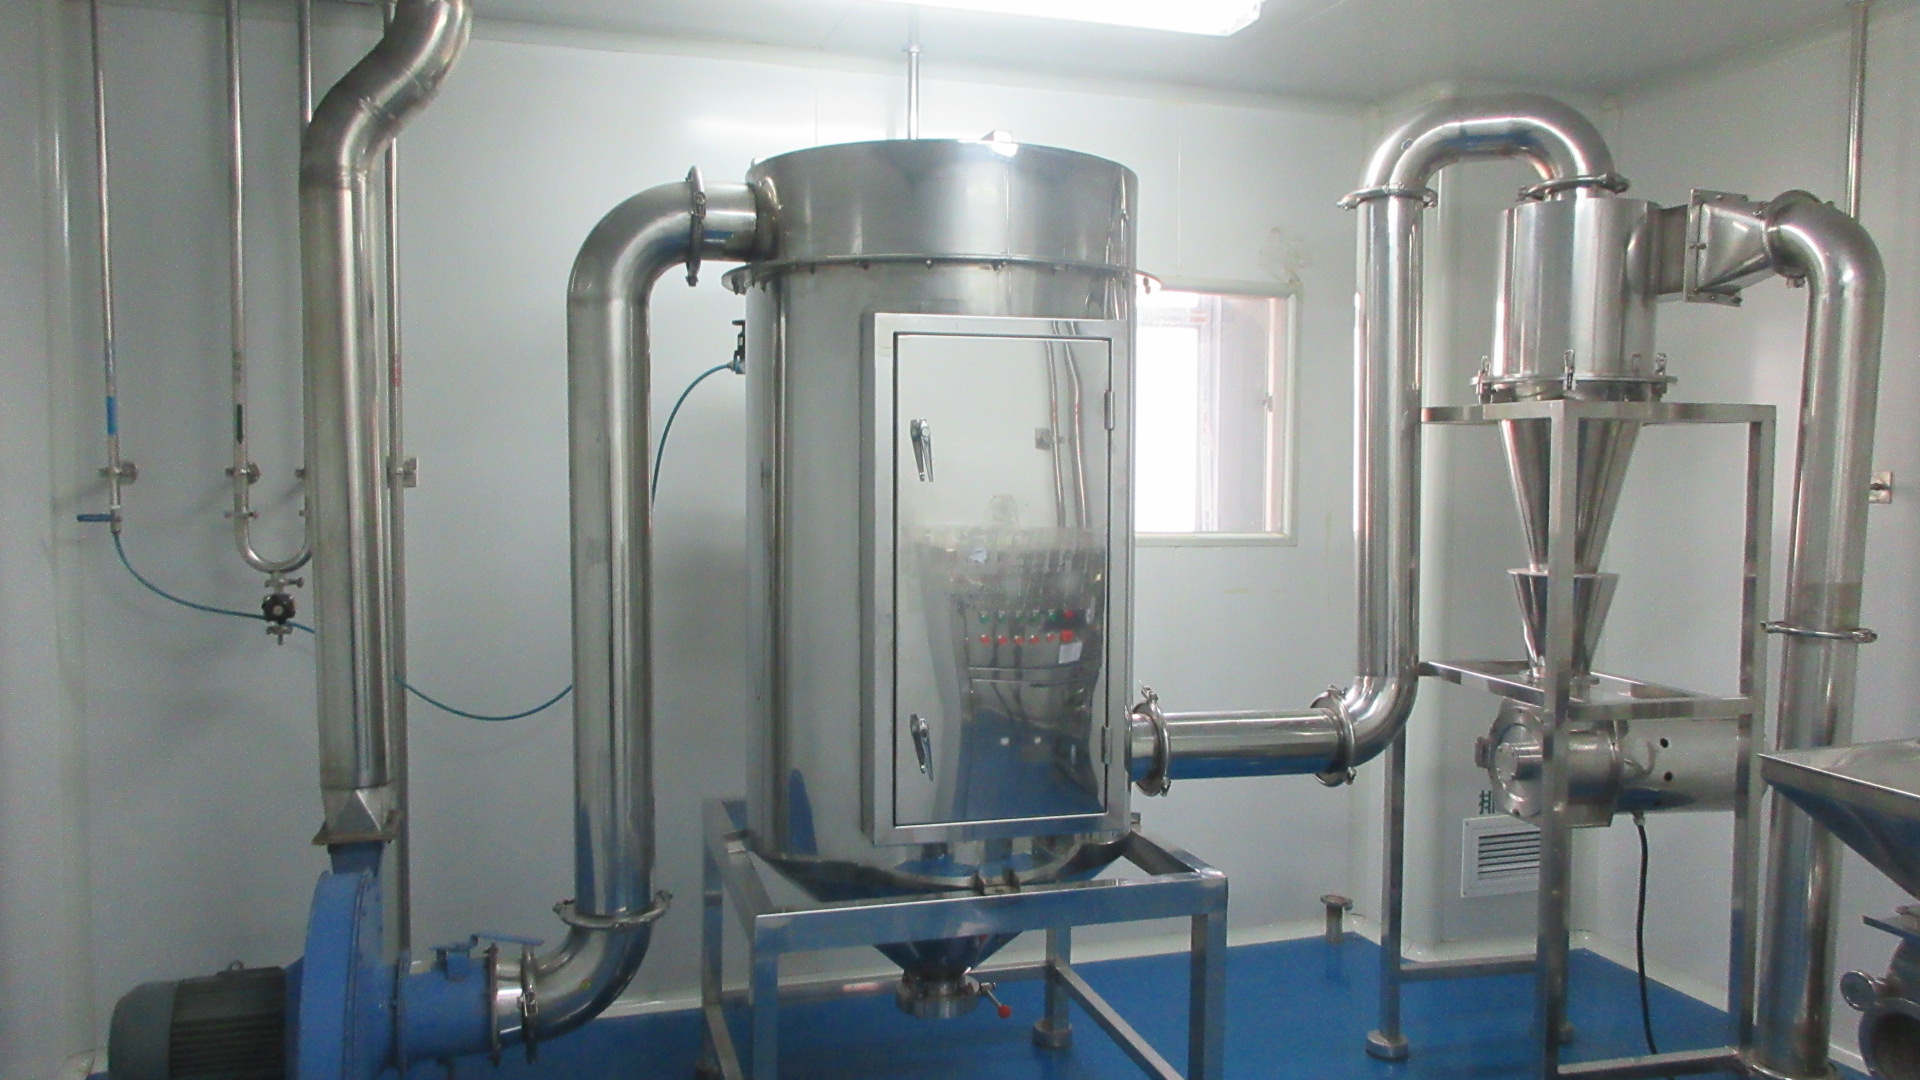
Smashing & Sieving
Controlled micro-pulverization and multi-mesh vibratory sieving (80 to 200 mesh).
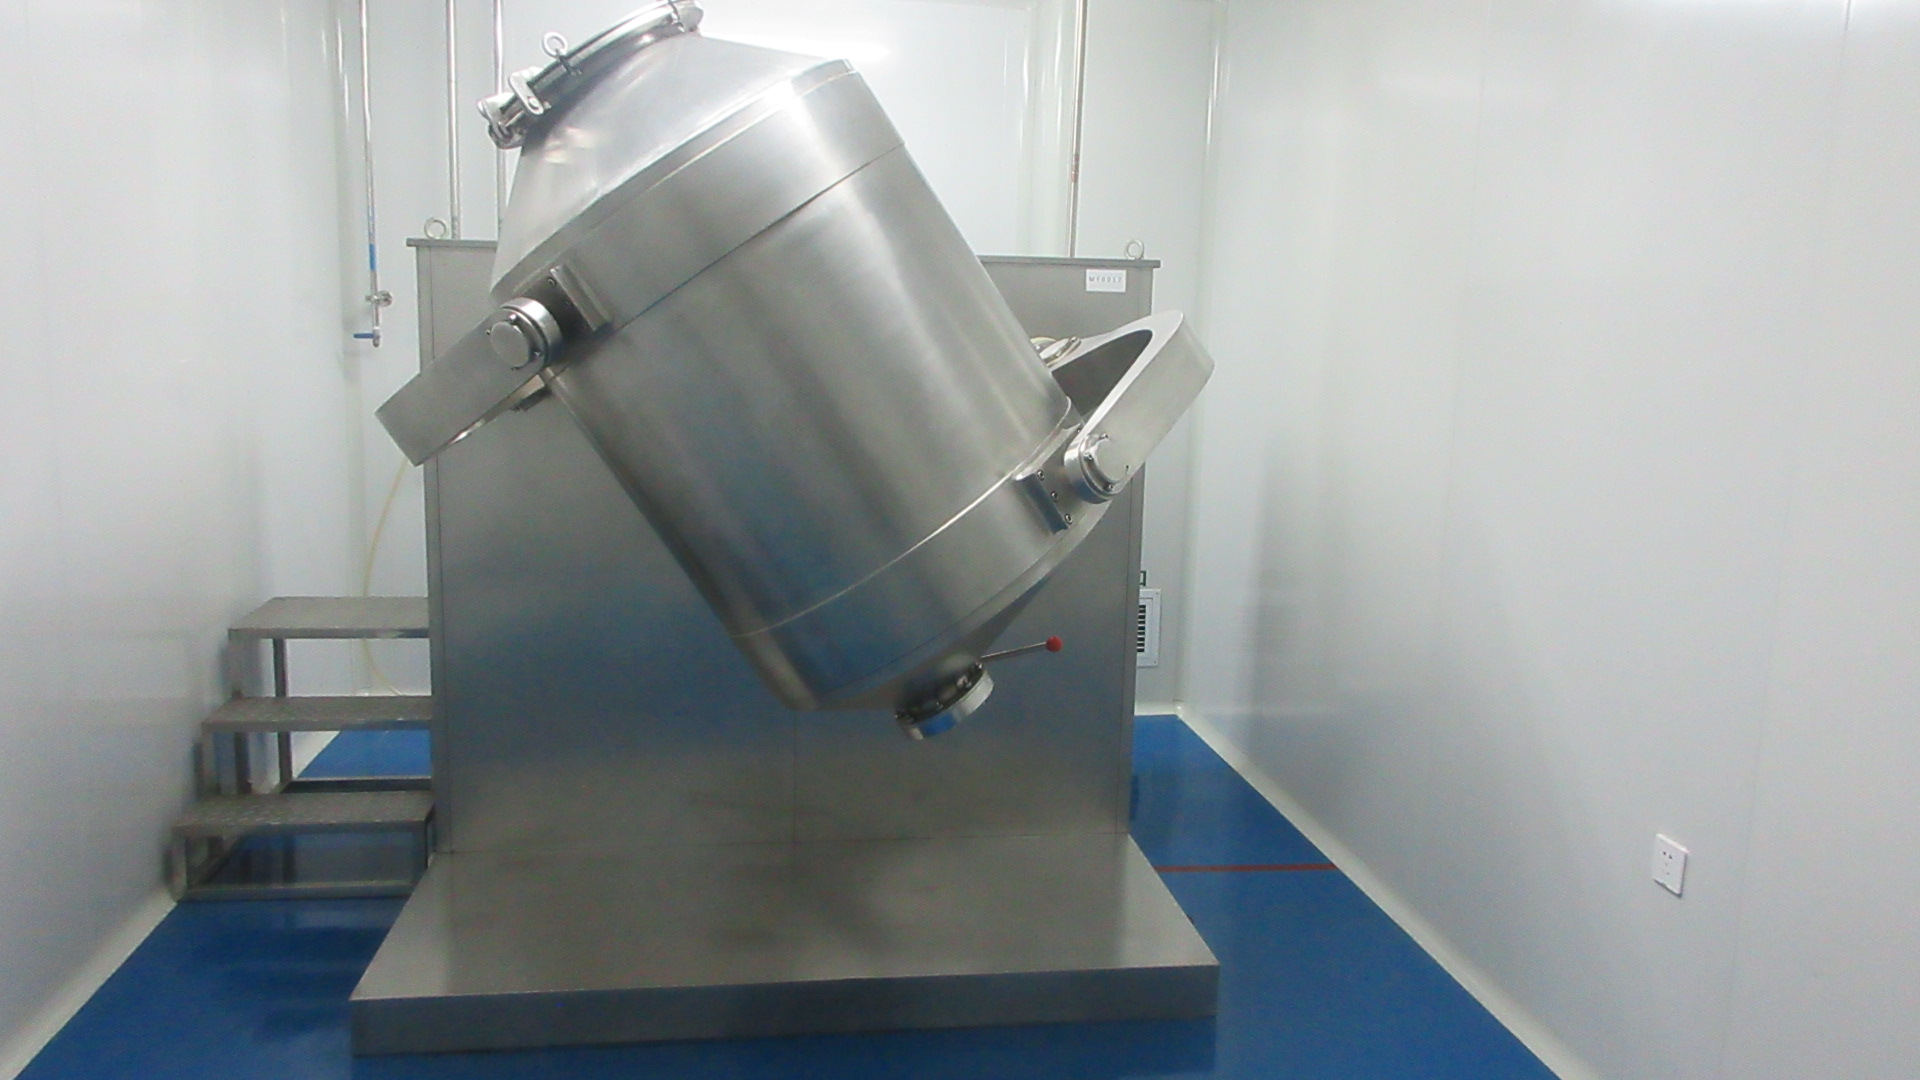
Mixing
Three-dimensional industrial blenders ensuring absolute batch-to-batch homogeneity.
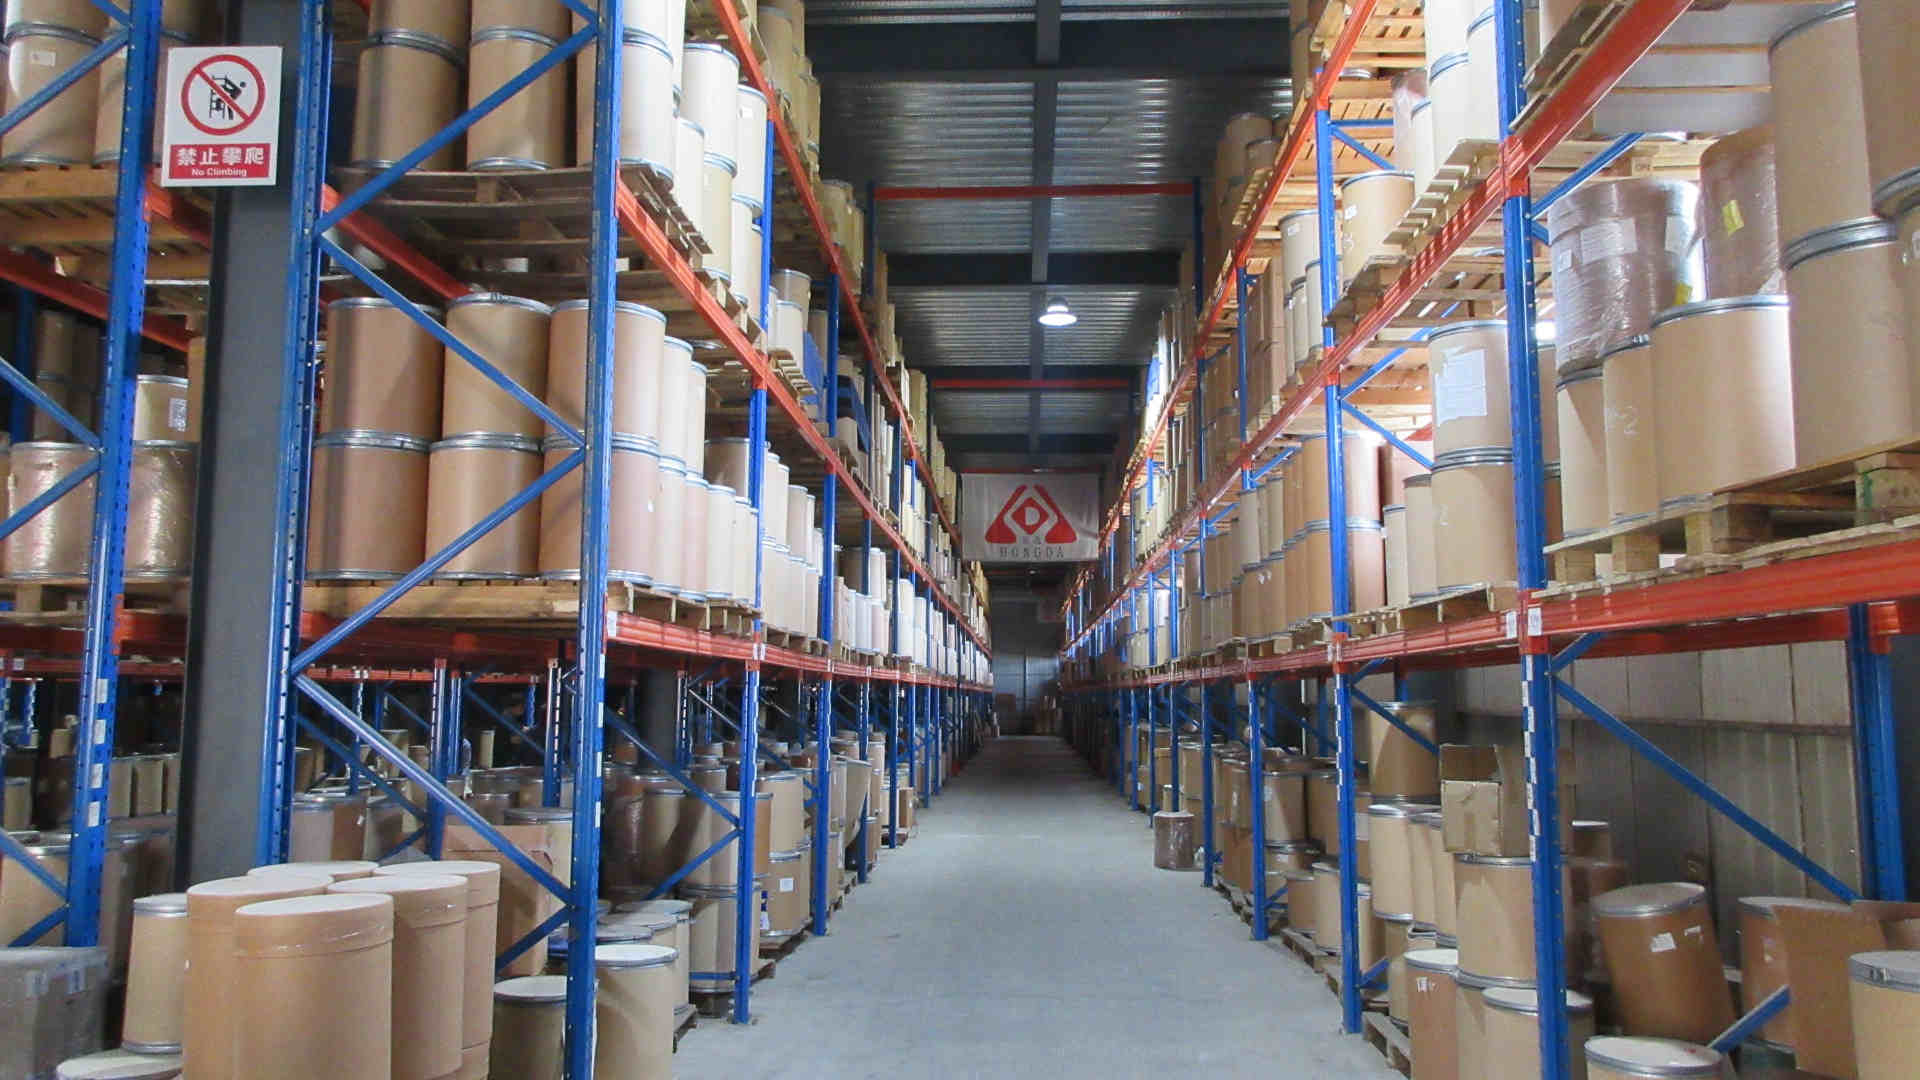
Finished Product
Cleanroom packaging in food-grade foil bags and drums with complete serialization.
Modern Extraction Lines & Precision Analytical Labs
We operate high-volume stainless steel processing hardware complemented by advanced chromatography and spectrometry instruments to assure safety, potency, and compliance.
Workshop Machinery & Processing Systems
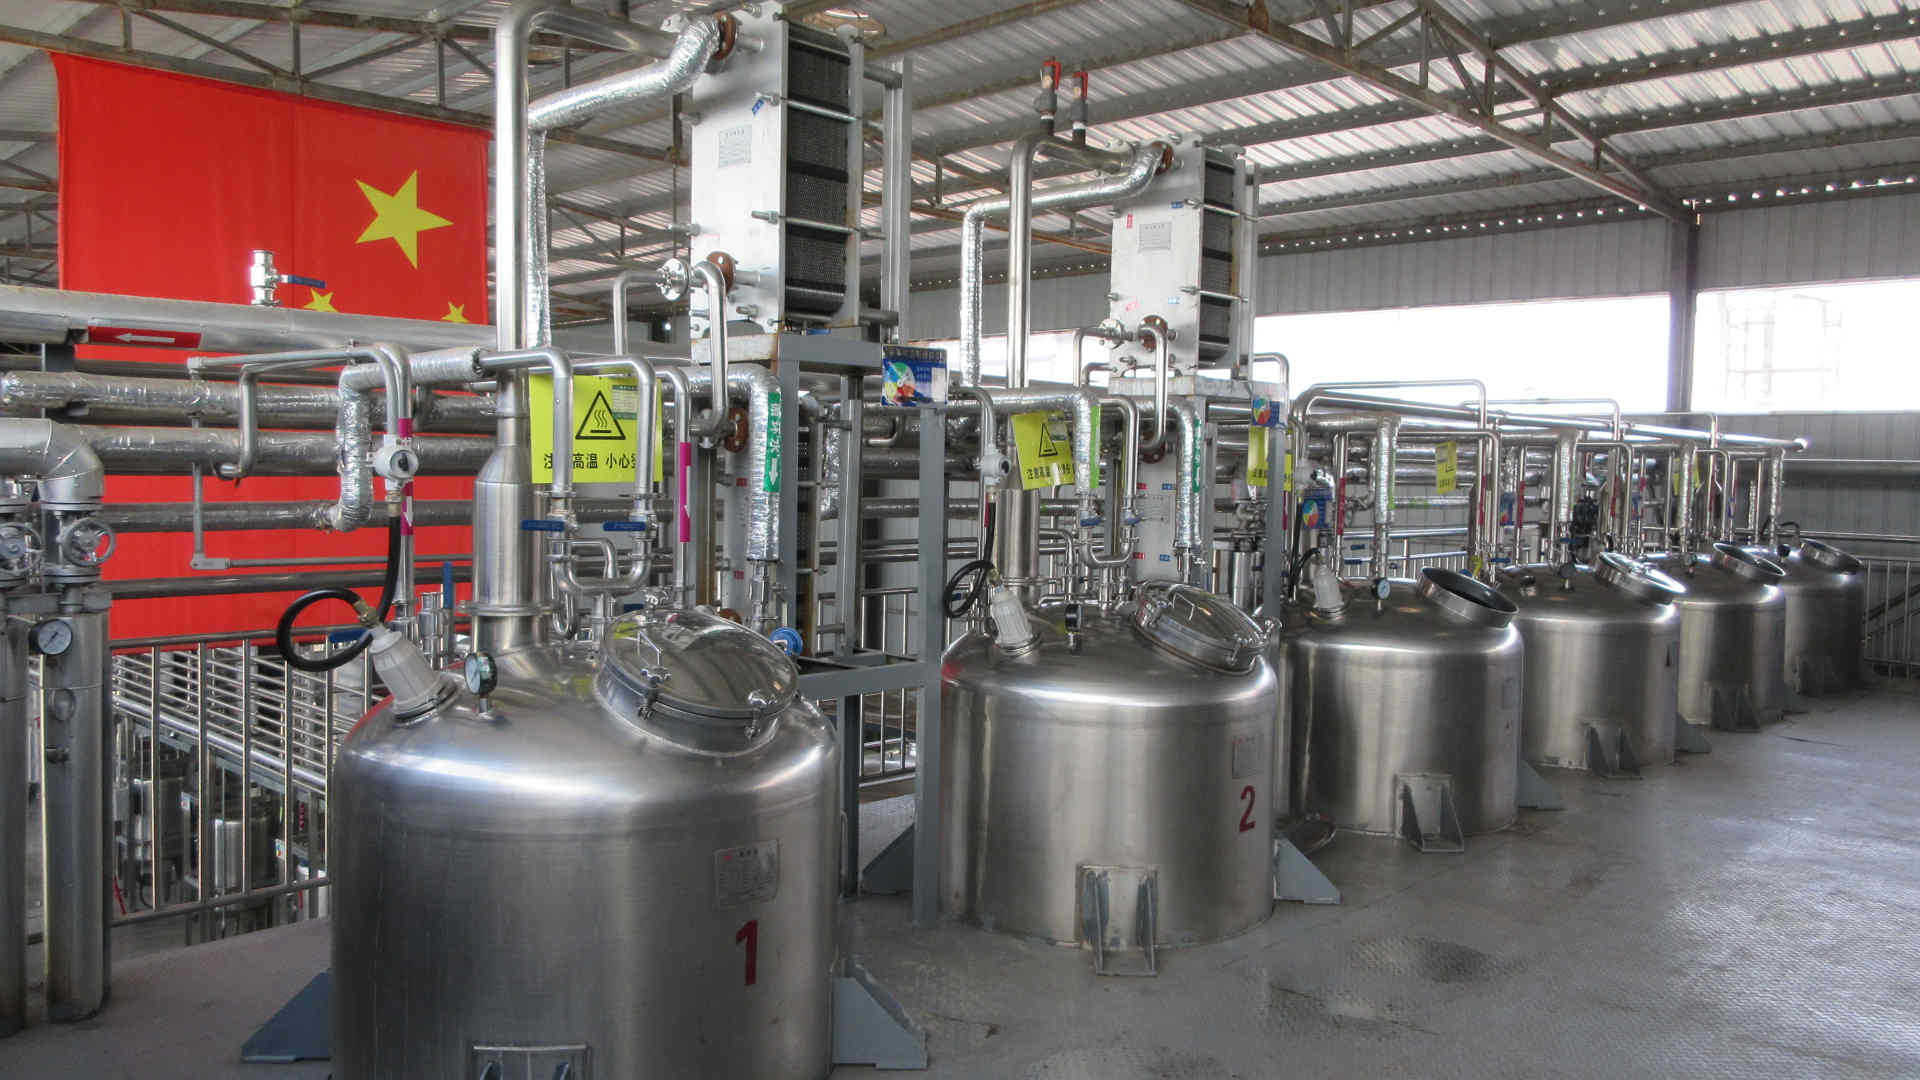
Multi-Function Extract Tank
High-efficiency solvent extraction system for botanical bioactives.
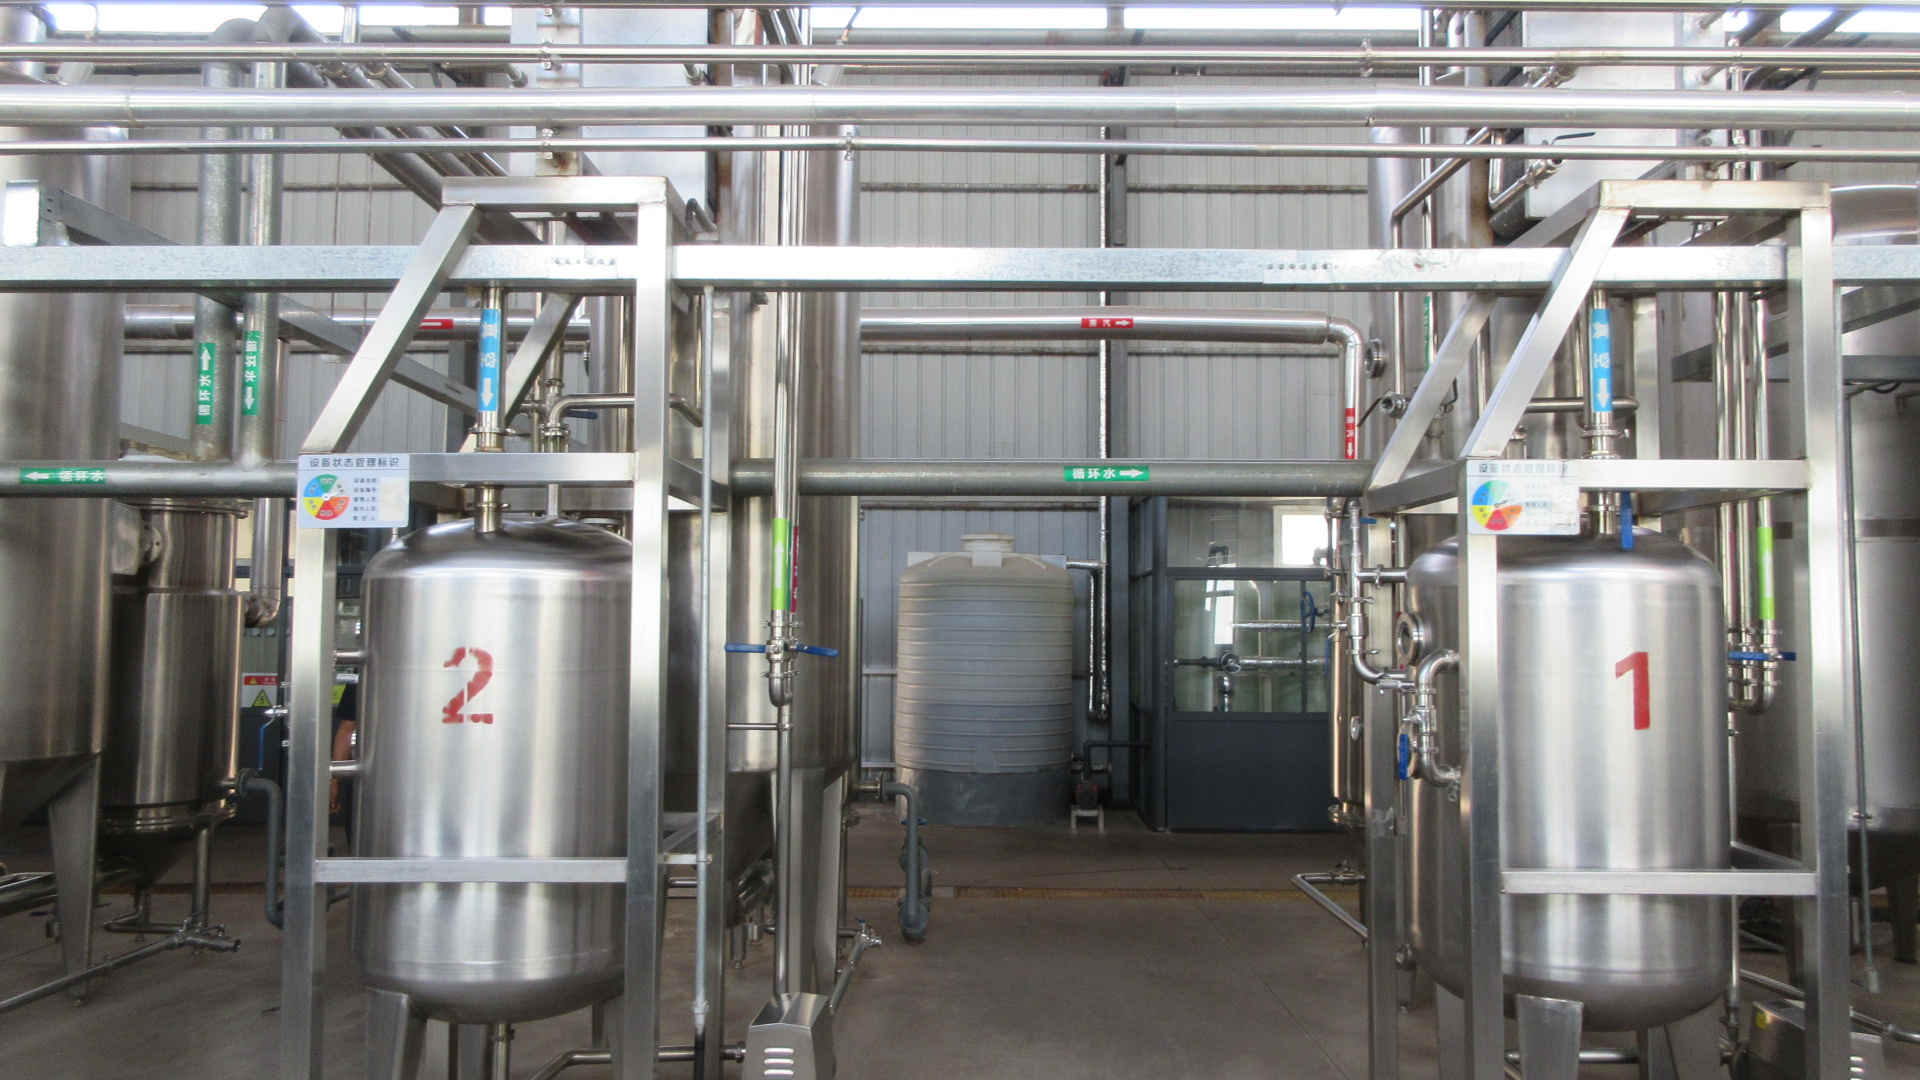
Vacuum Concentrator
Energy-efficient falling film concentration under reduced pressure.
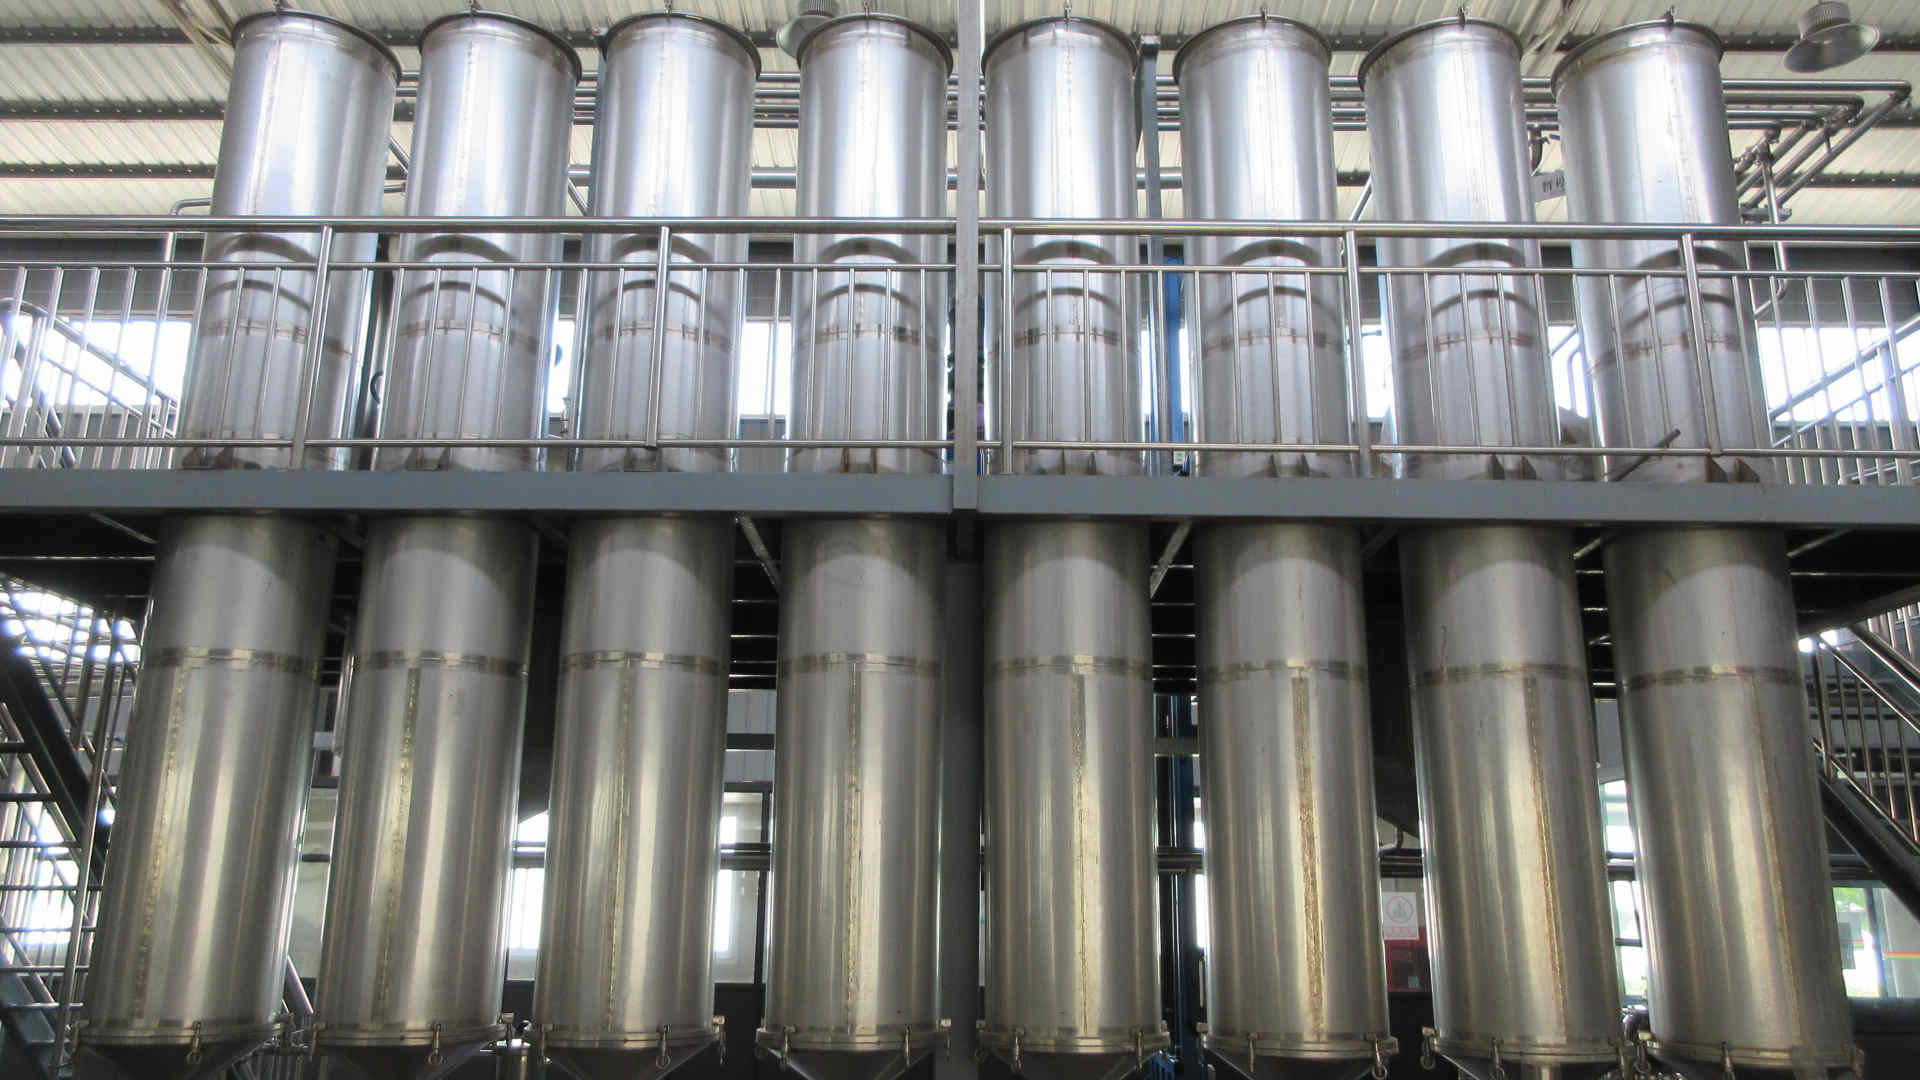
Adsorption Column Equipment
Selective chromatographic separation for high-potency monomer fractions.
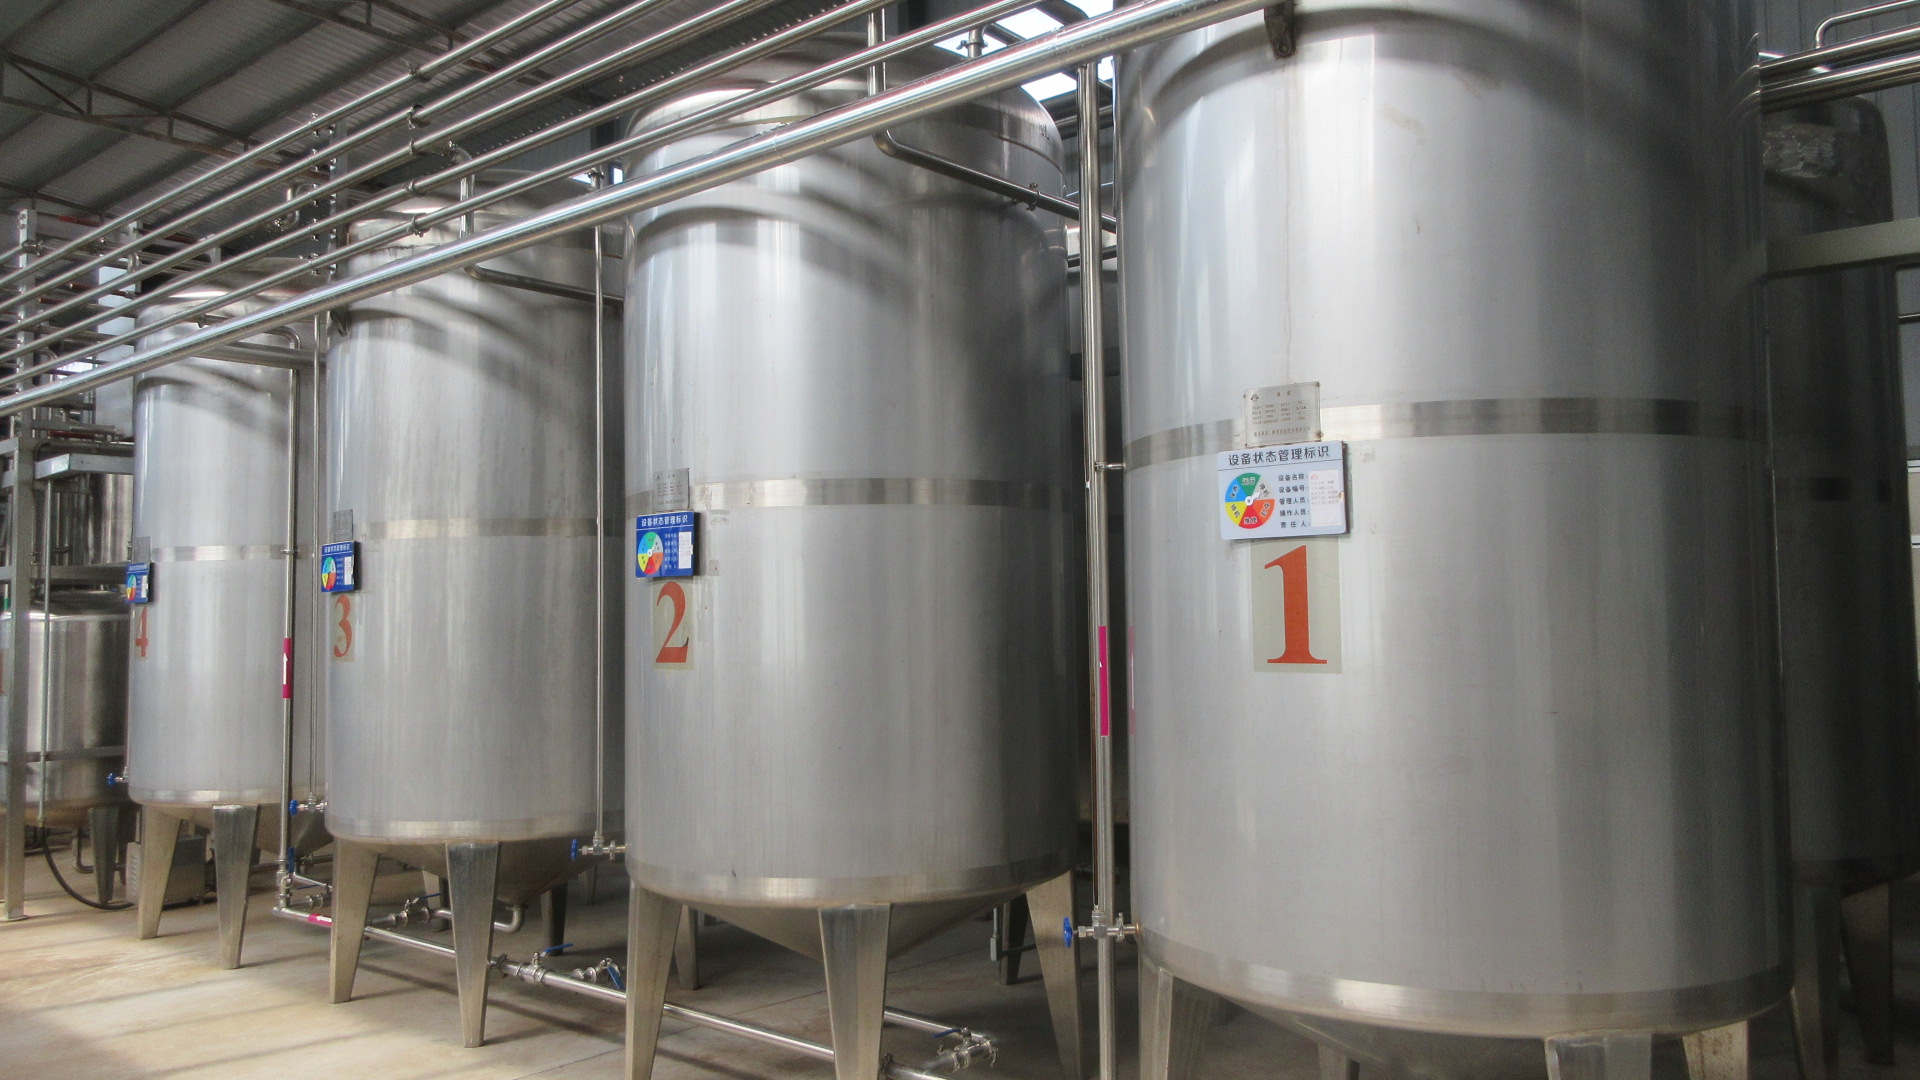
Sanitary Storage Tanks
Food-grade SS304/SS316 storage vessels with CIP automated washing.
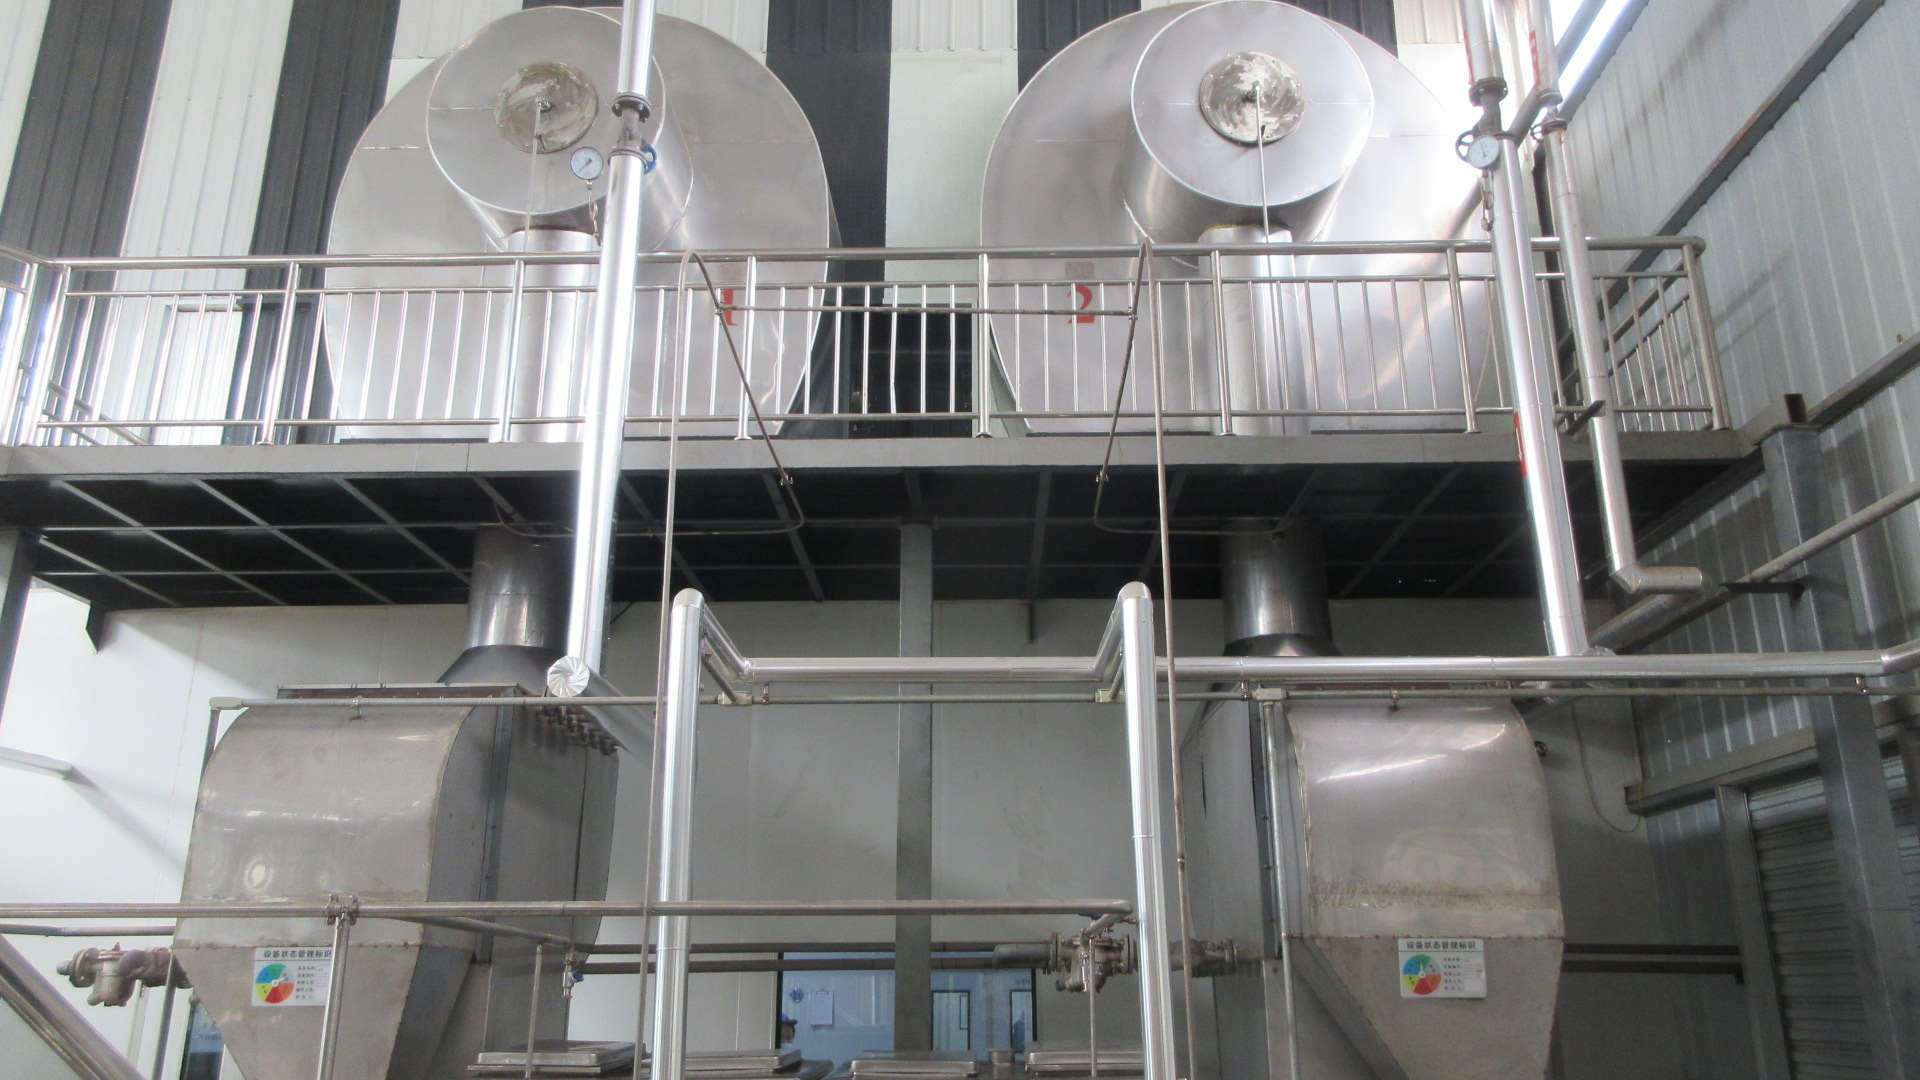
Spray Drying Tower
Instant atomization drying to retain biological activity and particle texture.
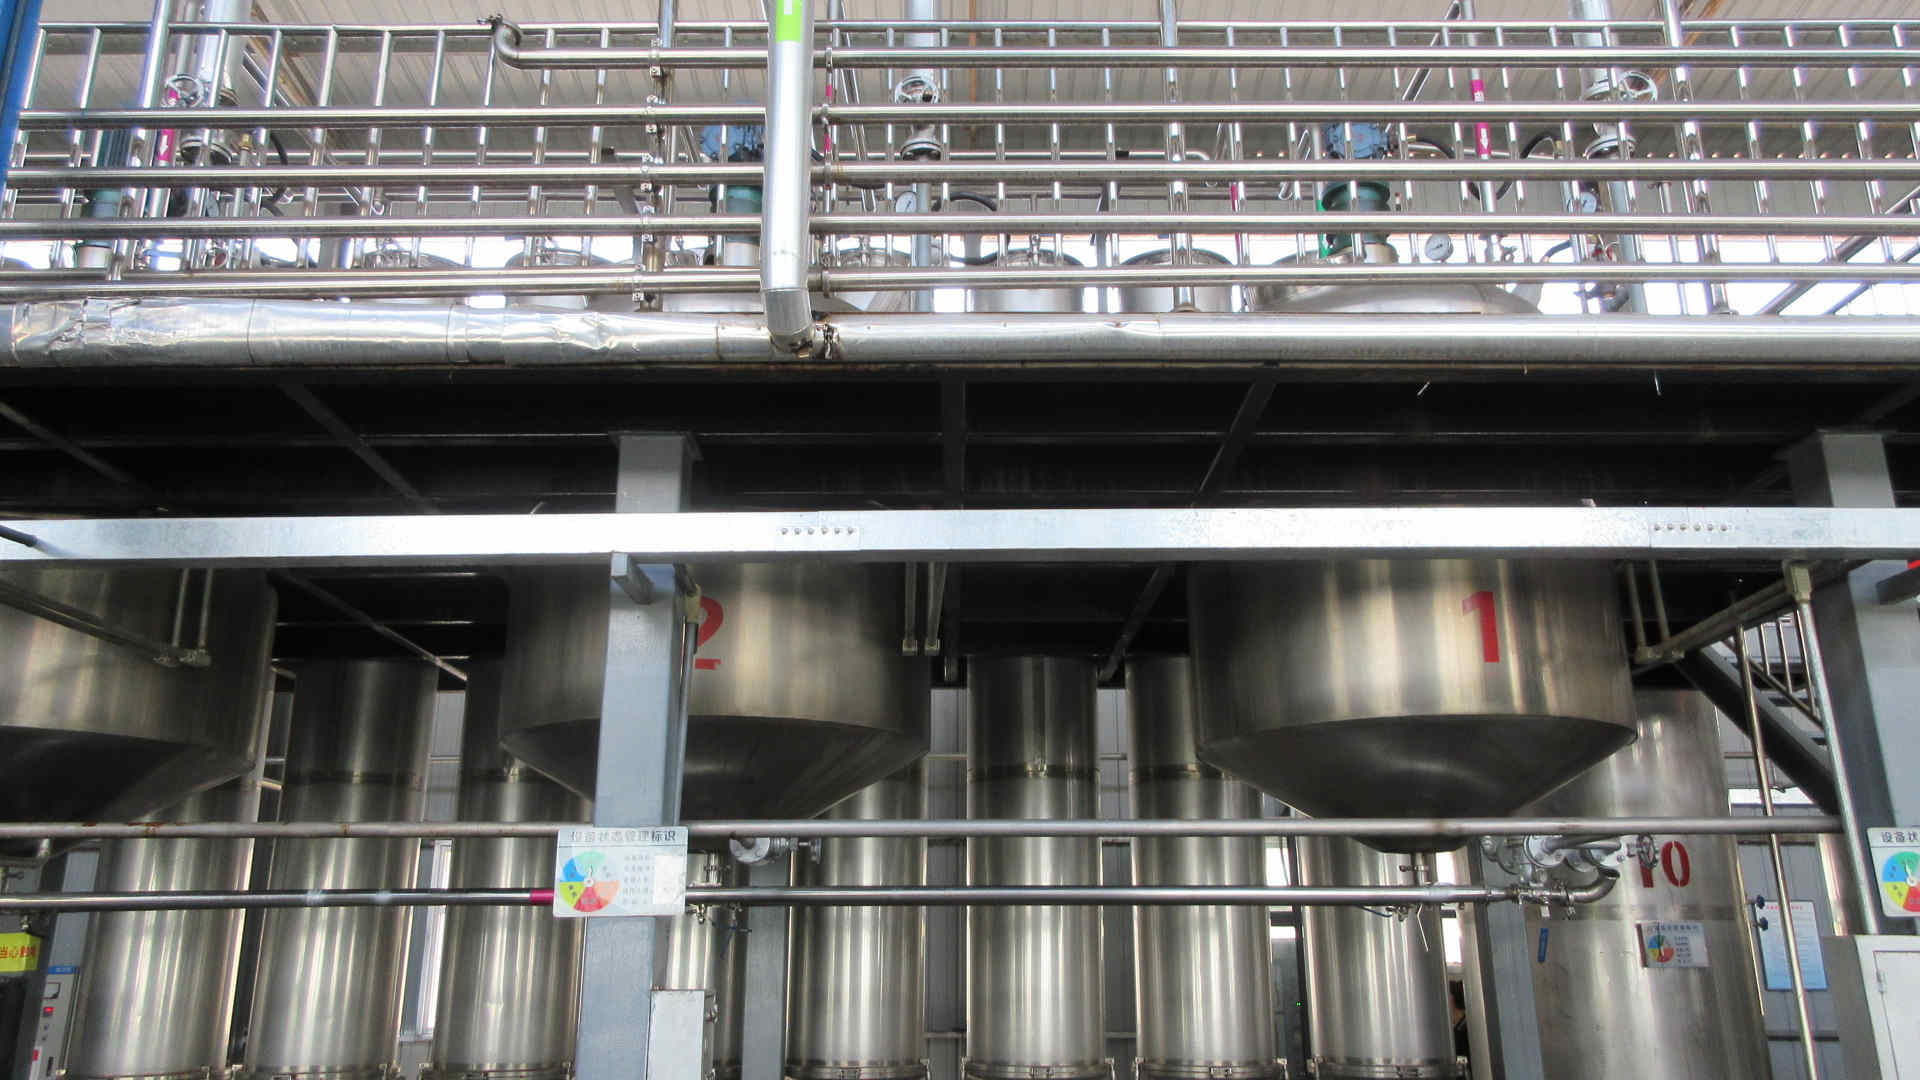
Jacketed Reaction Tank
Precise temperature and agitation controls for chemical refinement.
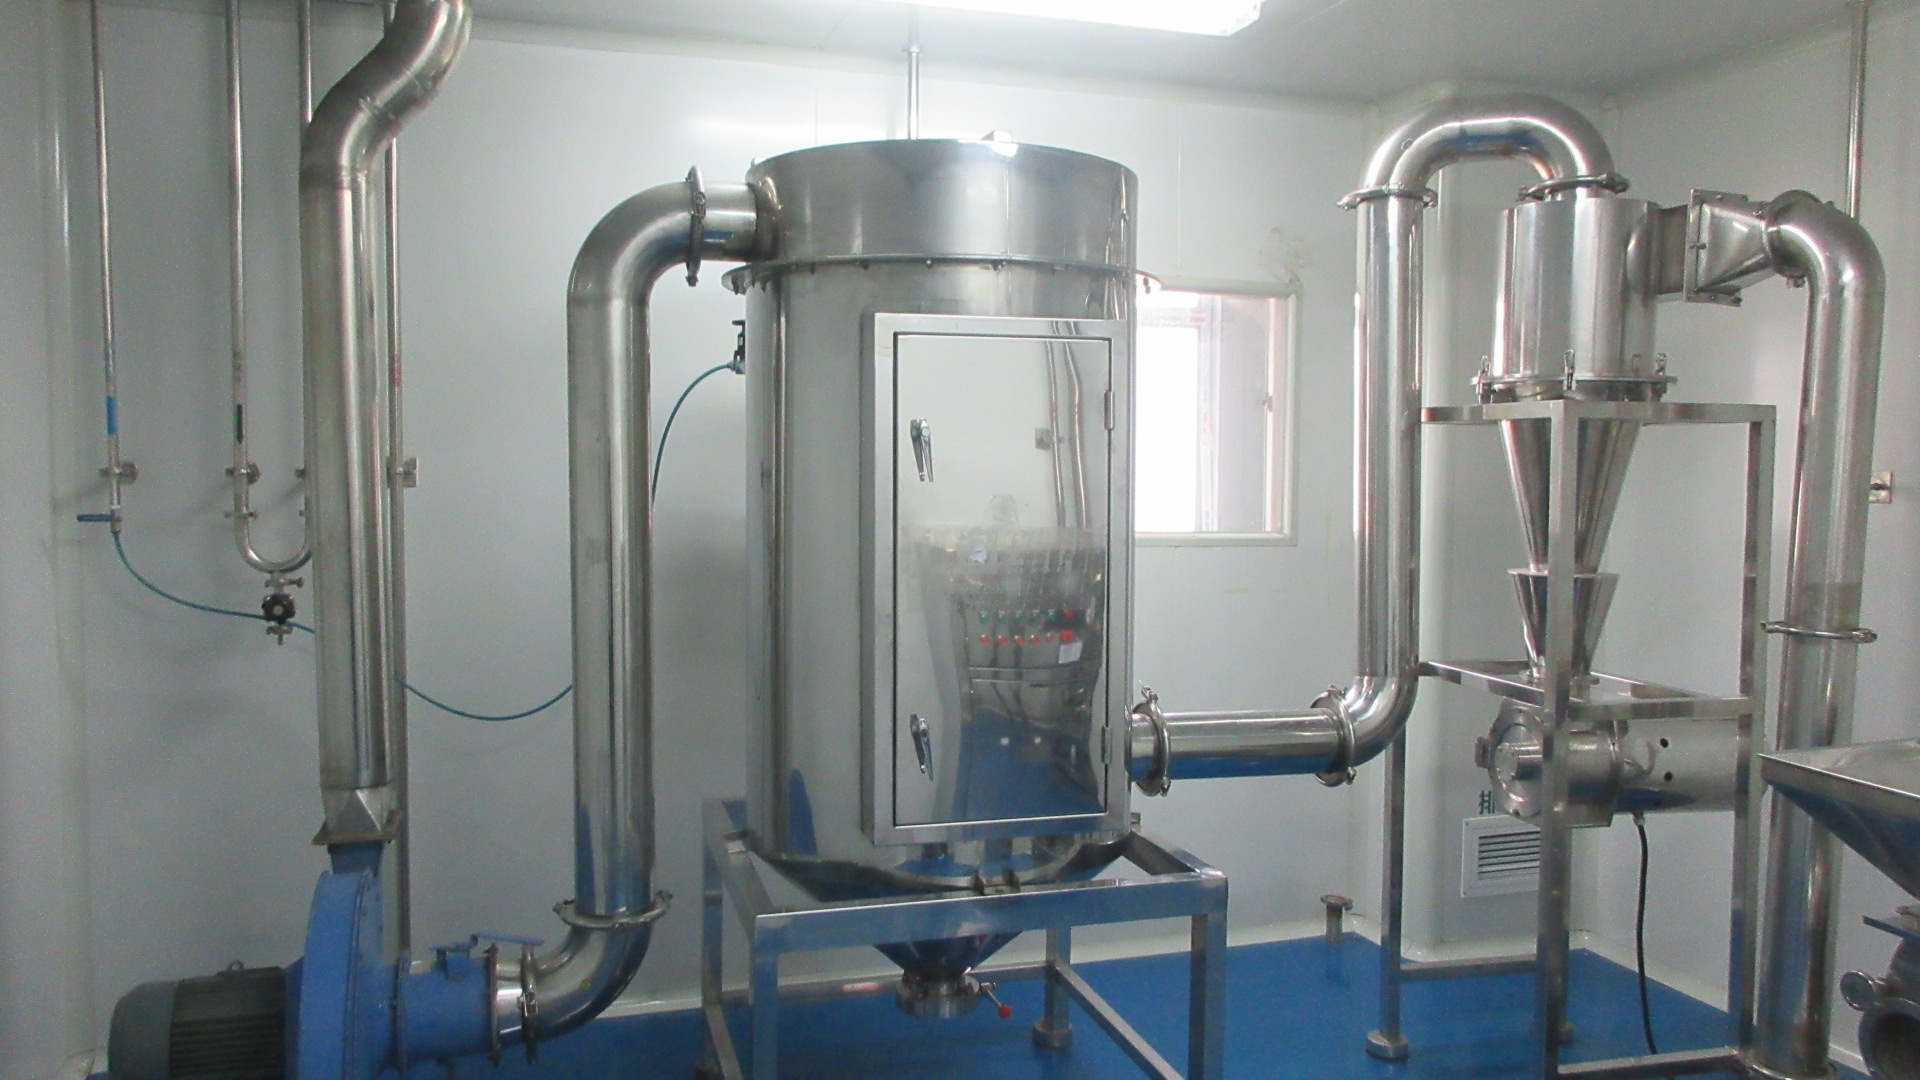
Ultrafine Pulverizer
High-speed impact milling for uniform, micronized powder density.
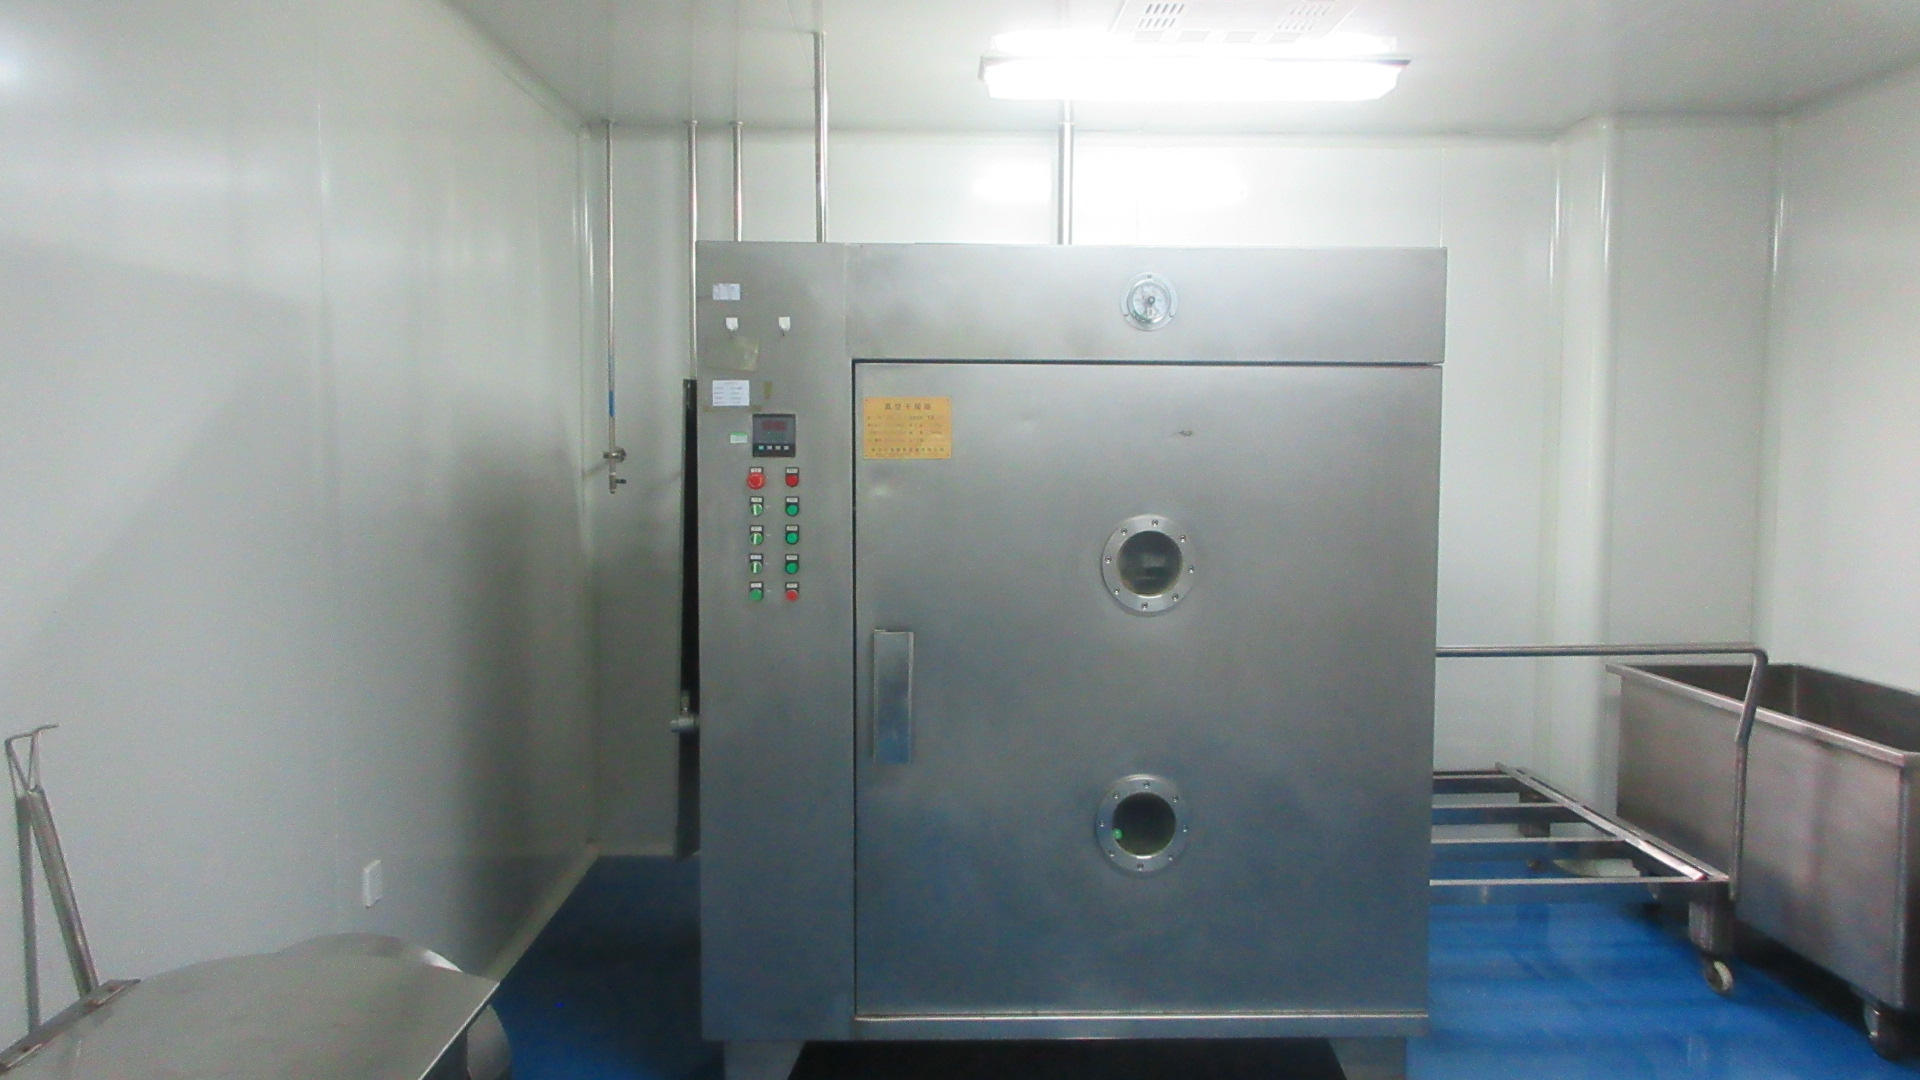
Vacuum Dry Oven
Cleanroom-compliant drying for moisture-sensitive active ingredients.
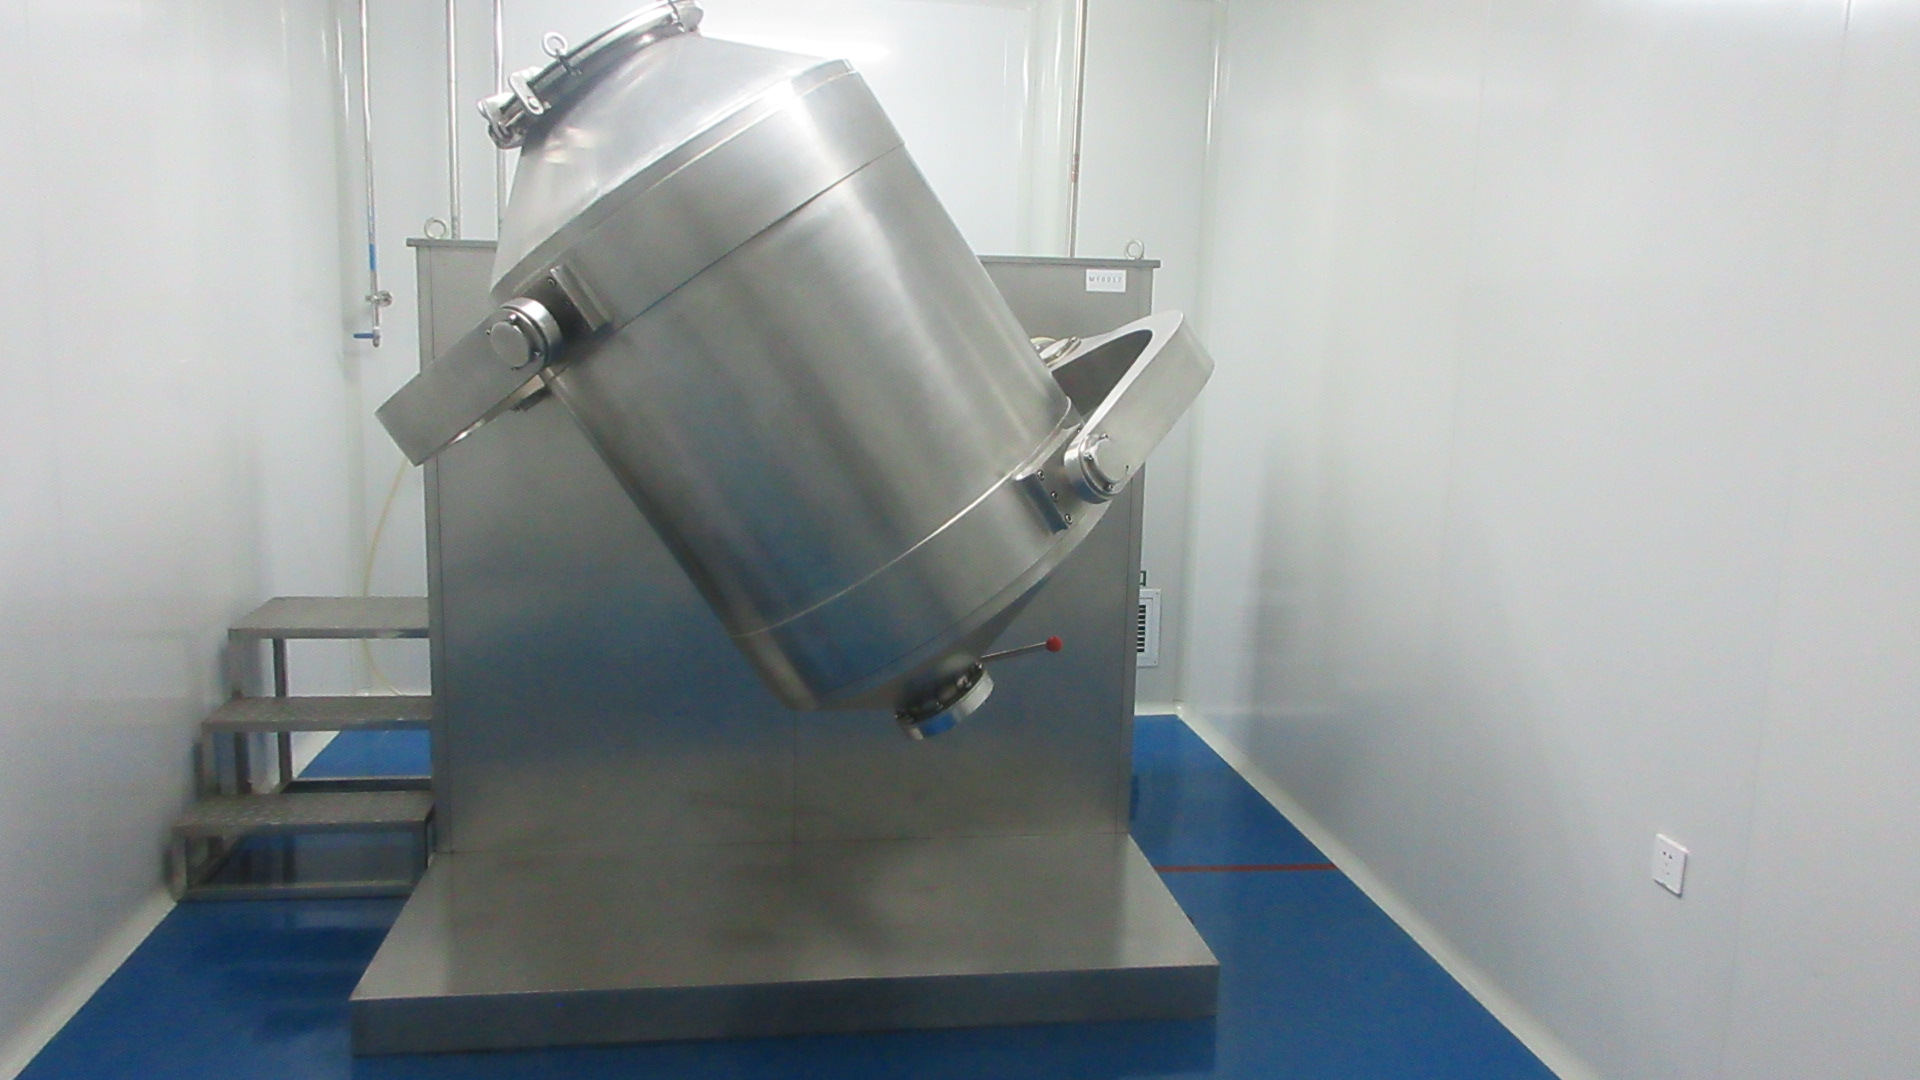
Homogenizing Mixer
Multi-directional powder blending for compound premixes and nutrition blends.
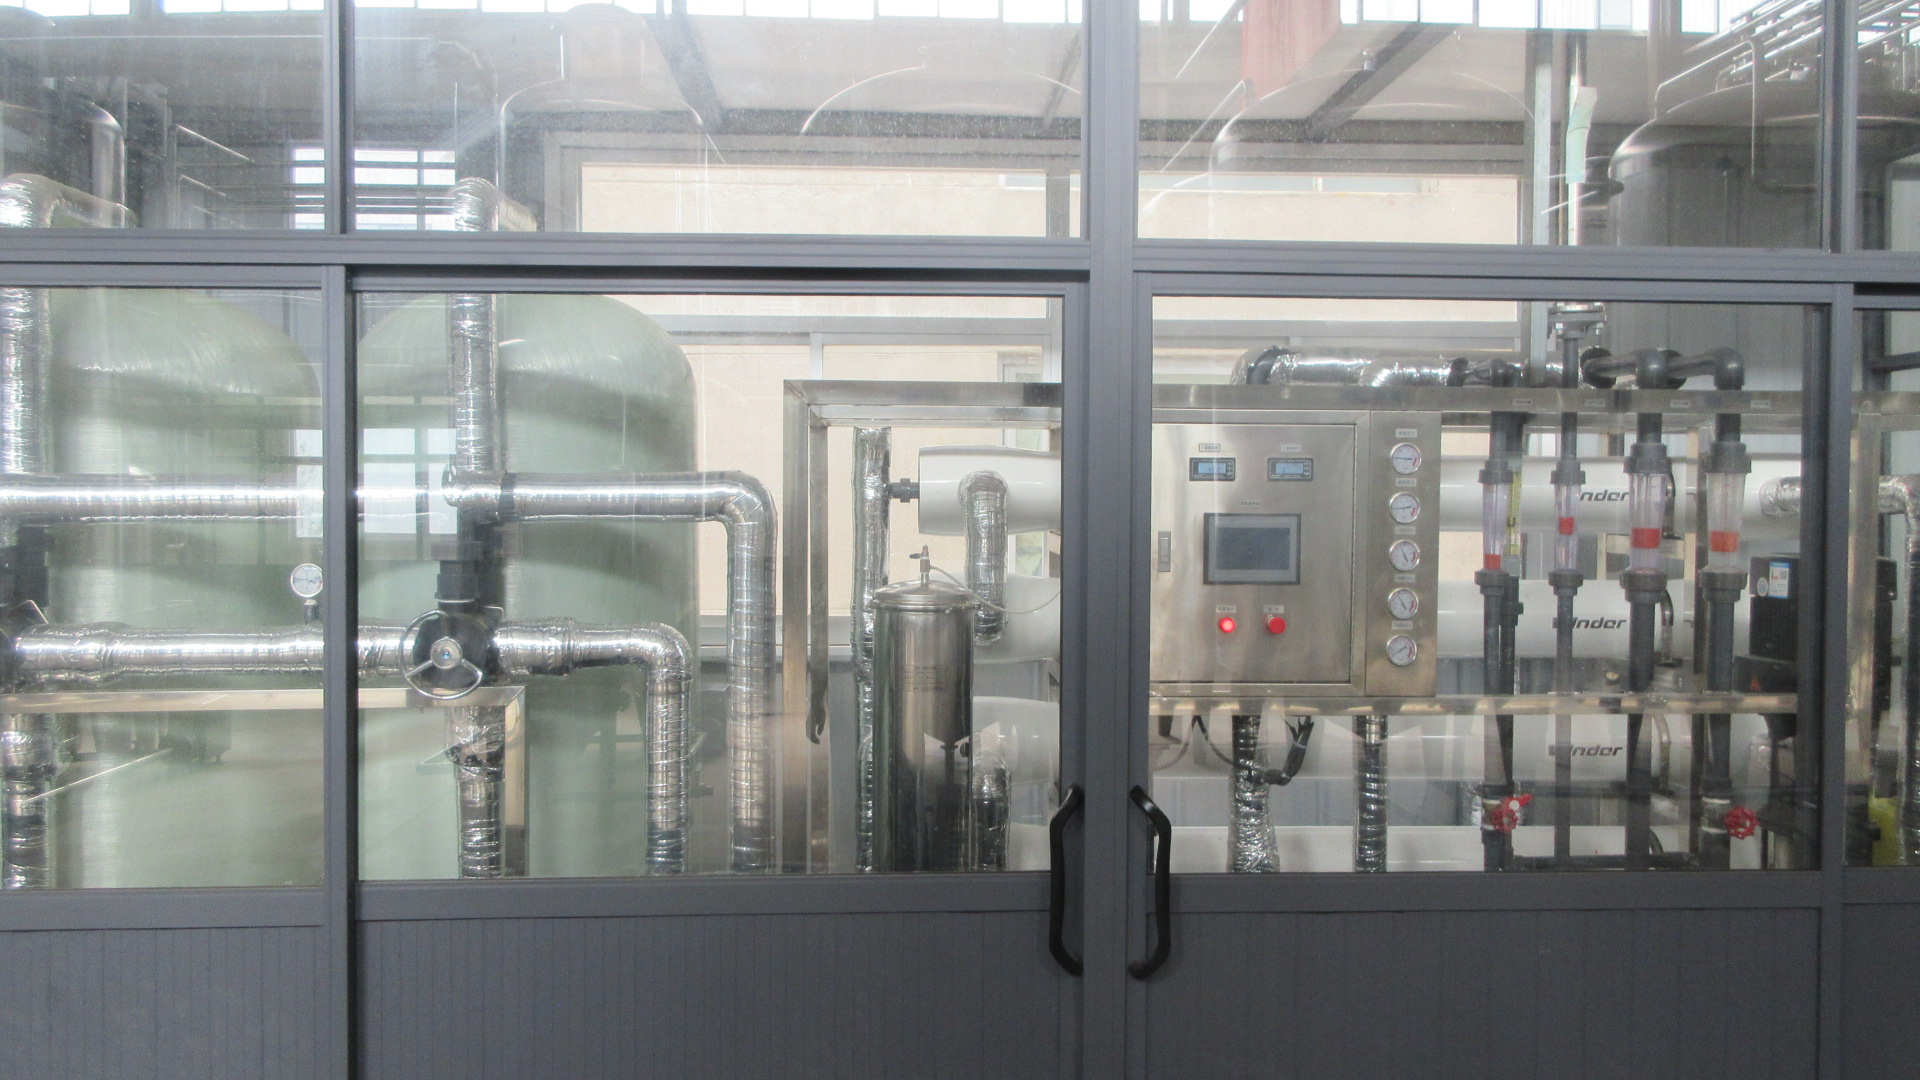
RO Water Treatment System
Multi-stage reverse osmosis unit delivering pharmaceutical-grade process water.
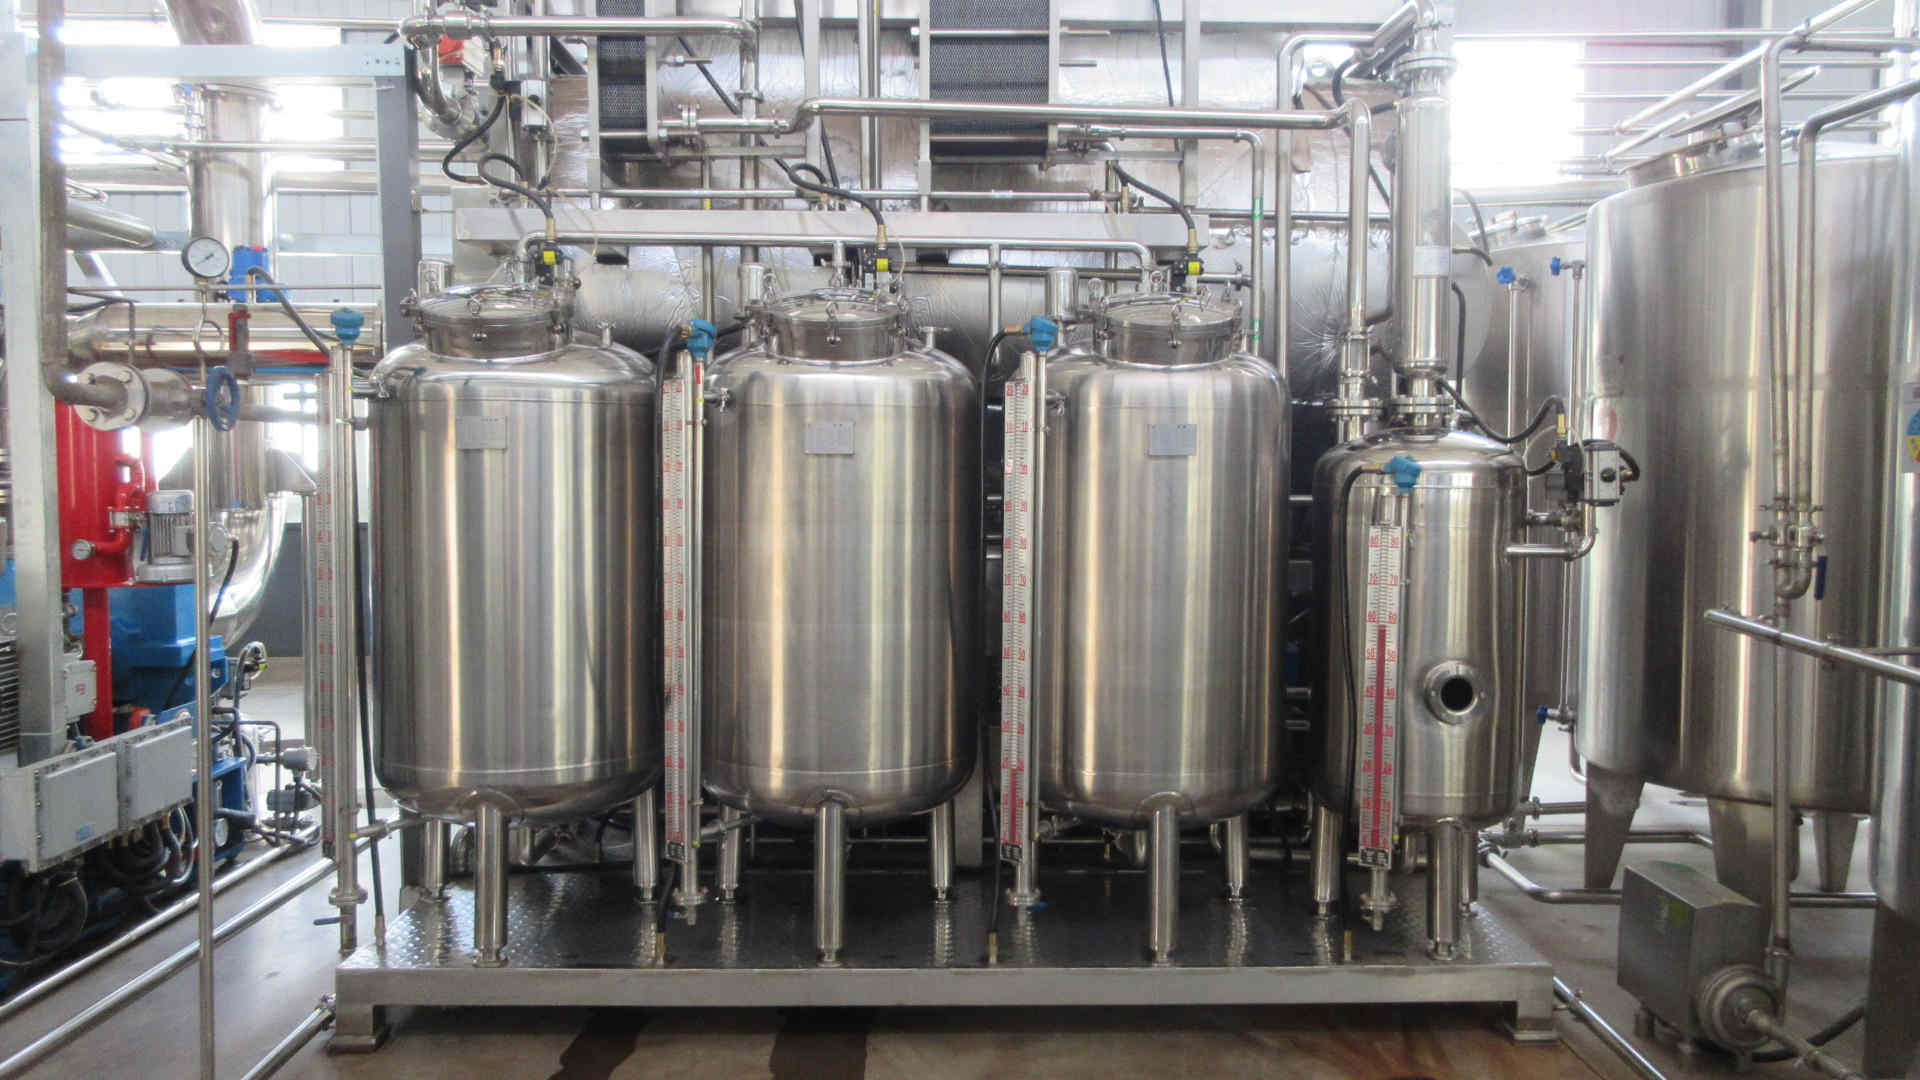
Electric Concentrator
Thermal evaporation equipment customized for small-batch active concentrations.
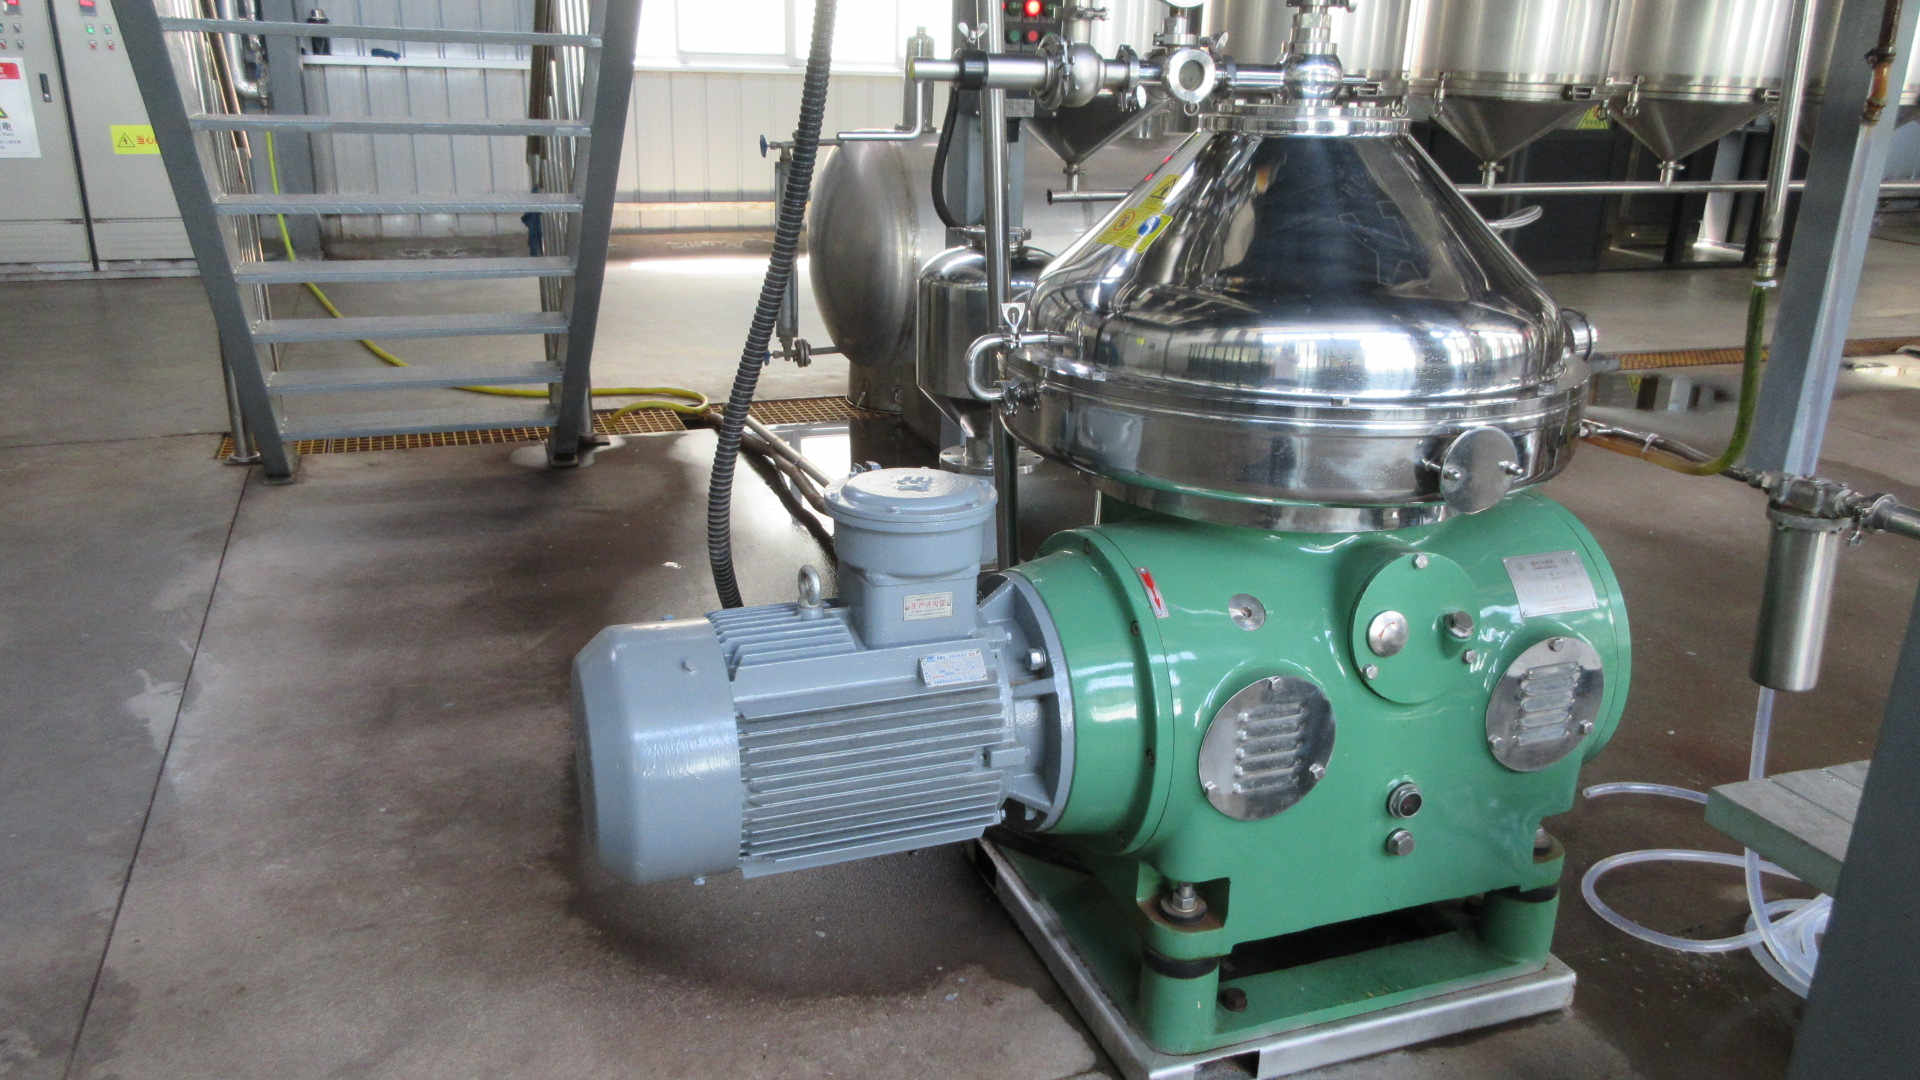
Disc Stack Separator
Continuous centrifugal clarification for liquid-solid separation with high yield.
Quality Control & Testing Instrumentation
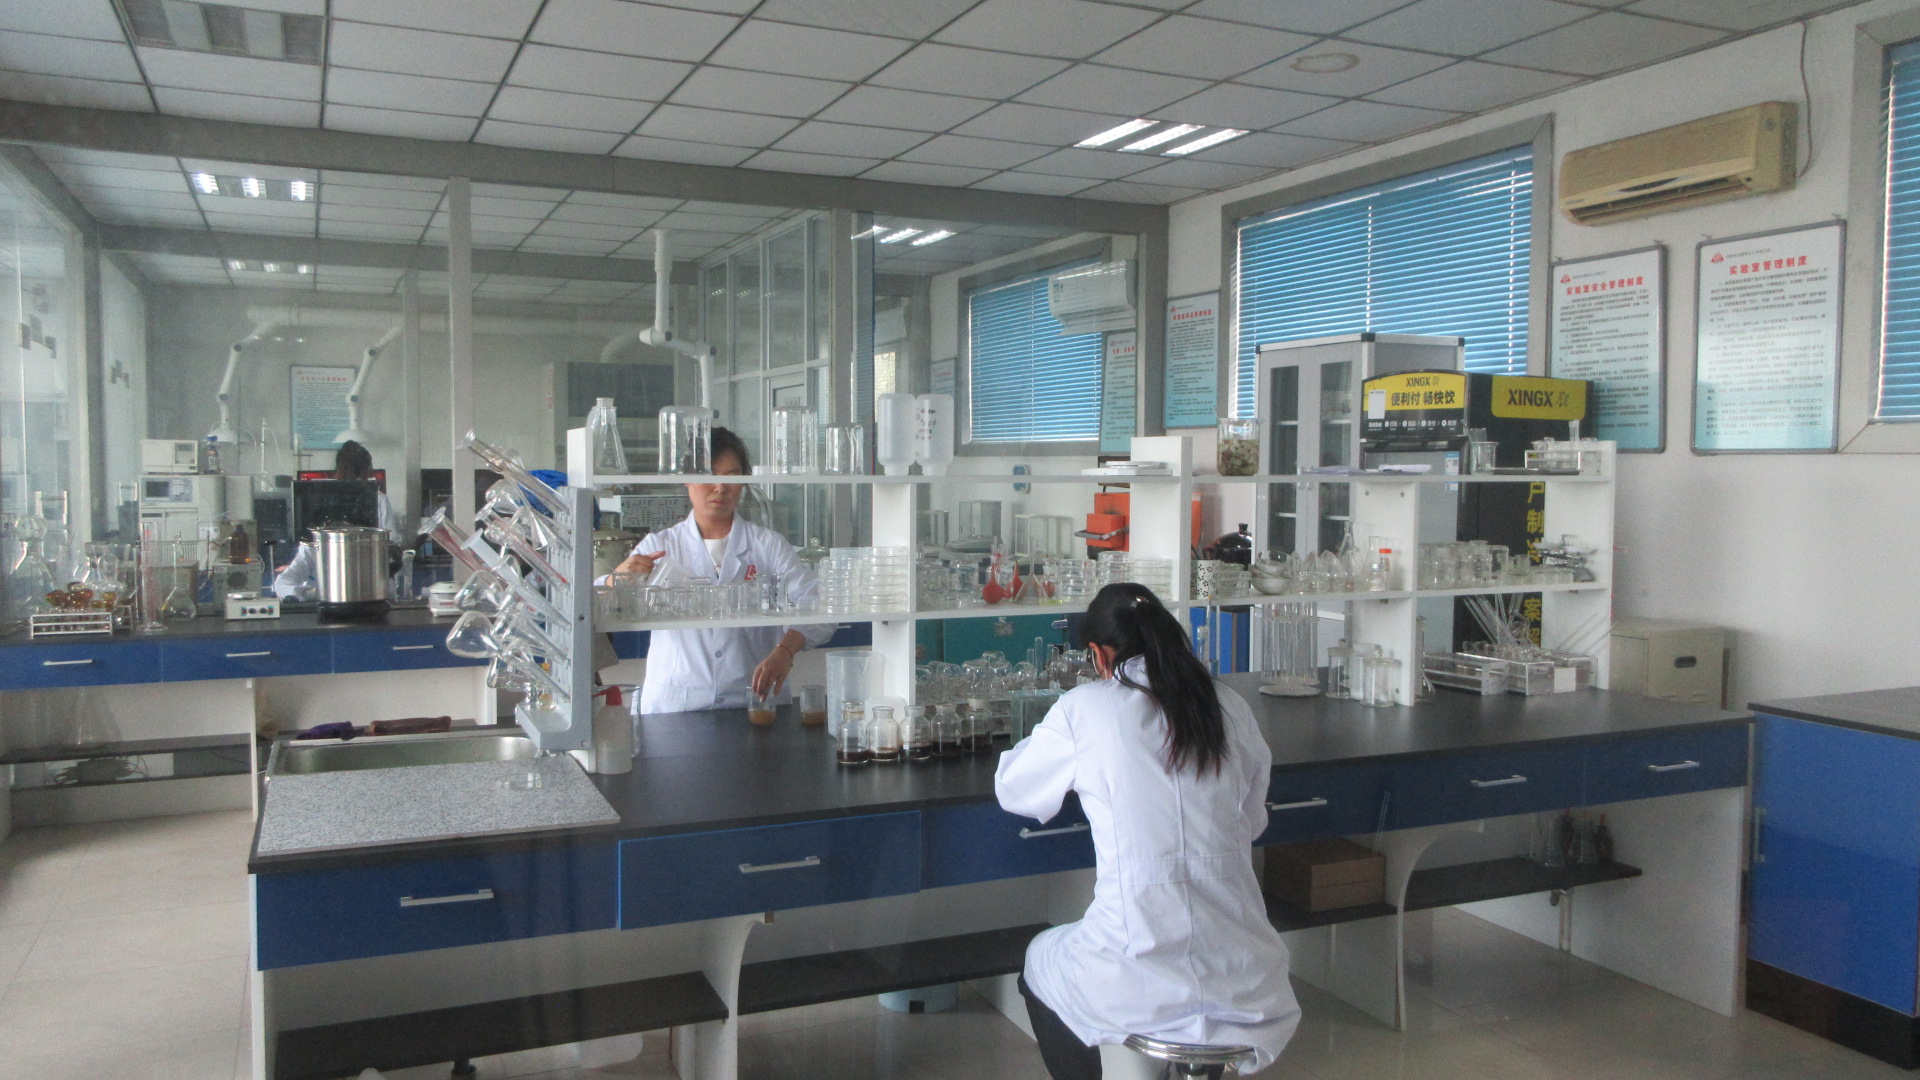
Central Testing Lab
Standardized inspection suite complying with GLP laboratory management.
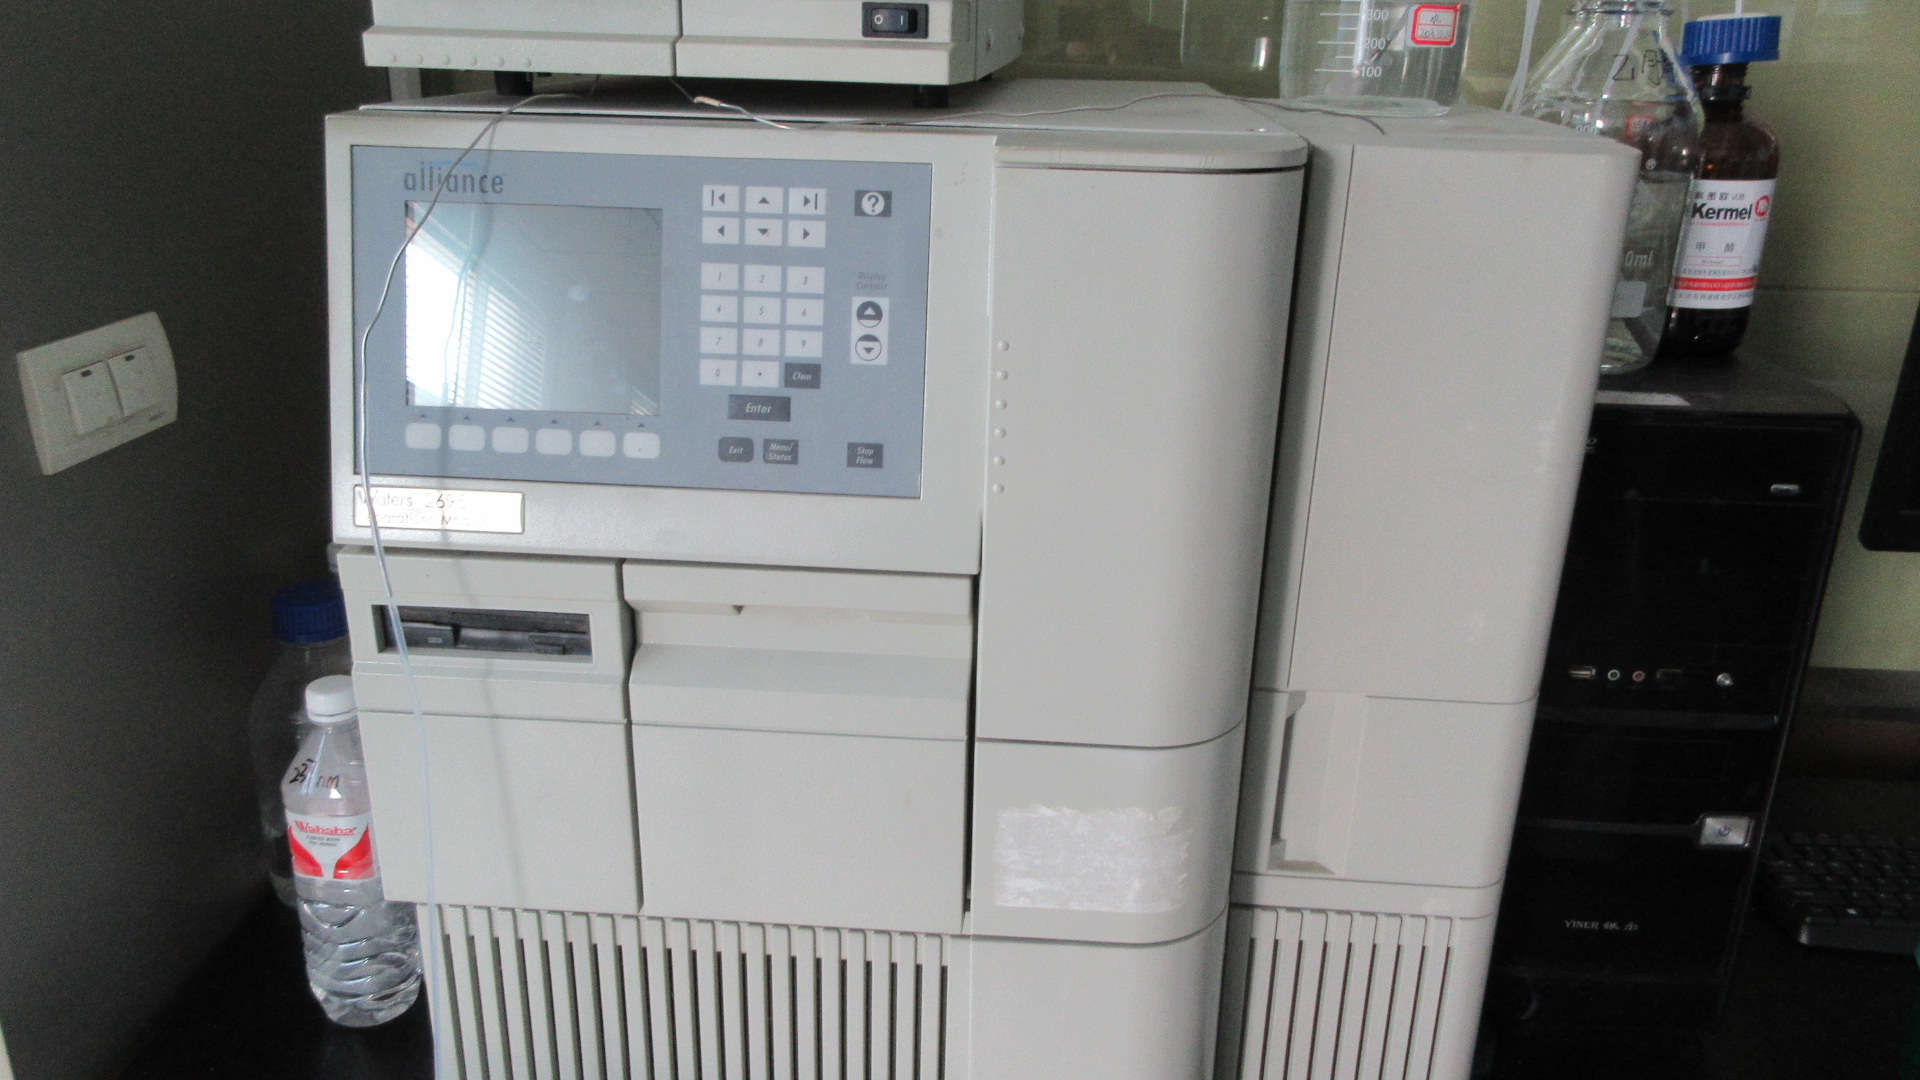
Liquid Chromatograph (HPLC)
Assay quantification, active monomer purity determination, and fingerprint analysis.
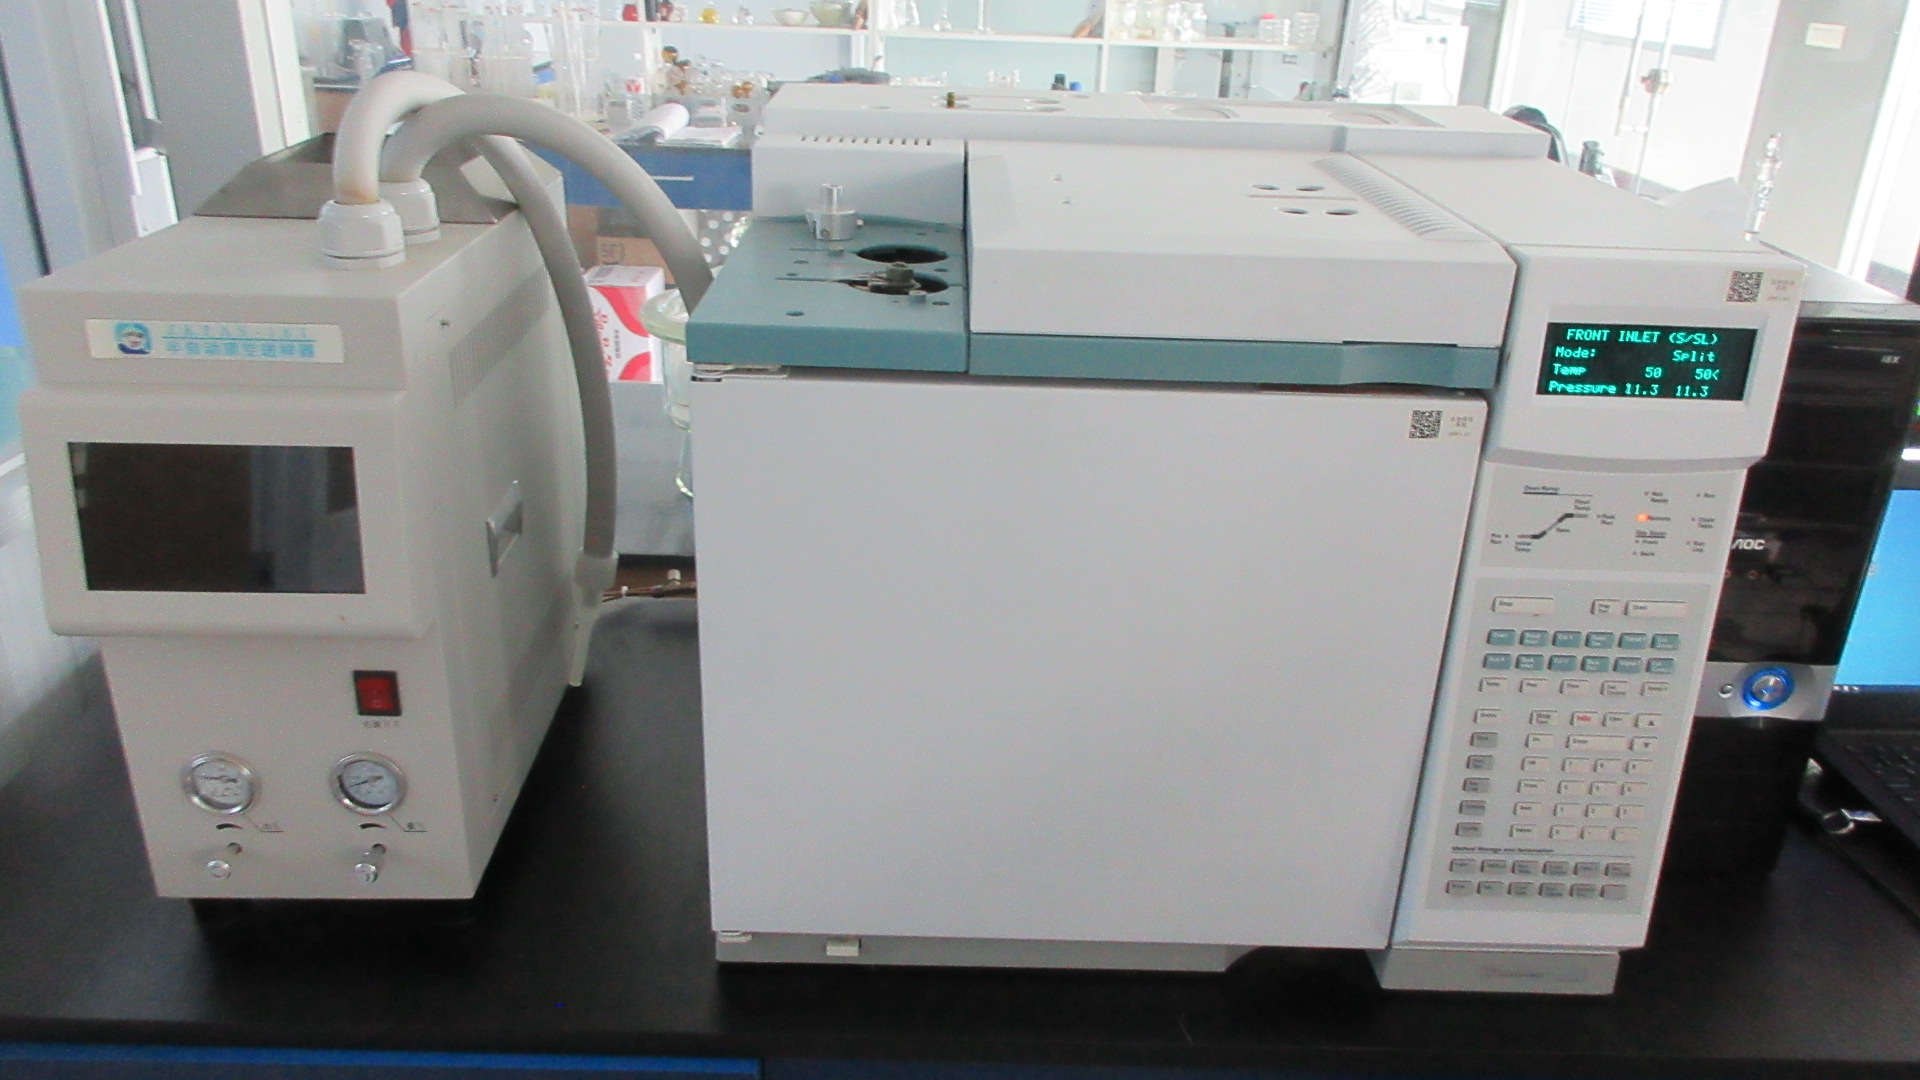
Gas Chromatography (GC)
Screening and quantification of residual extraction solvents and volatile compounds.
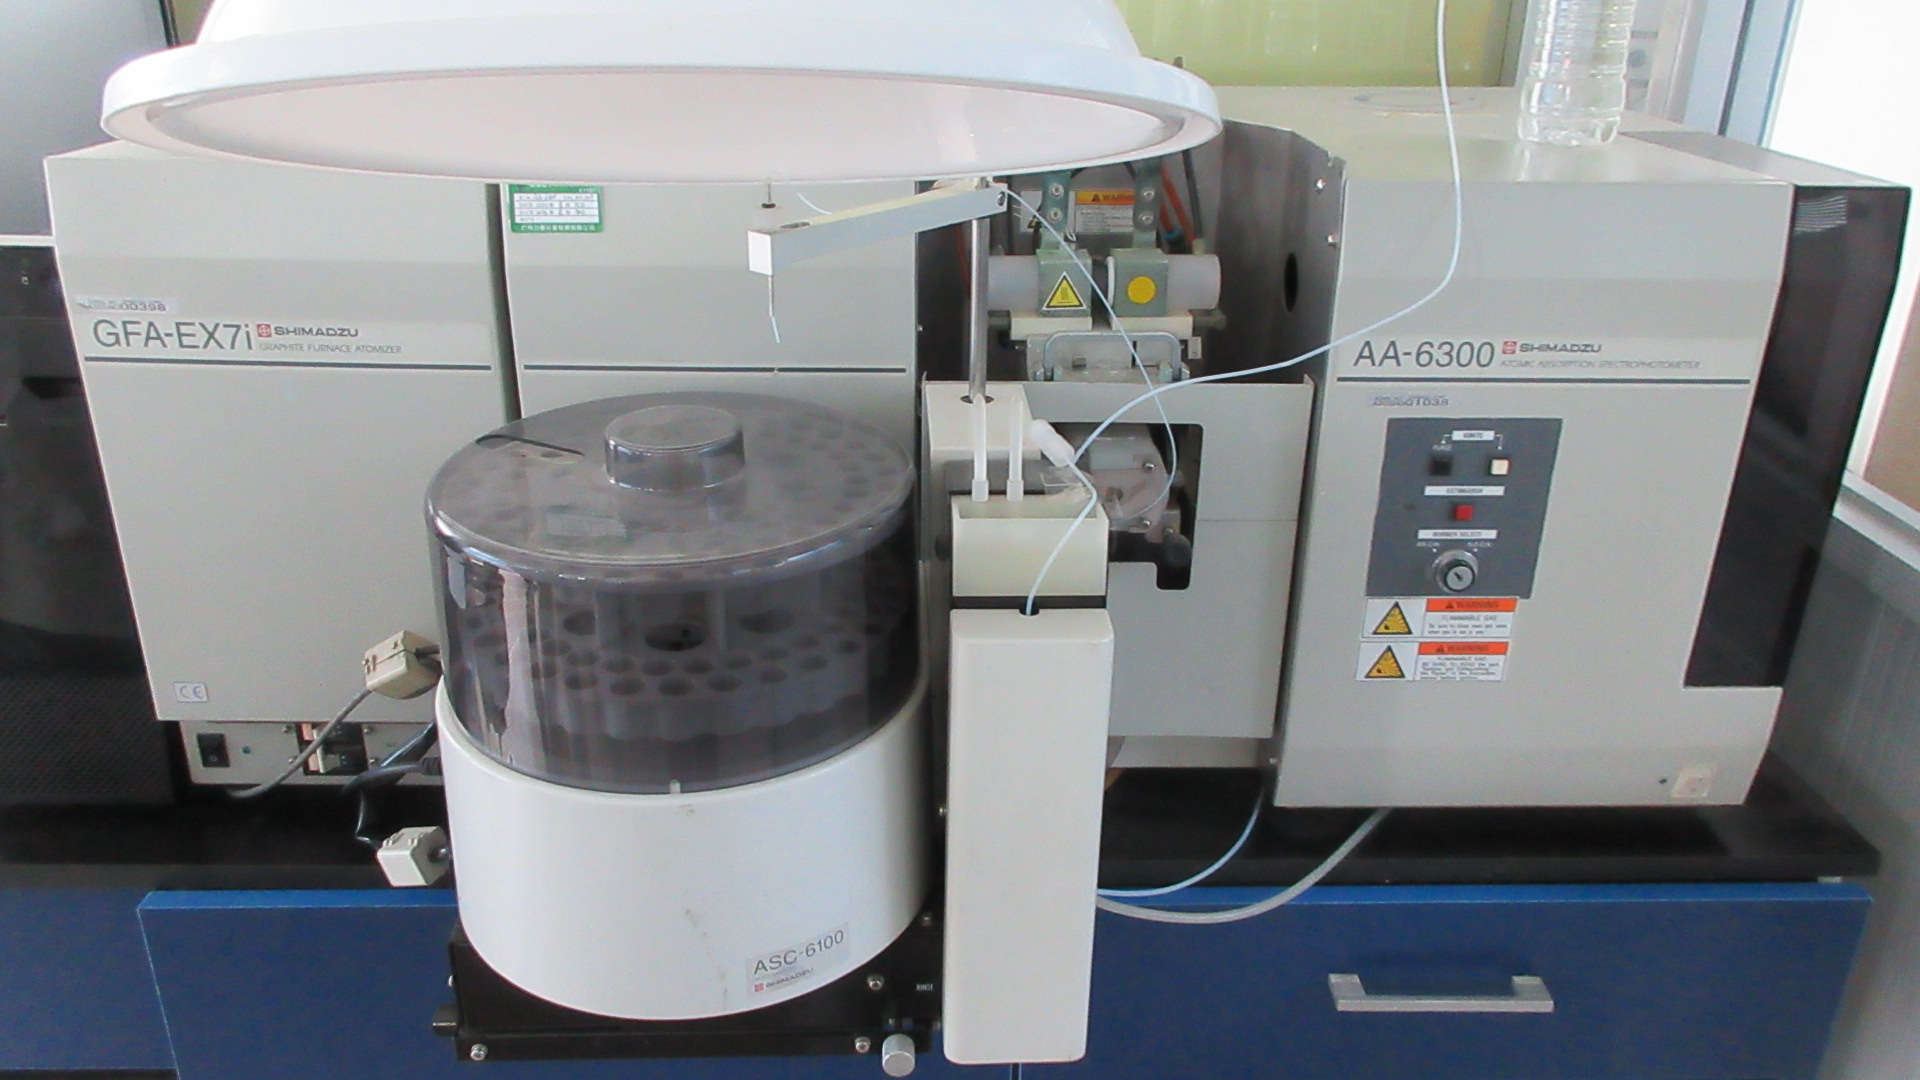
Atomic Absorption (AAS)
Trace heavy metal detection (Lead, Cadmium, Arsenic, Mercury) for USP/EP compliance.
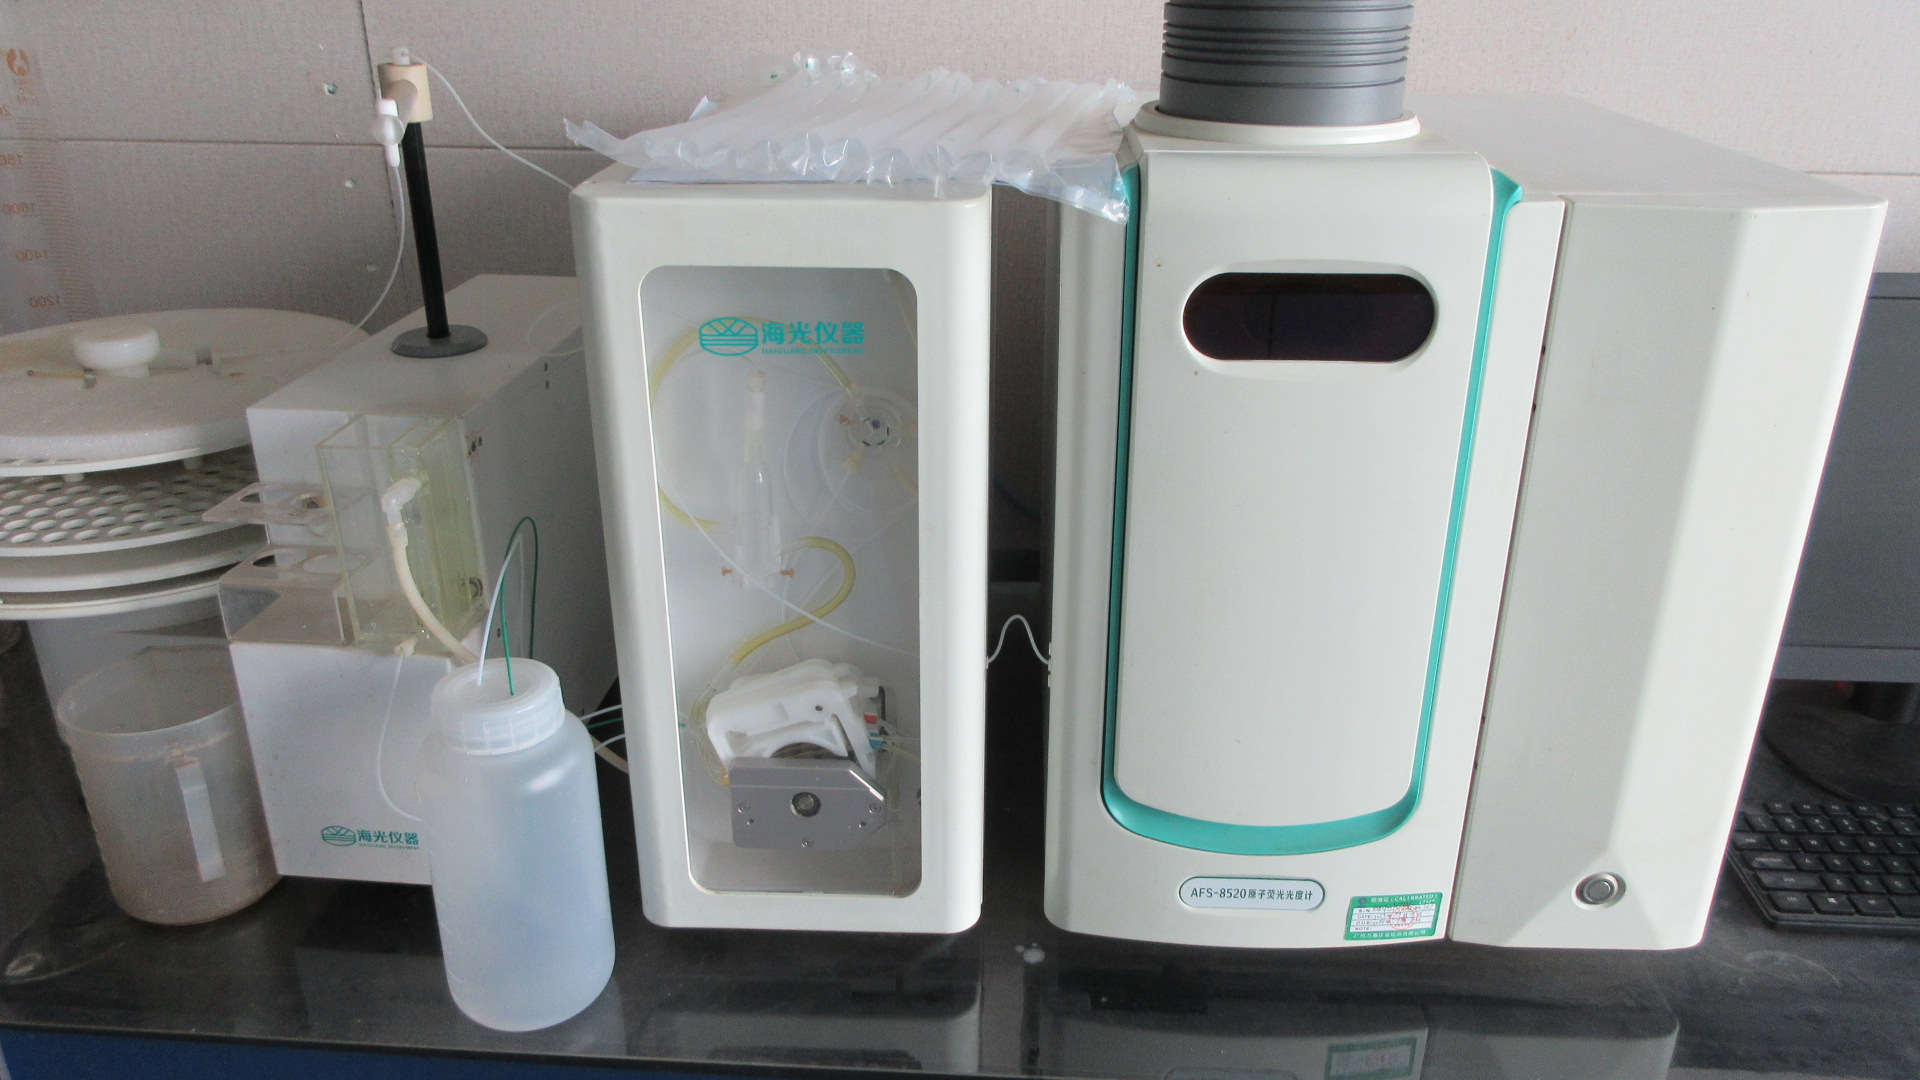
Atomic Fluorescence (AFS)
Ultra-trace level elemental determination ensuring uncompromising safety profiles.
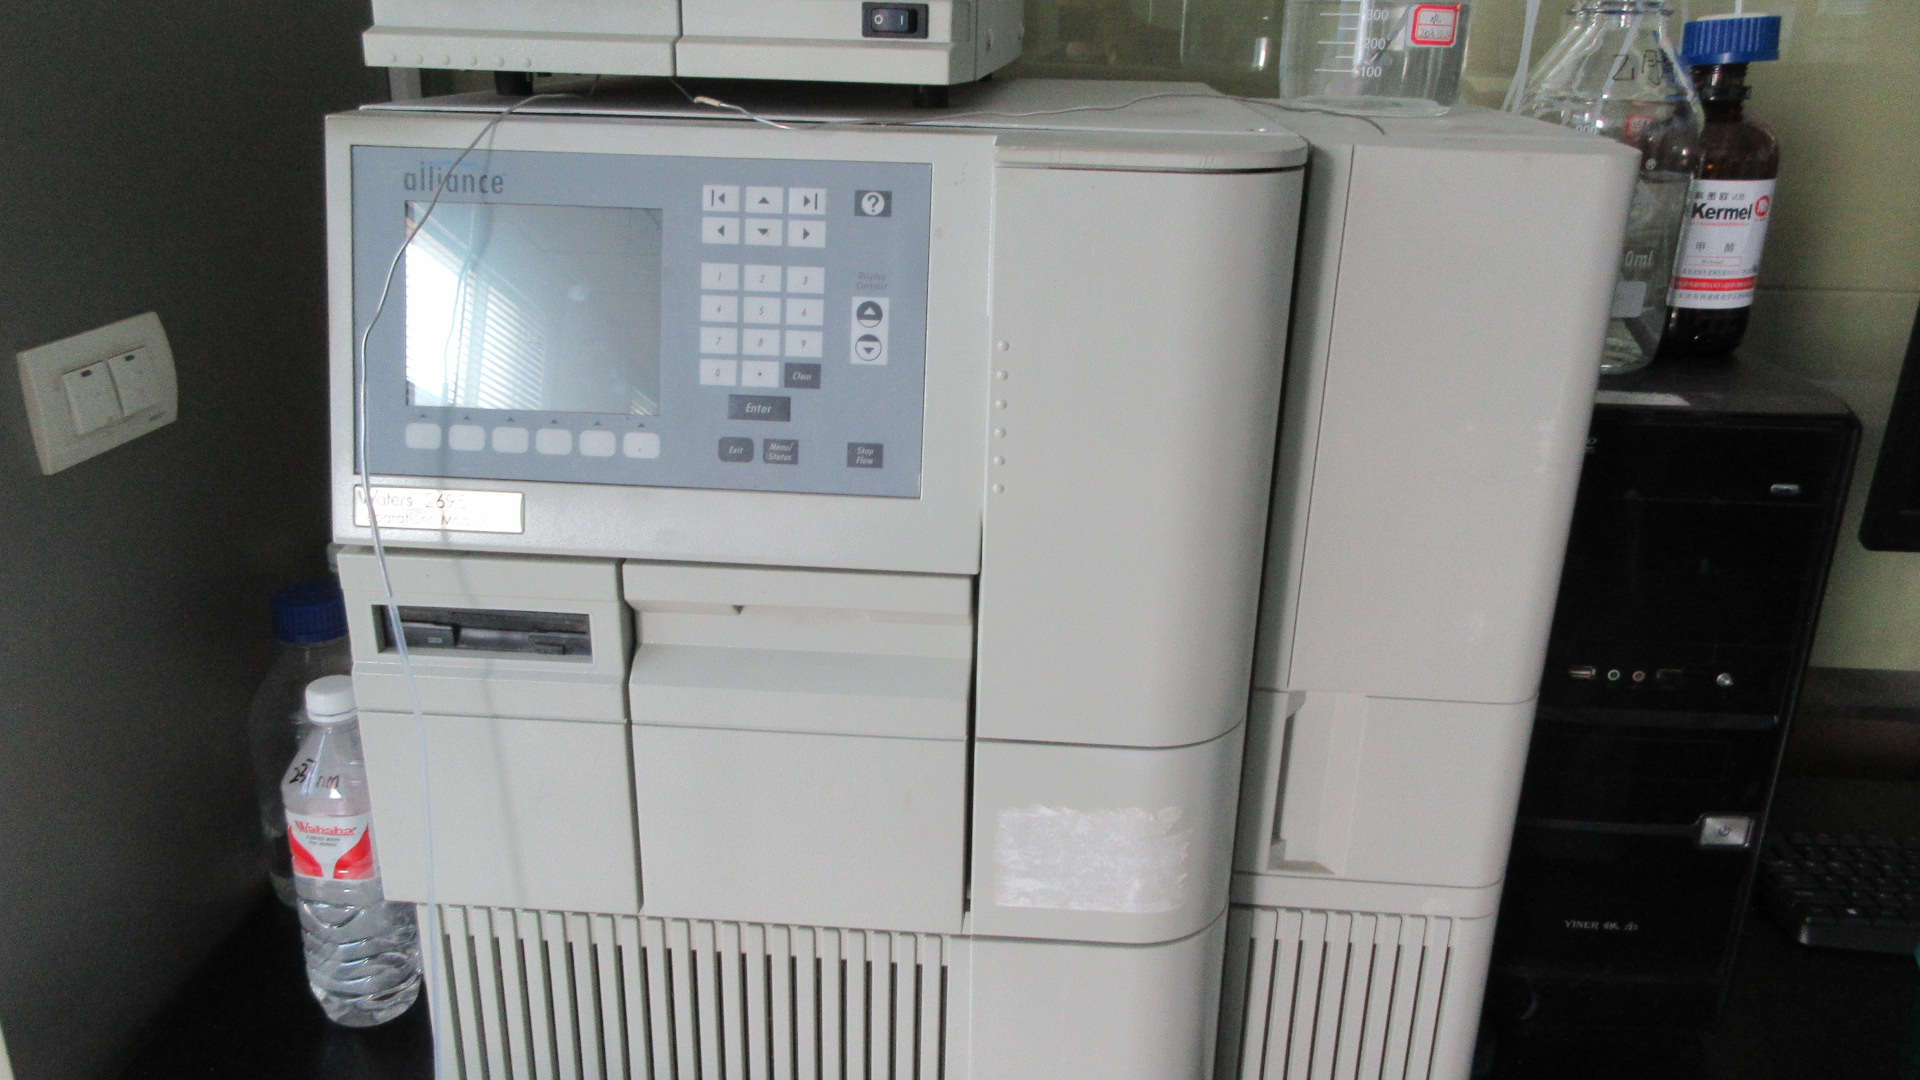
HPLC System Channel II
High-throughput testing channel for rapid lot verification and batch release.
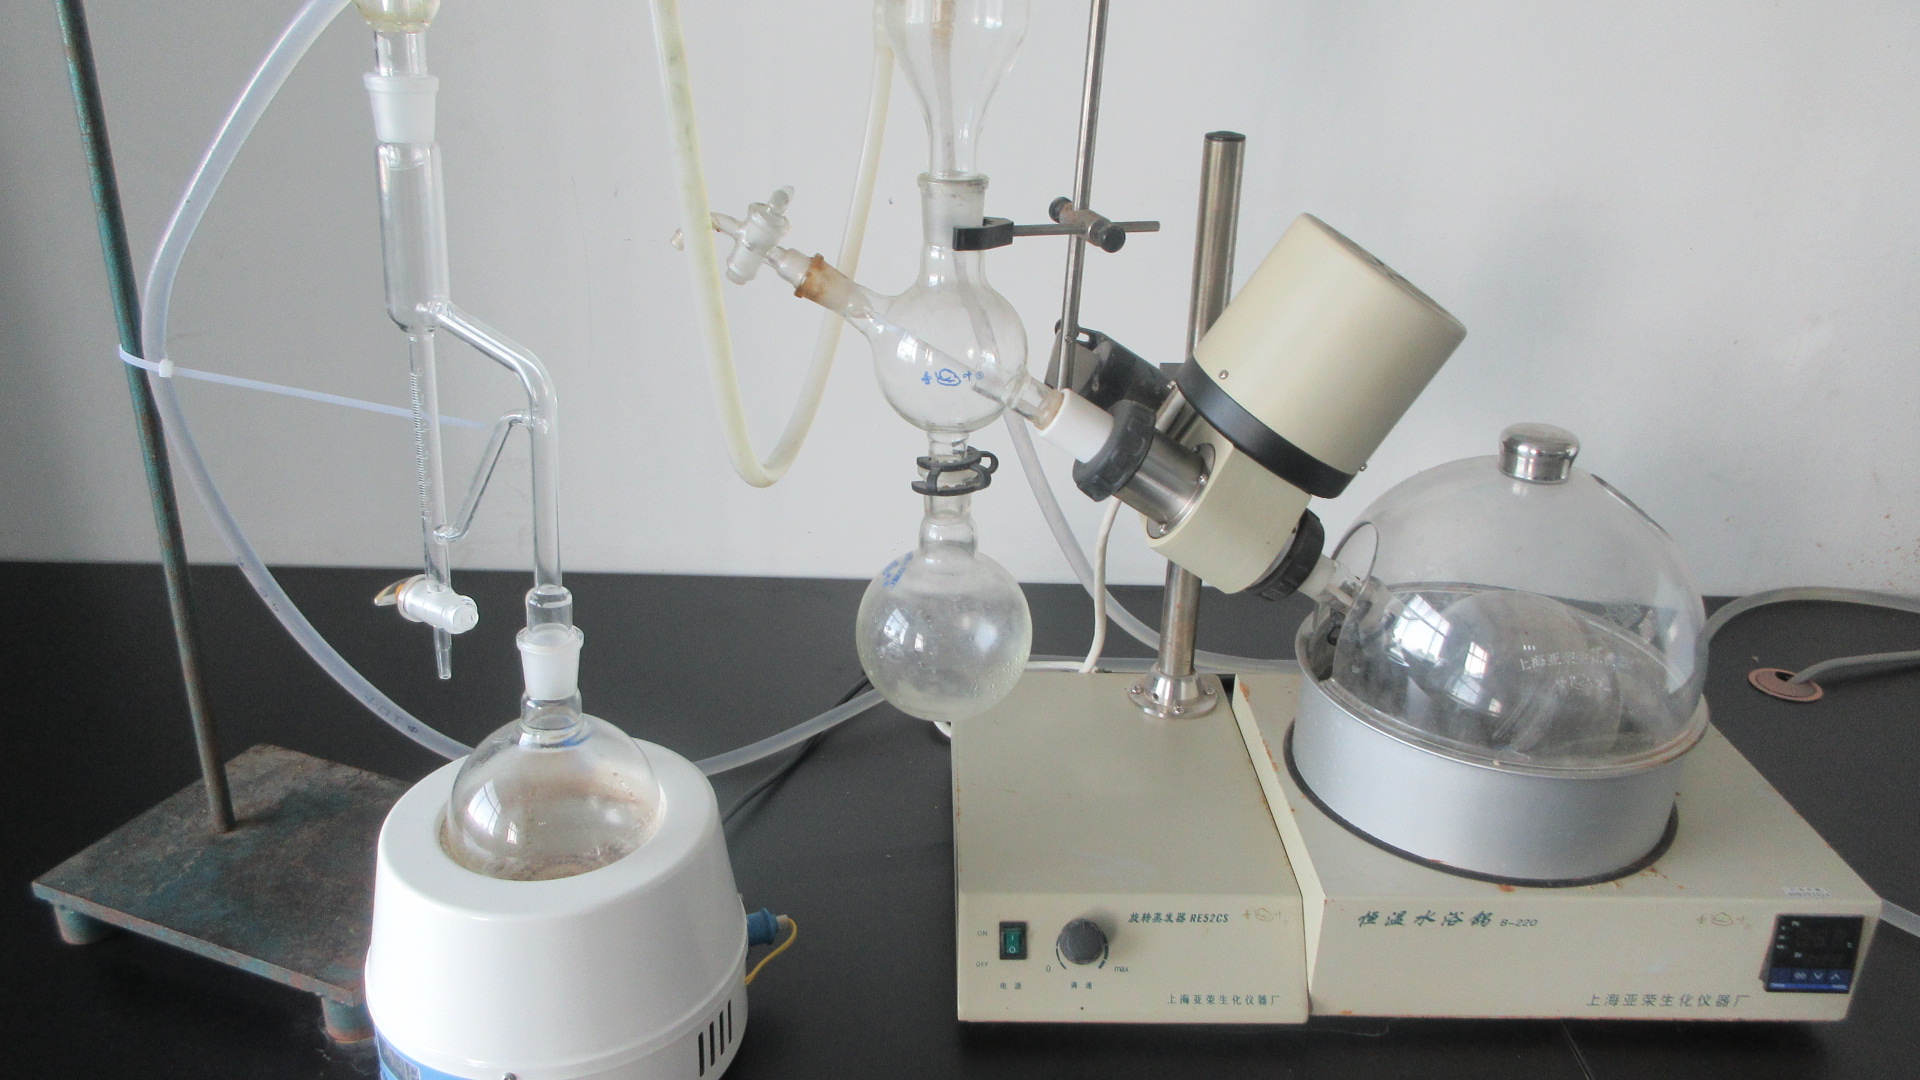
Rotary Evaporator
Solvent recovery and small-scale pilot trial concentration in R&D projects.
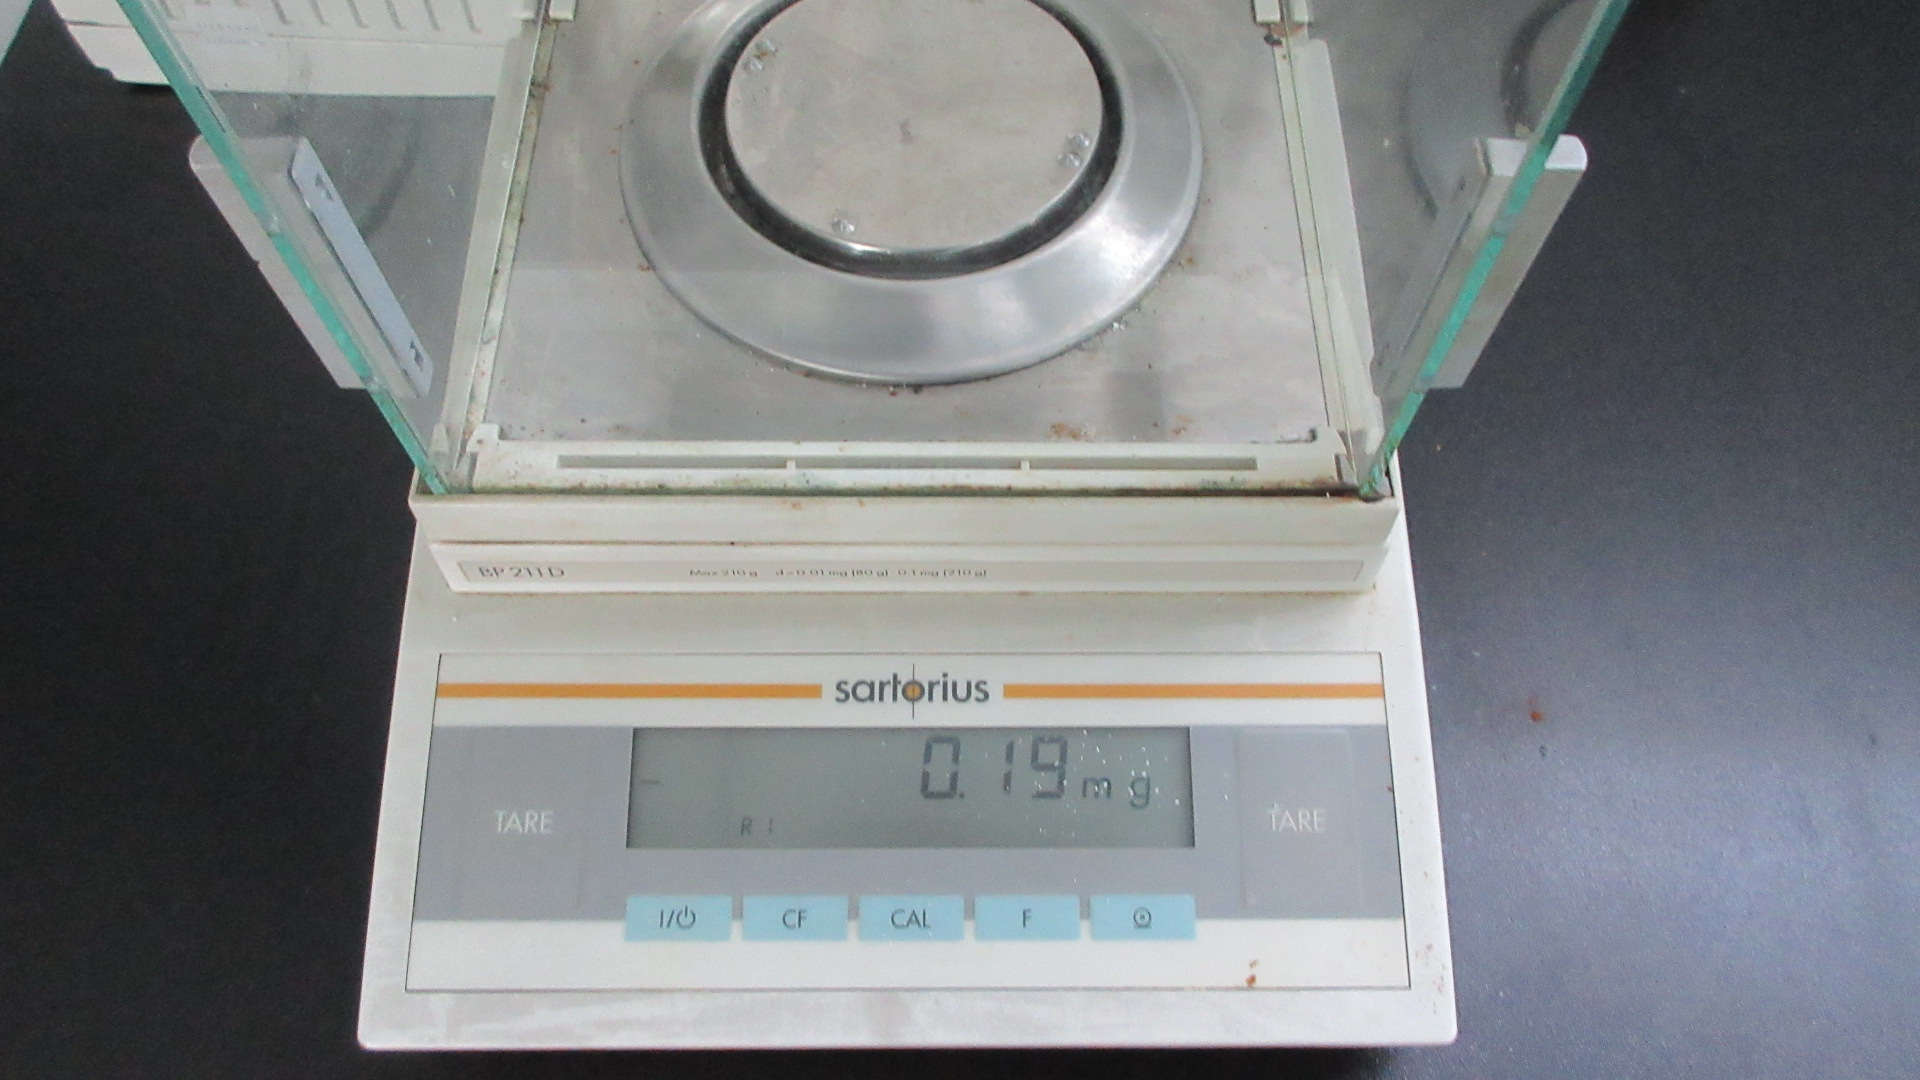
Micro Analytical Balance
0.0001g high-precision gravimetric measurements for accurate reference calibration.
Global Market Coverage & Export Infrastructure
Supplying pharmaceutical, nutraceutical, functional food, and cosmetic formulators across North America, Europe, Asia, and Latin America.
Strategic local inventory in the United States enables prompt 3-5 day delivery for core fast-moving items.
Routine fast transit via Shanghai, Beijing, and Qingdao ports with comprehensive customs clearance paperwork.
Regular on-site presence at global conventions including SupplySide West, CPHI World, and Vitafoods Europe.
Every shipment is backed by batch COA, MSDS, Certificate of Origin, and complete third-party lab documentation.
International Certifications & Factory Qualifications
Independent global assessments verifying regulatory adherence, social accountability, food safety standards, and strict religious dietary certifications.

ISO22000
Certified by SGS (CN25/00007367)
Audited
cGMP
Certified by SGS (CN23/00001732)
Audited
FSSC22000
Certified by SGS (CN23/00006360)
Audited
USDA Organic
Cert ID: 1780878535
Certified
HALAL
Cert ID: 25449371654285
Certified
KOSHER
Cert ID: MM8NL-V9SJ3
CertifiedRequest Audited Factory Dossiers & Working Quotes
Contact our technical procurement team directly for specification sheets, third-party SGS inspection reports, batch COAs, and customized sample packages.